Tensile Creep Testing Parameters for Short Fiber Thermoplastics
Tensile creep parameters for short fiber thermoplastics require testing excised part coupons along and across melt flows under controlled moisture and temperature.
Tensile creep parameters for short fiber thermoplastics require testing excised part coupons along and across melt flows under controlled moisture and temperature.
Dynamic deflection and pressure loss decay require rigid pre-loaded bolsters, tapered core interlocks, and rheologically balanced hot runner delivery.

Size gate depth to wall thickness and expand width to keep shear rates below polymer degradation limits under non-Newtonian melt flow.
Predictive transient thermal modeling optimizes conformal core channels, balancing heat extraction and structural integrity to minimize cycle time and part warpage.
Scientific moulding balances multi-stage cavity pressure against gate freeze timing to eliminate differential shrinkage across non-uniform wall sections.
Balancing standing steel thickness below sixty percent of nominal wall and maintaining turbulent cooling prevents cosmetic sink marks.
Melt flow length scales with cavity thickness raised to the third power while cycle time increases quadratically, forcing tight nominal wall control.
Non-linear degradation modeling protects coated carbide shutoff lands by predicting exponential wear acceleration from volatile chemical binder leaching.
Injection mold land recession requires SPC tracking of shut-off steps to schedule laser micro-welding before parting line wear causes flash.
Balance high-cavitation valve-gated manifolds by calculating viscous shear heating against conductive steel losses to equalize cavity fill across cycles.
Optimizing melt channel bifurcations with melt rotation geometry and stepped hydraulic diameters eliminates shear-induced viscosity gradients across cavities.
Naturally balanced manifolds require symmetrical 3D runner geometry, smooth transitions, and uniform thermal zones to ensure identical cavity filling.
Perfection of cross-border offsite tooling requires local statutory registry filings, bilingual plates, bailment contracts, and customs documentation.
Predicting warpage in semicrystalline inserts requires coupling transient thermal FEA with crystallization kinetics to balance core-cavity heat flux.
Turbulent flow inside conformal cooling circuits requires managing additive channel roughness and diameter to prevent pump choking and inflated cycle times.
Transient cooling calculations govern injection mold cycle times, where resin thermal diffusivity and steel channel turbulence dictate part yield and warpage.
Dynamic process window drift in high cavitation tooling is verified through cavity-stratified telemetry and contractual pressure integral bounds.
Calculate mold cavity dimensions using ISO 294-4 divisor formulas biased toward steel-safe limits to absorb material shrinkage variance before machining.
Tolerance grade allocations require matching polymer shrink variance and parting line mechanics to DIN 16742 standard capability limits early.
Optimal stretch blow moulding demands exact pre-blow timing synchronization to control strain hardening and achieve uniform container wall thickness.
Coupled viscoplastic modeling of back-stress hardening and adiabatic softening allows thin-wall tooling optimization that cuts cycle times and capital spend.
Deterministic FPGA processing of piezoelectric cavity telemetry converts micro-moulding melt front arrivals into sub-millisecond switchover execution.
Predictive state observers compensate fieldbus latency in thin-wall tooling, shifting pressure switchover before delayed packets cause cavity flash.
Closed-loop cavity pressure control stabilizes micro-injection molding by compensating for viscosity shifts and holding part dimensions within micron tolerances.
Deterministic TDMA wireless telemetry across multi-cavity tooling eliminates fragile wiring harnesses while preserving sub-millisecond pressure curve tracking.
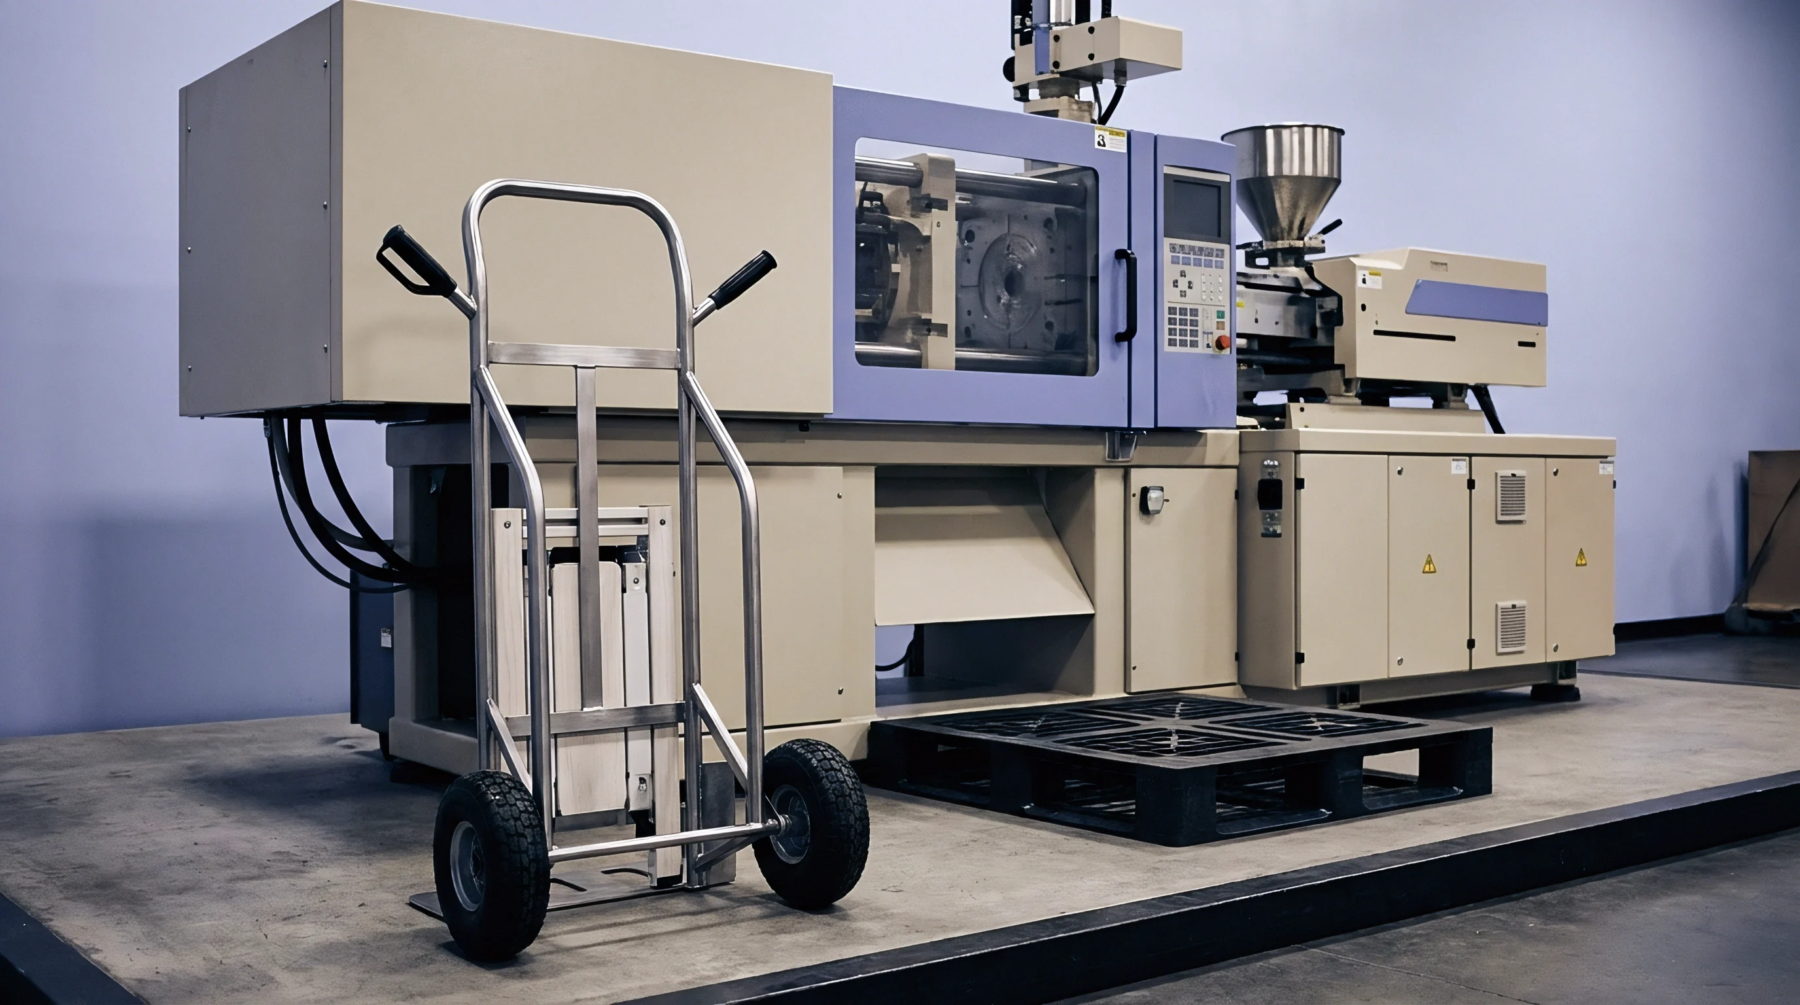
Coupling cavity pressure telemetry directly to machine velocity switchover eliminates part weight variance caused by melt viscosity shifts across production runs.
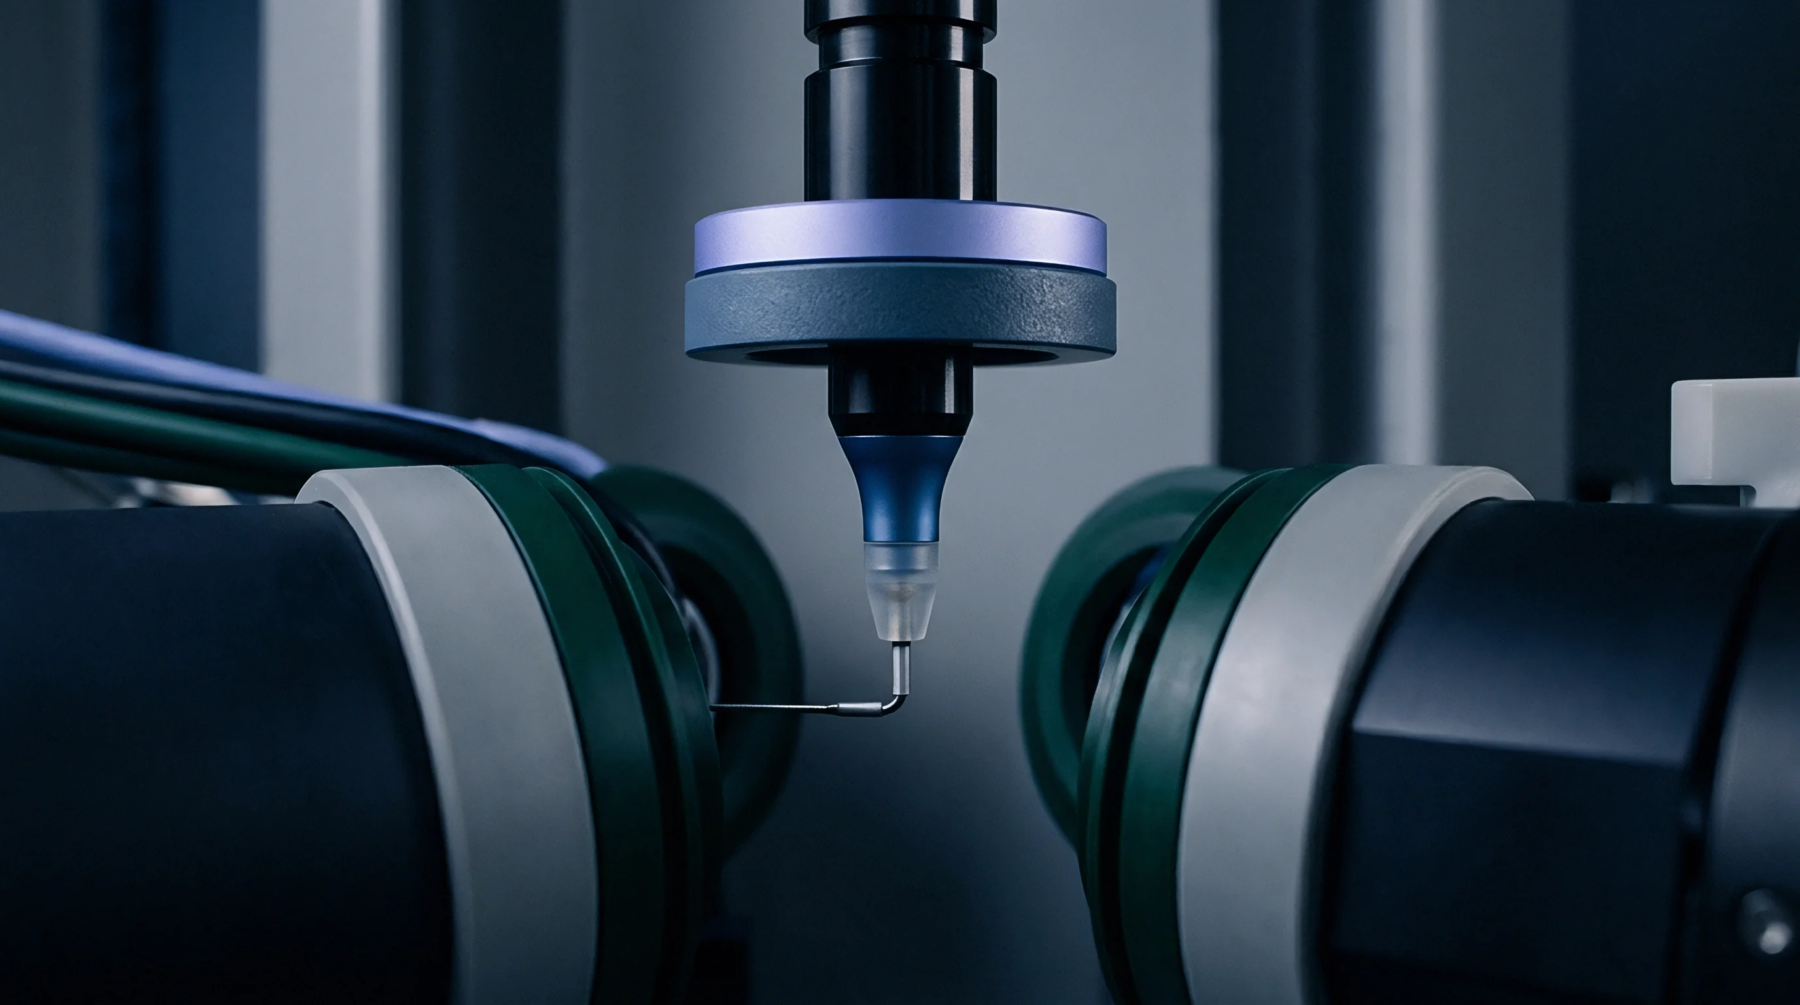
Machining sensor bores to strict concentricity tolerances and establishing direct picoCoulomb calibration scales cavity pressure for closed-loop process control.
Decoupled cavity pressure control decouples melt rheology from machine mechanics, fixing peak pressure to guarantee tight dimensional stability.
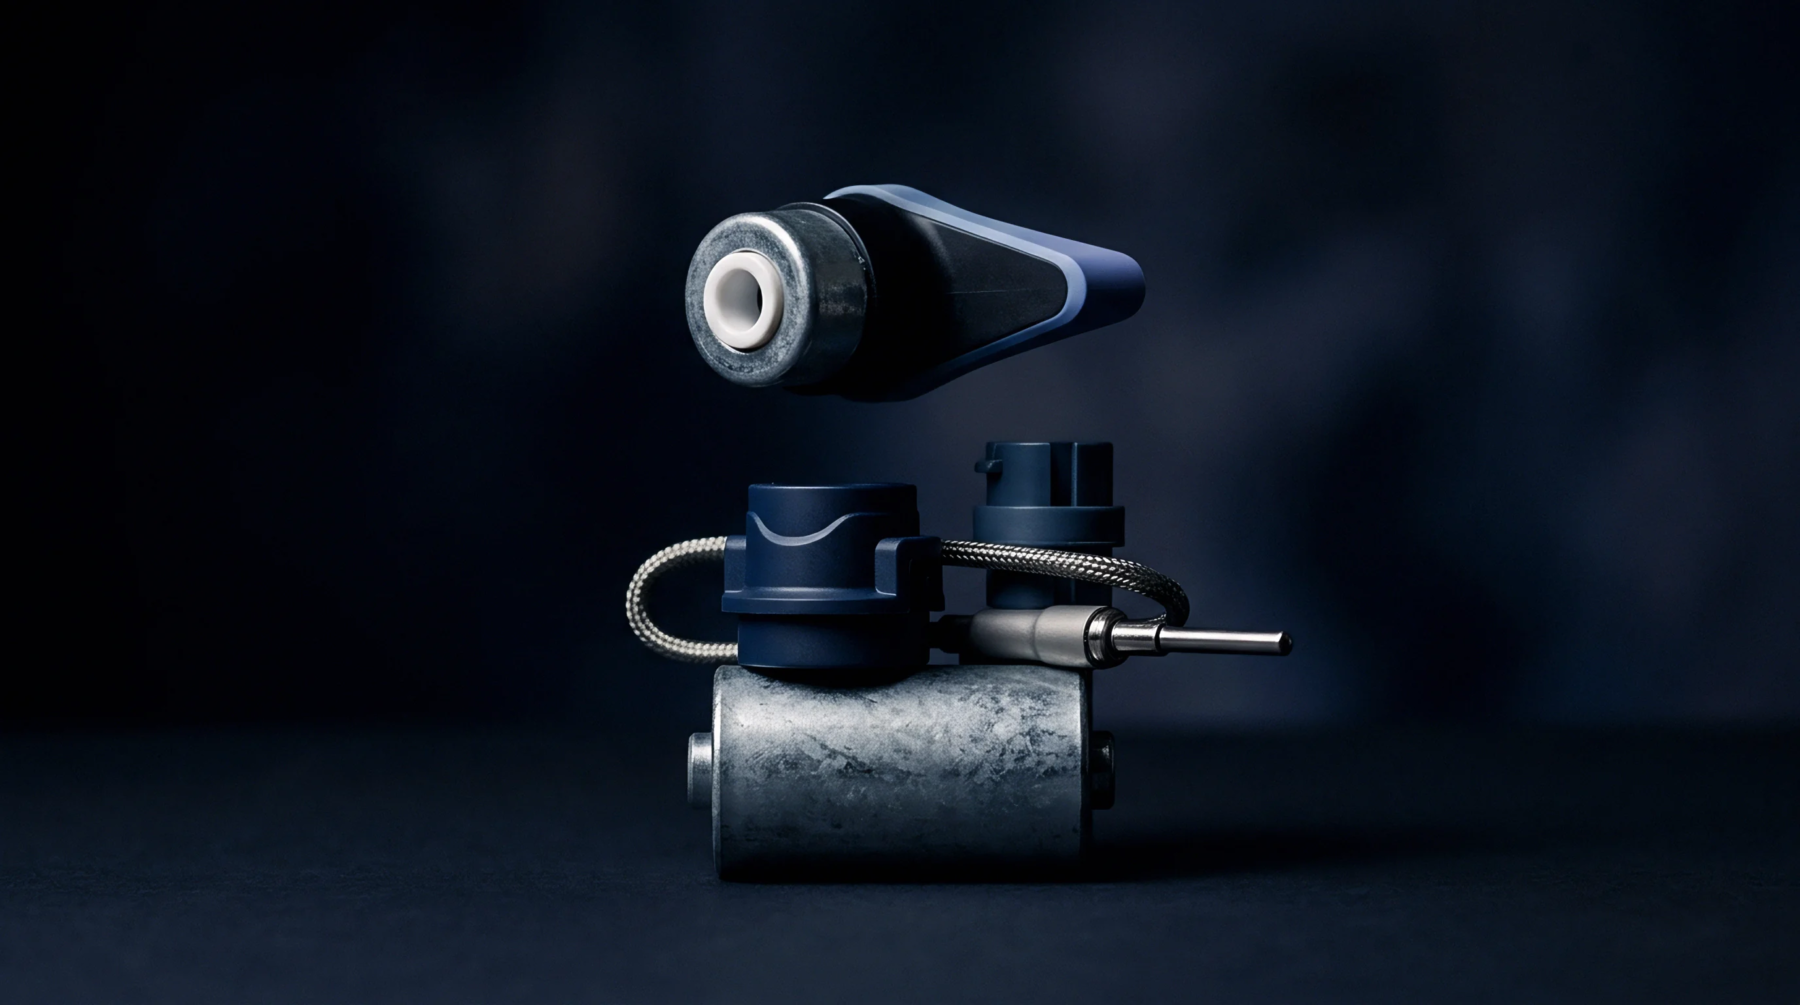
Cavity sensor integration requires rigid pocket machining, protected wire routing, and direct melt placement to decouple press dynamics from part tolerance.
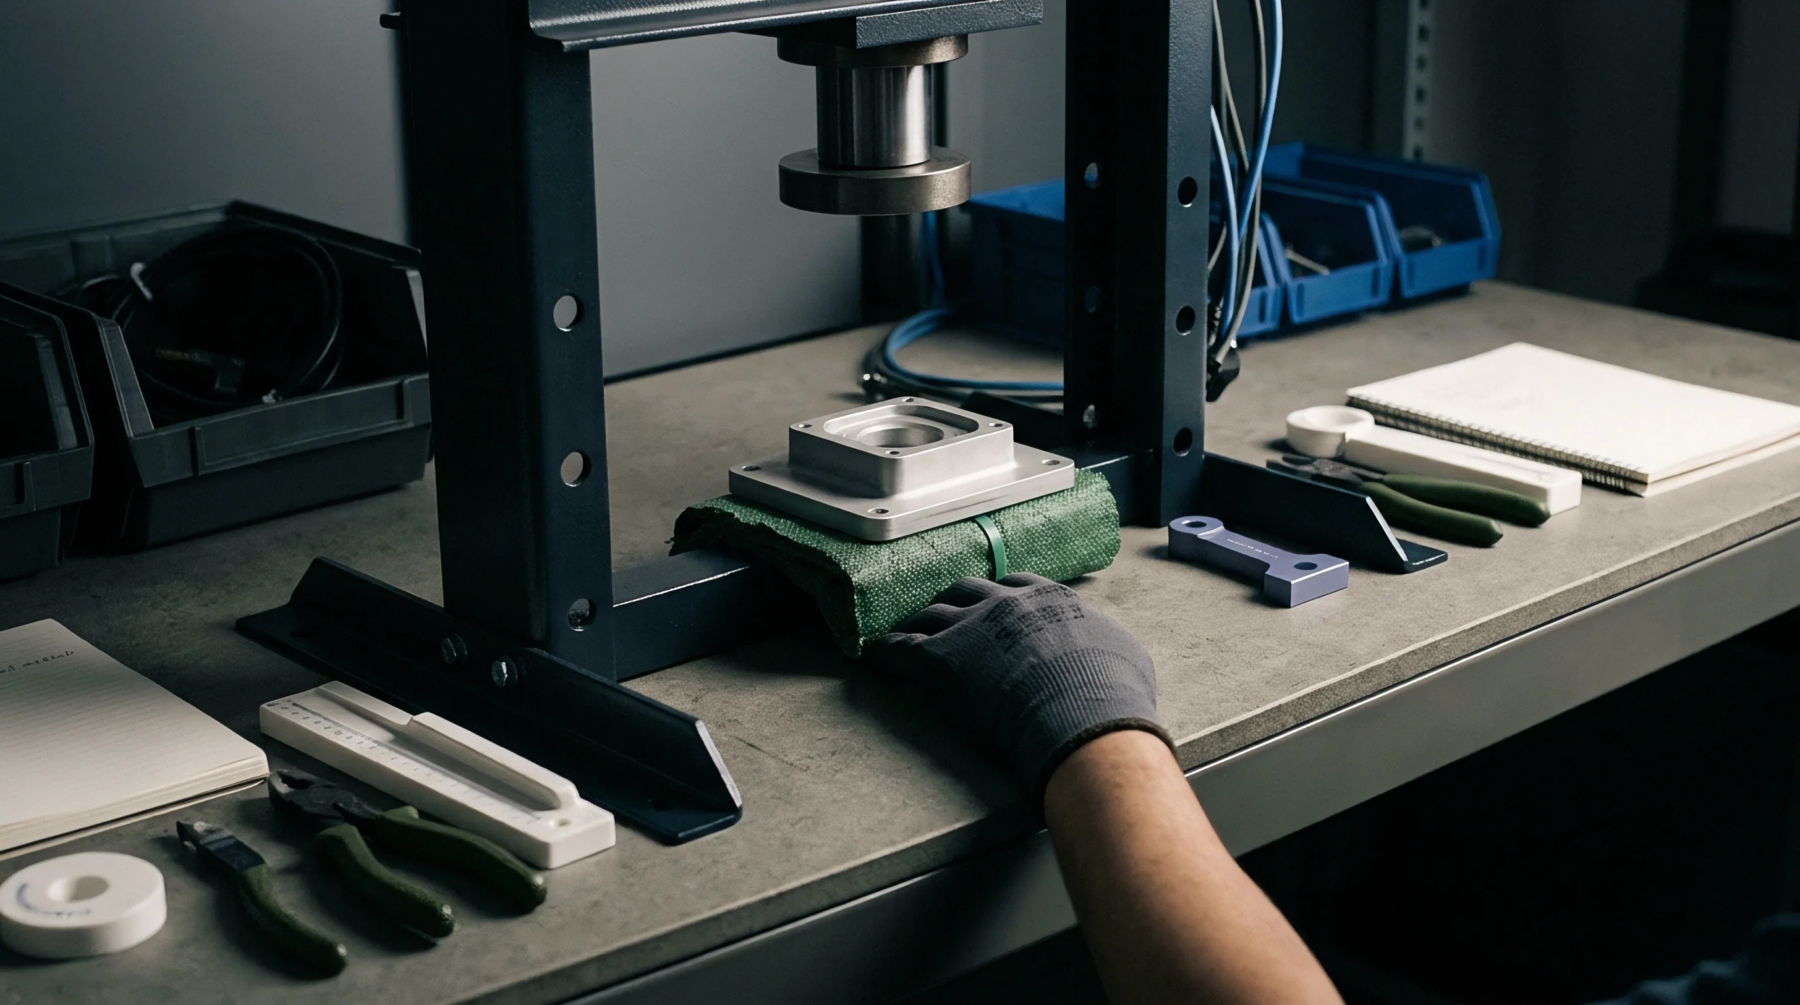
Predicting parting line wear and deflection requires balancing support pillar layouts, steel hardness, and thermal expansion gaps against resin flash limits.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.