Optimizing Melt Channel Bifurcations to Eliminate Shear Heating Viscosity Gradients
Optimizing melt channel bifurcations with melt rotation geometry and stepped hydraulic diameters eliminates shear-induced viscosity gradients across cavities.
Split
A first shot ejected from an unheated eight-cavity cold runner tool lands on the inspection bench with a four-gram mass disparity between inner and outer cavities. Part weights on the inner positions register 28.4 grams while outer positions stall at 24.1 grams under identical velocity control. Toolmakers routinely attribute this discrepancy to thermal cooling line variations inside the tool steel or uneven gate land electrical discharge machining.
The actual mechanism sits inside the runner branches.
High velocity injection forces thermoplastic polymer against cooled tool steel, generating steep velocity gradients near perimeter walls. Polymer melt functions as a pseudoplastic, shear-thinning fluid governed by non-Newtonian fluid mechanics. As molten resin shears against the stationary steel boundary, localized mechanical friction generates viscous dissipation.
This frictional dissipation elevates the melt temperature within a narrow annular boundary layer directly adjacent to the frozen skin layer. The shear layer stays thin. Melt flowing through the center of the conduit remains insulated by the surrounding resin, maintaining its nominal barrel temperature.
Laminar flow prevails under injection moulding conditions, preventing transverse convective mixing between the heated outer boundary layer and the cooler central core.
Geometrically balanced runner branches create rheologically unbalanced cavity fill patterns whenever non-Newtonian melts make consecutive ninety-degree turns.
Standard eight-cavity H-style layouts route fluid along pathways of identical physical length and bore diameter. Machining identical runner lengths, trapezoidal profiles, and gate dimensions creates an illusion of volumetric symmetry. When the primary melt channel reaches the initial tee junction, the flow splits evenly into secondary conduits.
The thermal distribution across the cross-section of each secondary channel becomes asymmetrical immediately following this turn. The high-shear, heated outer laminate from the primary feed travels selectively into one side of the secondary branch, while the cooler, higher-viscosity core occupies the opposing side. As this fluid approaches the tertiary split, the outer and inner bifurcations peel off distinct thermal laminates.
Outer cavities receive hotter material. Inner cavities receive colder resin from the un-sheared core of the primary runner stream. Because polymer viscosity drops exponentially with increasing temperature and shear rate, the hotter resin flows with reduced hydraulic resistance.
The inner cavities short out. Unequal cavity filling produces structural defects that standard machine profile adjustments cannot correct without introducing secondary flaws.
- Differential volumetric shrinkage induces post-moulding part warpage across symmetrical assemblies, causing dimensional rejections under coordinate measuring machine audits.
- Localized flash formation appears on inner cavities running hotter, lower-viscosity melt while adjacent outer cavities on the same shot exhibit hesitation marks.
- Non-uniform gate freeze times cause packing pressure variations across impressions, creating sink marks and internal voids in parts fed by colder runner streams.
- Weld line weakness develops when cooler melt fronts merge downstream at degraded thermal bonding temperatures, lowering drop-impact fracture resistance.
Toolmakers frequently assert that slight differential heating on runner heaters compensates for unbalanced filling, deflecting attention from geometric melt imbalance.
Dissipation
Mechanical energy from the machine screw converts directly into heat via internal fluid friction as macromolecules slide across one another. The magnitude of this temperature rise depends on the shear rate, polymer thermal conductivity, specific heat capacity, and the local shear viscosity function. At injection velocities between 100 and 300 millimeters per second, wall shear rates inside tertiary runner channels exceed 10,000 reciprocal seconds.
In technical resins such as glass-filled polyphthalamide and polybutylene terephthalate, local wall temperatures elevate by 15 to 30 degrees Celsius above nominal melt settings.
Viscous heating alters the core temperature. The Cross-WLF viscosity model describes how the shear rate and local temperature interact to dictate fluid resistance across the channel profile. As wall shear heating intensifies, local viscosity drops by 40 to 70 percent along the runner perimeter.
High shear thins the boundary polymer. The cold core retains high viscosity, traveling as a solid plug through the runner centerline. When this stratified plug reaches a traditional tee bifurcation, the division of fluid shears the boundary layers unevenly.
Does Melt Rotation Eliminate Thermal Stratification?
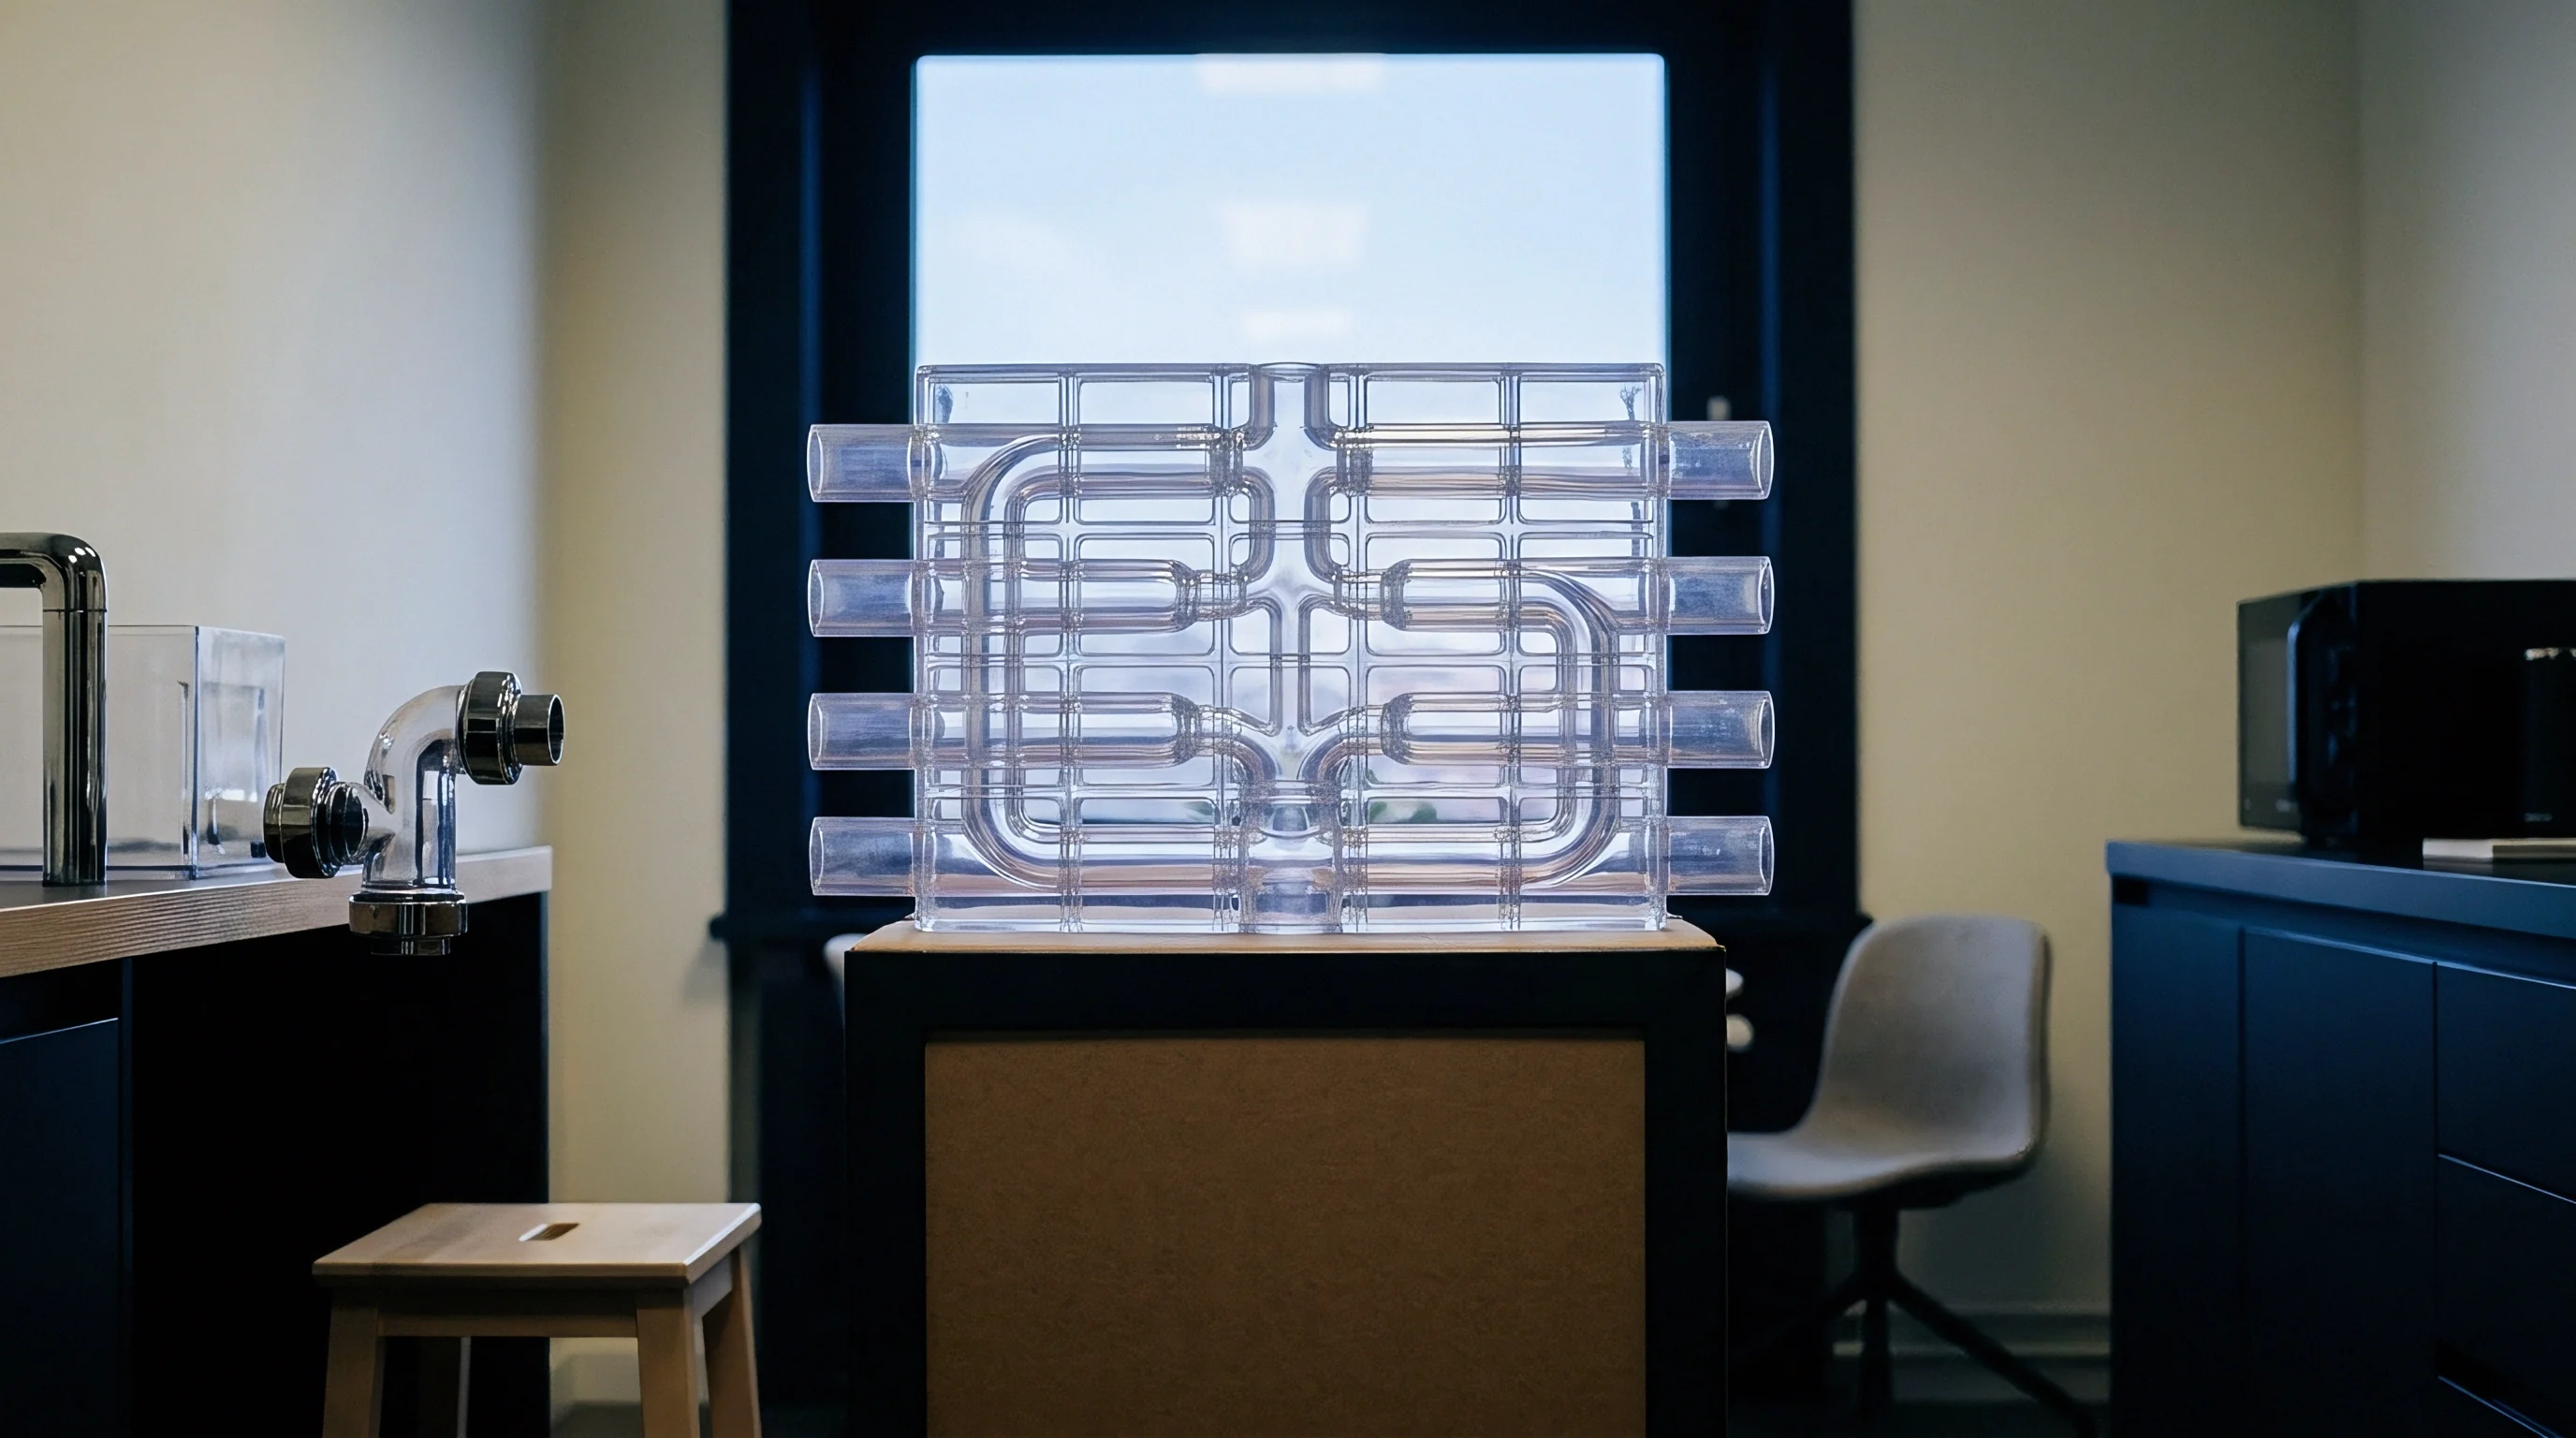
Repositioning high-enthalpy fluid elements from outer runner walls to the central core arrests non-uniform filling across downstream cavities. Melt rotation geometries divide the incoming melt stream and turn its cross-section through ninety degrees before subsequent branch junctions. Shear-induced melt rotation technology repositions the hot, sheared outer layer to the neutral centerline of subsequent channels, redistributing thermal energy symmetrically between left and right cavity feeds.
Tool builders without licensing agreements for specialized melt-flipper inserts often attempt to machine static mixing pins or restrictive flow dams at runner bifurcations. Static pins increase total system hydraulic pressure drop by 25 to 45 bar, compounding viscous dissipation rather than mitigating its gradient. Restrictive dams create stagnant dead zones where heat-sensitive resins degrade during extended cycle times.
Melt flippers rotate stratified layers. Repositioning the thermal boundary layer via three-dimensional runner geometry preserves total volumetric flow without accelerating thermal degradation.
A shear rate of 8,500 reciprocal seconds inside a 6 mm runner branch elevates local polycarbonate melt temperature by 14.2 degrees Celsius within 45 millimeters of linear travel.
The figure of 14.2 degrees Celsius rests on capillary rheometer test data compiled under ASTM D3835 at a 280 degrees Celsius barrel reference for a medium-viscosity polycarbonate, assuming an adiabatic wall boundary. In actual production, heat transfer into tool steel tempered at 85 degrees Celsius dissipates roughly 35 percent of this energy. Faster injection speeds or higher mold temperatures shift this localized temperature excursion upward, expanding the viscosity gap between split streams.
Nahme Number Thresholds in Technical Resins
Coupling between temperature-dependent viscosity and internal heat generation dictates whether thermal runaway destabilizes laminar conveyance. The dimensionless Nahme number quantifies this balance. When the Nahme number remains below 0.1, thermal conduction into the mold steel outpaces internal viscous dissipation, maintaining stable viscosity across the runner radius.
When injection velocity forces the Nahme number above unity, viscous dissipation outstrips thermal conduction, generating extreme temperature gradients.
The Nahme number exceeds unity. Semi-crystalline polymers exhibit sudden changes in thermal diffusivity and specific heat as they transition across melt crystallization temperatures, compounding the severity of Nahme instability. Liquid crystal polymers and polyphenylene sulfide present high Nahme values at modest shear rates, requiring conservative runner velocity profiles.
| Resin Designation | Nominal Melt Temp (°C) | Viscosity at 10⁴ s⁻¹ (Pa·s) | Thermal Diffusivity (mm²/s) | Calculated Nahme Number | Adiabatic Temp Rise (°C) |
|---|---|---|---|---|---|
| PA66 (Unfilled) | 285 | 28.5 | 0.082 | 1.42 | 18.6 |
| POM Copolymer | 205 | 42.1 | 0.075 | 1.88 | 22.4 |
| PC (Medium Flow) | 295 | 65.0 | 0.098 | 2.15 | 27.9 |
| PBT 30% GF | 260 | 52.3 | 0.112 | 1.64 | 21.1 |
| LCP (Vectra A130) | 340 | 14.8 | 0.135 | 3.10 | 34.5 |
| Calculations assume a circular runner diameter of 5.5 mm, volumetric delivery rate of 45 cm³/s, and thermal data derived from standardized capillary rheometry across 1 mm capillary dies. | |||||
Hydraulic pipeline engineering in civil petroleum distribution manages viscosity through line tracing and boundary layer heating to cut pumping power over long distances. High-pressure injection tooling reverses this objective entirely, requiring the tool designer to suppress localized thermal development so that fluid resistance remains uniform at every branch tip.
Thick runners cool slowly, while thin runners generate heat.
Branch
Primary feed lines distribute material outward toward secondary and tertiary runners through abrupt ninety-degree junctions. Standard machining practice employs full-round or parabolic runners cut via matching CNC ball end mills across cavity and core plates. Sharp interior corners at branch intersections generate localized shear spikes where boundary fluid accelerates around the pivot radius.
Radiusing bifurcation corners minimizes local pressure drop while maintaining symmetrical velocity distribution into diverging channels.
Pressure drops rise steeply downstream. Expanding runner diameters counteracts pressure decay, yet over-dimensioned runners extend cooling time, increasing cycle duration and regrind generation. The hydraulic diameter must taper logically at each successive branching generation to preserve balanced flow velocity and wall shear stress.
Channel Diameter Ratios across Branch Generations
Sizing successive runner segments requires balancing volumetric flow rates against cumulative pressure drop through the feed system. If the primary runner diameter equals d_1, sizing subsequent branches according to a volumetric flow retention rule yields a diameter ratio where d_2 equals d_1 multiplied by the reciprocal of the square root of the branching count. For a two-way branch, maintaining constant wall shear rate dictates that the branch diameter equals the incoming diameter multiplied by 0.794.
Toolrooms that machine uniform channel diameters throughout the entire layout drop the wall shear rate by more than 50 percent at each split. Lower shear rates in downstream branches permit premature cooling of the thermal boundary layer, causing unpredictable filling behavior across cavitation tiers. Maintaining a target shear rate between 1,000 and 5,000 reciprocal seconds across all runner generations preserves predictable non-Newtonian flow behavior from machine nozzle to cavity gate.
Cold outer runner boundaries track into part perimeters unless melt rotation geometry redirects fluid laminations before the final gate branch.
| Branch Generation | Conduit Count | Target Diameter (mm) | Flow Velocity (mm/s) | Wall Shear Rate (s⁻¹) | Hydraulic Loss (bar) |
|---|---|---|---|---|---|
| Primary (Spur) | 1 | 7.50 | 385 | 2,050 | 18.4 |
| Secondary | 2 | 5.95 | 308 | 2,070 | 24.2 |
| Tertiary | 4 | 4.72 | 246 | 2,090 | 31.6 |
| Drops (Gate Feed) | 8 | 3.75 | 196 | 2,110 | 42.1 |
Where Do Viscosity Variations Shift Cavity Pressure?
Downstream gates encounter non-uniform melt fronts during dynamic fill, altering pack density across outer and inner part locations. When hot, sheared material enters Cavity 1 while cooler core material enters Cavity 2, the dynamic viscosity at gate freeze differs by a factor of two. Cavity transducers record asymmetric filling rates.
The hotter cavity continues packing long after the colder cavity gate has sealed, producing high internal stress, crystalline variation, and dimensional divergence.
Tool design reviews require detailed examination of runner bifurcations prior to steel cutting. The checklist below establishes the physical and rheological criteria for bifurcation layout sign-off:
- Channel diameter stepping preserves wall shear rates between 1,500 and 4,000 reciprocal seconds across successive branching tiers without generating dead spots.
- Corner blend radii measure at least half the incoming runner diameter to eliminate flow separation and localized shear concentration at bifurcation corners.
- Cold slug well extensions extend past every junction by a length equal to 1.2 times the incoming runner diameter to trap stagnant boundary skin layers.
- Melt inversion geometries sit at the secondary-to-tertiary split on layouts exceeding four cavities to balance thermal boundary distribution across all drops.
- Parting line matching tolerances hold within 0.015 millimeters across runner plates to prevent flash formation and asymmetrical shear generation at channel perimeters.
Whether three-dimensional curved splitters fully eradicate second-generation thermal banding across semi-crystalline polyamides remains unsettled across production toolrooms.
Proof
Press-side setters detect unbalanced filling through progressive injection velocity cuts during initial tool trials. First-shot protocols isolate the filling phase from packing influence by setting holding pressure to zero and cutting injection stroke volume. Short-shot evaluations identify mechanical imbalance instantly.
Thermal gradients induce uneven gate freeze. Setters observe that parts from inner runner drops fill completely while outer cavities present short shots of 80 percent nominal volume under identical transfer positions. The setter verifies that volumetric delivery matches cavity volume by tracking short-shot progression across systematic fill percentages.
Short Shot Progression across Cavitation Tiers
Stepping machine injection volume from forty percent to ninety-five percent fill exposes physical imbalances among mold cavities. In an unbalanced layout, the imbalance manifests as a distinct filling sequence that remains fixed regardless of injection velocity increases.
- Mount the tool in an electric press, bringing steel temperatures and barrel heating zones to verified setpoints under equilibrium conditions.
- Disengage holding pressure completely, setting transfer position to trigger via screw position when the shot reaches forty percent nominal part volume.
- Inject resin at production velocity, eject the resulting short shots, and record the mass of plastic delivered to each cavity location.
- Advance the transfer position in ten percent increments, ejecting and weighing parts at each step up to ninety percent fill volume.
- Plot cavity fill percentage against shot position to quantify the filling disparity between inner and outer cavitation tiers.
- Analyze part weight spread across the array, verifying that fill variation stays below three percent across all positions.
Tool deflection widens part tolerances. When cavity filling proceeds asymmetrically, injection pressure exerts non-uniform opening forces across the mold parting line. The side receiving hotter, lower-viscosity melt fills first, creating localized mold separation while outer cavities are still filling under dynamic pressure.
This separation causes localized flash, parting line pitting, and long-term damage to alignment leader pins and interlocks.
Sensor Signatures in Multicavity Tooling
Piezoelectric transducers mounted behind ejector pins track dynamic melt front arrival across distinct quadrants of the mold base. In balanced systems, pressure traces from Cavity 1 and Cavity 8 overlay cleanly, showing identical arrival times, peak cavity pressures, and pressure decay rates during cooling. Shear heating imbalances deform these traces into divergent paths.
Specification of DIN 16742 TG4 tolerances forces rejection of mold components showing cavity pressure variations exceeding seven percent across quadrant branches.
A cavity pressure variation threshold of seven percent rests on production monitoring standards across thirty-two-cavity medical syringe barrel molds running polypropylene at a 12-second cycle time. Tooling for less demanding consumer housings permits pressure spreads up to fifteen percent before dimensional scrap surfaces. The tighter seven percent limit ensures that volumetric shrinkage remains identical across tight-tolerance core pins where diametrical drift cannot exceed 0.020 millimeters.
The desk cannot defend a definitive universal sensor pressure divergence threshold for glass-fiber filled polyphenylene sulfide components due to variable fiber orientation effects across gate lands. Sourcing engineers encountering this uncertainty mandate pre-production multi-cavity weight studies across three distinct shift lots, rejecting tools whose weight variation exceeds 1.5 percent of nominal part mass.
Unbalanced filling generates variable part weights, uneven shrinkage, warped show surfaces, and rejected quality lots during unattended shifts.
Margin
Tooling purchase orders balance initial steel machining capital against piece-part scrap yield during production life. Sourcing engineers frequently accept traditional H-pattern cold runner quotes because toolmakers quote lower initial fabrication hours. A sixteen-cavity tool built without melt rotation inserts costs roughly 12,000 dollars less during initial machining.
That initial saving vanishes during the first production run.
Steel rework costs mount rapidly. When parts fail dimensional qualification under coordinate measuring machine scans, the moulder alters gate lands, grinding down gates on lagging cavities and welding shut gates on fast cavities. Modifying gate diameters artificially balances fill time at a single injection speed, but destroys balance whenever the press technician adjusts barrel temperatures or injection rates to clear cosmetic flaws.
Artificial gate sizing creates an unstable, knife-edge process window.
Tool Steel Modification and Rework Economics
Correcting an unbalanced thirty-two cavity runner through electrical discharge machining adds machine shop hours and press downtime. Re-machining hardened tool steel inserts typically incurs 8,500 to 18,000 dollars in direct toolroom labor, accompanied by two to four weeks of lost production schedule. If the runner modification requires welding and re-cutting runner plates, heat-affected zones degrade steel fatigue limits, shortening total tool life from one million cycles to fewer than 600,000 cycles.
Scrap rates compound across shifts. An uncorrected shear heating gradient producing a 3.5 percent scrap rate on a high-speed packaging tool destroys operating margins across high-volume contracts. A thirty-two cavity tool cycling every eight seconds generates 14,400 parts per hour.
At a 3.5 percent scrap rate, the press generates 504 rejected parts every operating hour, converting resin directly into regrind and consuming machine-hour allocations without generating salable inventory.
| Evaluation Metric | Standard H-Pattern Runner | Artificial Gate Balancing | Engineered Melt Rotation Runner |
|---|---|---|---|
| Initial Tooling Expense | $82,000 | $82,000 | $96,500 |
| Toolroom Rework Costs | $0 | $14,200 | $0 |
| First Article Qualification Time | 3 Weeks | 8 Weeks | 2 Weeks |
| Production Scrap Rate (%) | 4.2% | 2.8% | 0.4% |
| Annual Resin Scrap Cost (10M Units) | $46,200 | $30,800 | $4,400 |
| Net Cost Over 10 Million Parts | $128,200 | $127,000 | $100,900 |
Amortisation Bands across High Cavitation Programs
Financial models for medical closures and thin-wall connectors allocate upfront mold expense against tight unit pricing. Amortising the additional 14,500 dollars required for melt rotation inserts across a production run of ten million units adds 0.00145 dollars per part. The resin savings achieved by lowering scrap from 4.2 percent to 0.4 percent delivers 0.00418 dollars in immediate piece-price reduction, recovering the tooling premium within the first 3.5 million shots.
Sourcing agreements must address the commercial liability of runner-induced dimensional variation before tool design freezes. Tooling agreements that define balance purely by geometric layout leave the buyer unprotected against shear-induced filling variations. Procurement specifications require explicit melt-balance clauses tied to physical part attributes across all cavities under production speeds.
A tooling purchase contract clause specifying cavity-to-cavity weight variance within DIN 16742 Group 130 limits reallocates the financial burden of manifold rework directly to the toolmaker.