Designing Naturally Balanced Hot Runner Manifolds for Precision Injection Moulding
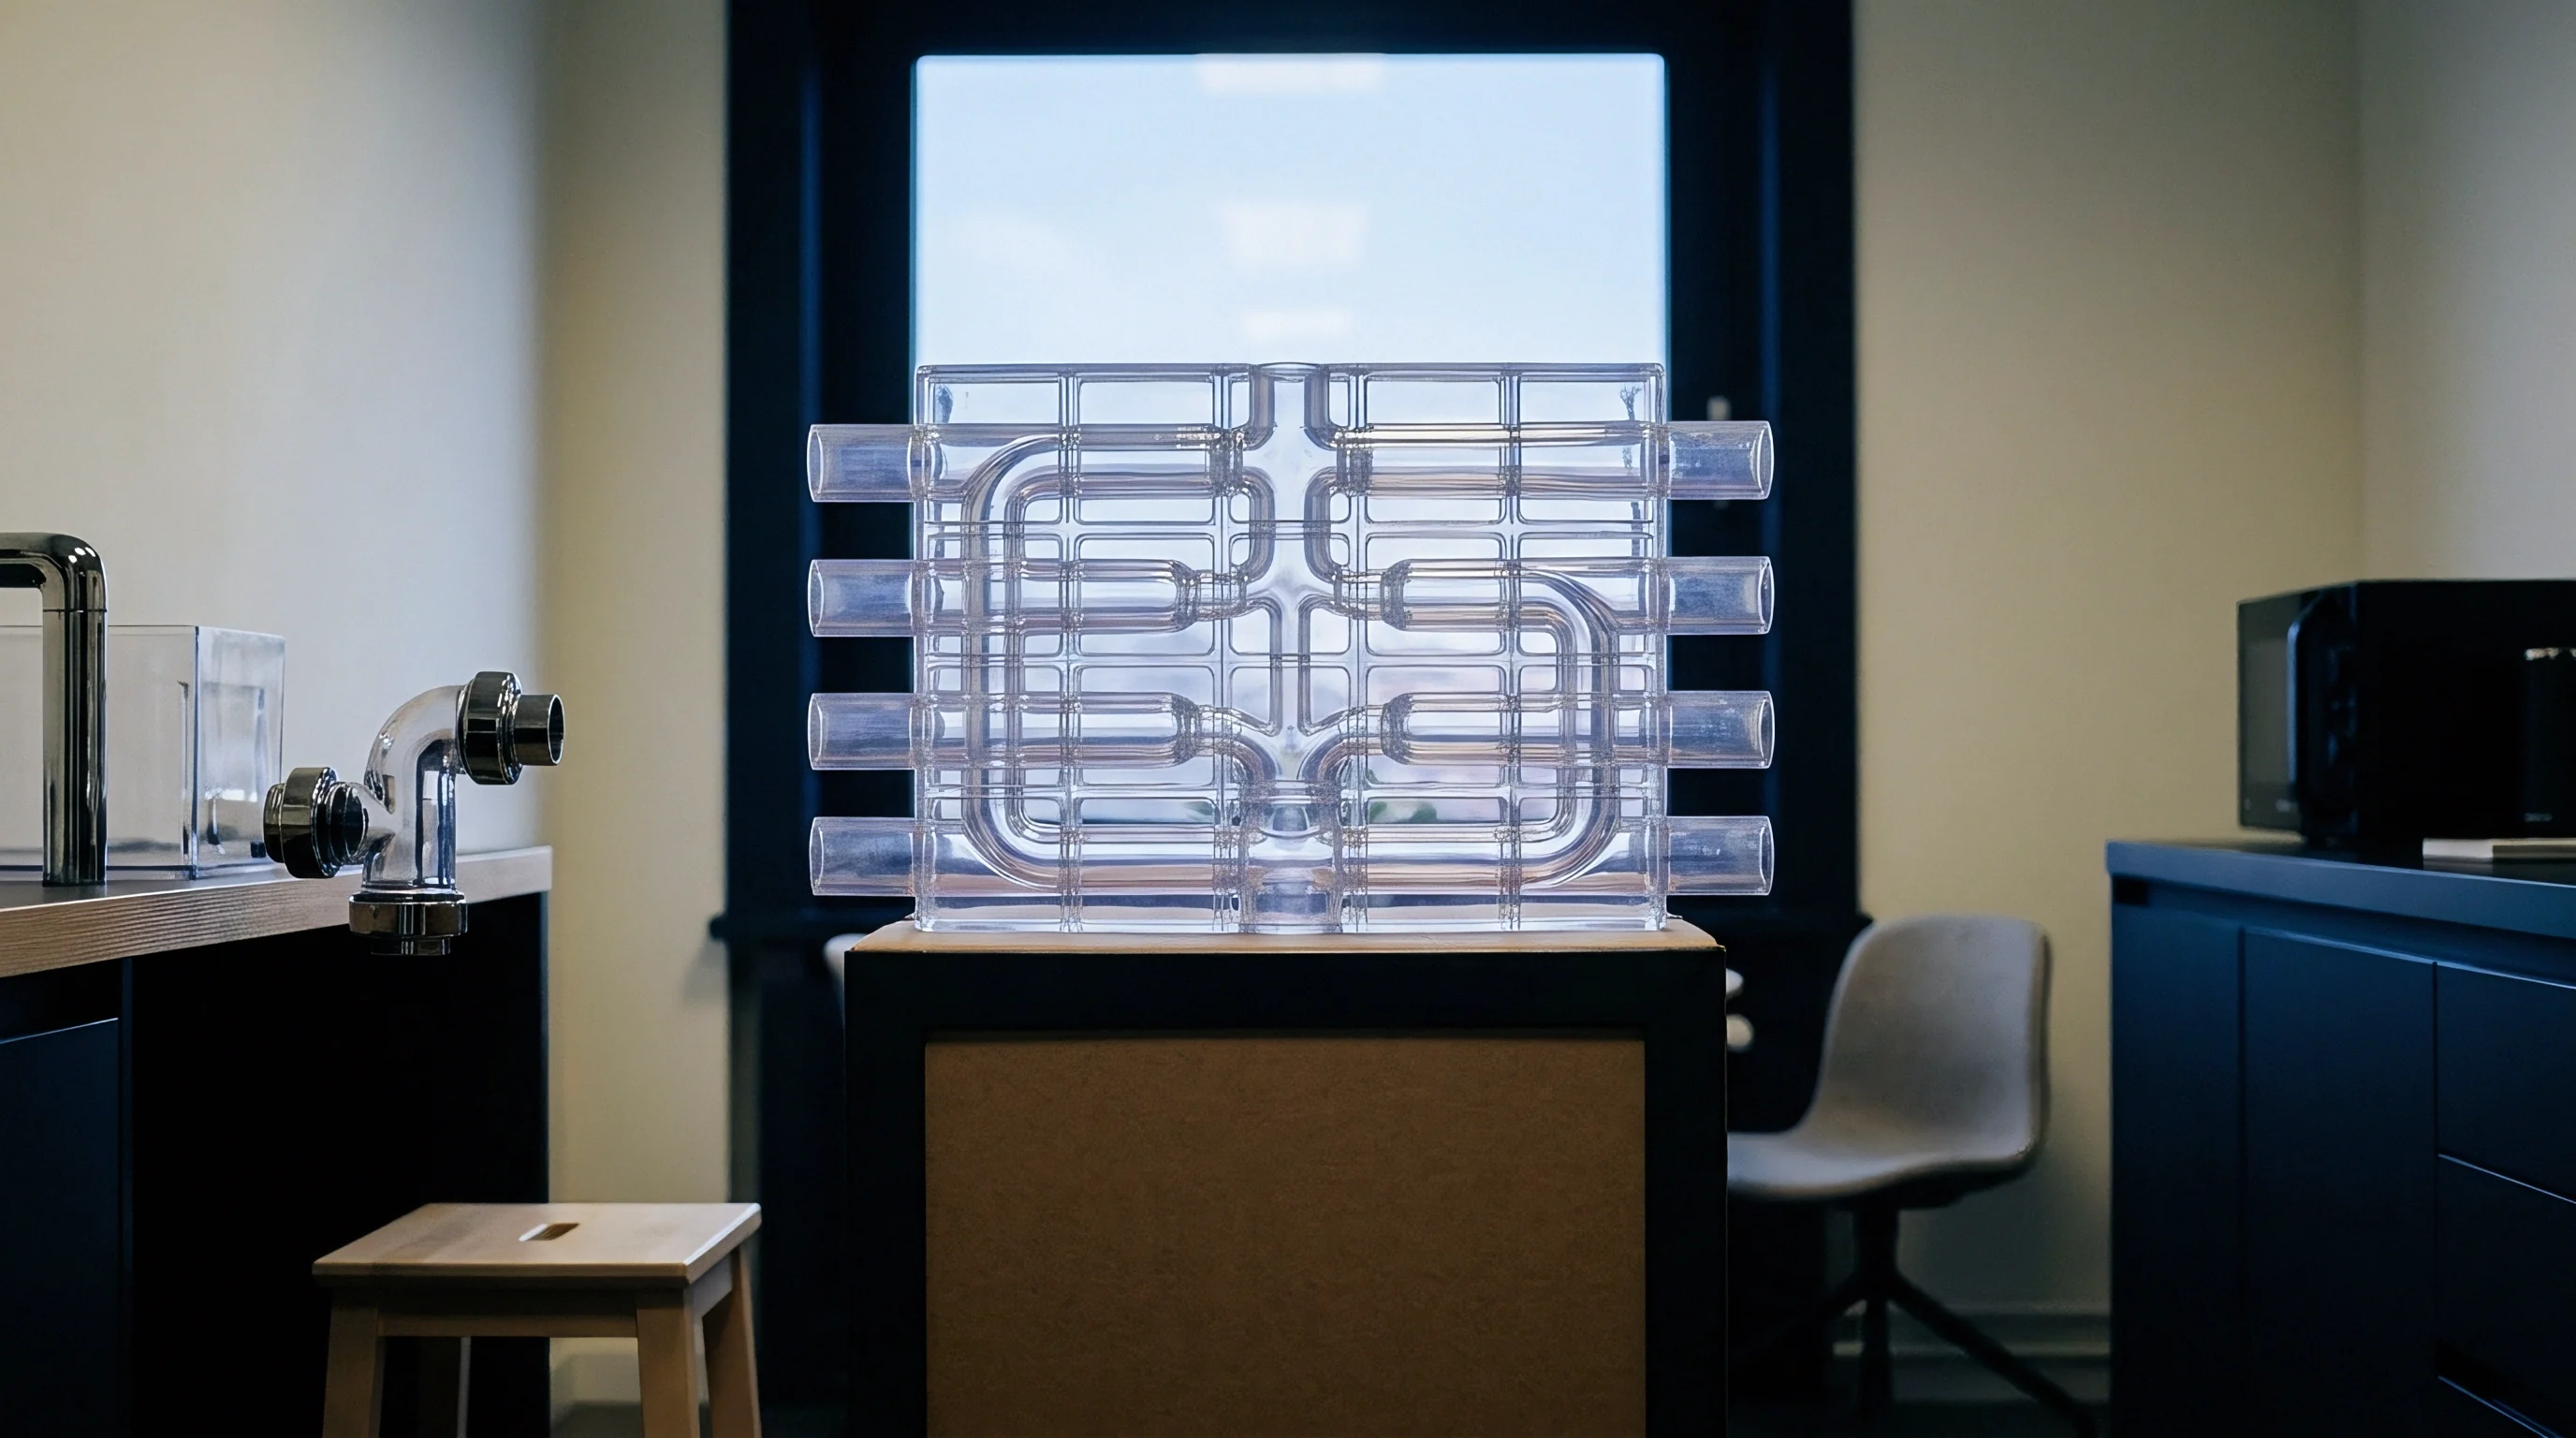
Naturally balanced manifolds require symmetrical 3D runner geometry, smooth transitions, and uniform thermal zones to ensure identical cavity filling.
Layout
Symmetric Branching Architecture
Precision injection tooling demands identical melt history across every flow path. In multi-cavity tools running technical polymers such as polyoxymethylene or polybutylene terephthalate, volumetric variation between cavities originates in the distribution manifold. A naturally balanced runner matches the flow length, channel diameter, bend angles, and internal surface transitions identically from the main sprue bushing to every terminal drop.
Geometrical balance ensures that resin travels identical path lengths under uniform driving pressure.
Geometric balance alone does not guarantee identical cavity fill rates. Non-Newtonian polymer melts undergo high wall shear that alters local viscosity profiles. A manifold split that mirrors geometry while rotating the shear planes creates substantial melt differences.
The inner fluid layers retain heat and experience lower effective viscosity, whereas the outer layers undergo extreme shear thinning before cooling near the boundary walls. When this stratified melt splits at a standard tee intersection, the low-viscosity core enters one downstream branch while the highly sheared perimeter diverts into the other.
A dimensional tolerance of five microns across multi-cavity medical housings collapses when shear-induced melt stratification produces cavity-to-cavity weight variations exceeding two percent.
Tool designers eliminate this variation by configuring runner junctions in three dimensions. Symmetrical branching layouts maintain identical primary, secondary, and tertiary channel lengths while managing flow splitting symmetrically. Pitch spacing dictates manifold outer dimensions, heater bore proximity, and tie-bar clearance inside the moulding machine.
Selecting an eight-drop, sixteen-drop, or thirty-two-drop configuration sets the physical envelope of the hot half before steel arrives at the machining centre.
Cavitation arrangements follow distinct branch generations. Two drops use an inline split. Four drops configure as an X-pattern or an H-pattern.
Eight drops require an H-pattern with identical secondary arms or a radial star configuration. Moving to sixteen or thirty-two cavities establishes successive binary forks where channel diameters step down at each generation to preserve linear velocity without generating excessive pressure drop.
The tooling buyer evaluates the physical envelope against machine platen spacing. A thirty-two-drop H-manifold requires substantial plate thickness to accommodate runner bore diameters, heater elements, clearance gaps, and backer support disks. Skimping on plate depth introduces plate bending under clamp tonnage, causing internal melt leaks around the nozzle seals.
Shear
Rheological Stratification across Branching Splits
Polymers exhibit pseudoplastic shear-thinning behavior inside runner bores. Fluid layers against the hot steel wall experience shear rates exceeding ten thousand reciprocal seconds, while fluid in the bore centre experiences negligible shear. As the polymer proceeds through a runner, this gradient produces an annular temperature and viscosity distribution.
The melt against the wall becomes hotter and less viscous than the core melt.
Planar manifold splits separate this fluid non-uniformly. In a standard two-plate branching runner where a secondary runner branches perpendicularly from a primary runner, the split peels the high-shear outer boundary layer into one sub-channel and the low-shear central core into the opposite sub-channel. Downstream cavities receiving the sheared melt pack faster, freeze later, and yield different component dimensions than cavities receiving the core melt.
True natural balance incorporates melt-rotation geometry at successive branch intersections. Toolmakers machine specialized flow diverters or multi-level crossover channels that reposition the sheared boundary layer toward the centreline of the subsequent runner segment before the next bifurcation. Cavity pressure curves verify whether shear management succeeds.
When cavity pressure transducers record identical curves across all positions, the rheological balance matches the geometric layout.
Semi-crystalline engineering resins amplify balance discrepancies. Polyoxymethylene exhibits severe volumetric shrinkage changes across minute thermal bands. An unmitigated shear imbalance shifts the local crystallization temperature within individual cavities, resulting in out-of-round cylindrical features and uncontrolled differential warp.
Which Geometric Configurations Induce Velocity Skew?
Standard ninety-degree mitered intersections displace the high-velocity core toward the outer radius of downstream channels. The velocity profile remains skewed across several runner diameters downstream of the turn. If a subsequent bifurcation occurs before the velocity profile stabilizes, the downstream split receives asymmetrical flow volumes regardless of matching channel diameters.
Designing balanced manifolds requires sweeping transition radii at all runner turns. Toolmakers blend corners with generous fillets, typically matching or exceeding the runner radius, to limit flow separation zones. Stagnant fluid pockets at abrupt corners degrade heat-sensitive resins like polyvinyl chloride or polyamide 66, generating carbonized particulate that clogs terminal gate orifices.
| Channel Stage | Bore Diameter (mm) | Wall Shear Rate (1/s) | Effective Viscosity (Pa s) | Pressure Drop Per 100mm (bar) |
|---|---|---|---|---|
| Primary Inlet | 14.0 | 167.2 | 185.4 | 12.4 |
| Secondary Split | 10.0 | 458.4 | 122.1 | 24.8 |
| Tertiary Branch | 7.0 | 1336.8 | 76.5 | 58.2 |
| Drop Feed Bore | 5.0 | 3666.9 | 48.2 | 142.6 |
The relationship between bore diameter and shear rate governs the pressure budget. Reducing runner diameter restricts manifold melt volume and reduces residence time, but escalates injection pressure demands. Toolmakers calculate the shear stress at the channel boundary to prevent exceeding polymer degradation thresholds, maintaining shear stresses below zero point one four megapascals for unreinforced technical compounds.
In hot runner systems running long glass-fiber compounds, unchecked shear rates fracture glass filaments within the manifold runner bores before the melt reaches the cavity gate. Retaining mean fiber length above zero point seven millimeters requires keeping bore diameters wide and transition angles smooth. Tool designers sacrifice minimal residence time gains to preserve mechanical structural properties in the finished moulding.
Calculations show that secondary and tertiary bore diameters must scale down monotonically. A primary runner carrying volume for sixteen cavities transitions to secondary branches sized for eight cavities, then tertiary branches for four cavities. The cross-sectional area decreases at each stage, maintaining linear melt velocity between one hundred and three hundred millimeters per second.
Step transitions follow conical taper angles between fifteen and thirty degrees to prevent dead zones.
The processing window remains narrow when shear thinning is unmanaged. The setter spends hours compensating for cavity weight imbalances by tweaking individual nozzle tip temperatures. When a tool relies on thermal manipulation to offset hydraulic runner imbalances, seasonal ambient shifts and cooling tower drift destabilize the process, driving scrap rates upward during unattended production runs.
Bore
Drilling Integrity and Internal Surface Topography
Gun drilling forms the internal network of hot runner manifolds. Deep-hole drilling in alloy tool steels like 1.2311 or 1.2344 creates surface roughness, runout drift, and intersect burrs. Deep bores drift off true axis by up to zero point one millimeters per one hundred millimeters of depth.
When two long runner channels meet at a ninety-degree internal intersection, bore runout generates an offset step that disrupts flow symmetry and traps polymer.
Toolrooms eliminate drilling offset by drilling from opposing faces using guided pilot bushings and finishing intersection zones with custom contour endmills. Internal flow channels receive abrasive flow machining or extruded hone finishing. Abrasive slurry pumped through the manifold channels polishes interior surfaces to a mirror finish below Ra zero point two microns.
Smooth internal walls prevent stagnant polymer retention and reduce boundary friction.
A surface roughness exceeding Ra zero point eight microns inside runner intersections generates thermal degradation pockets that release carbon flecks into technical mouldings.
Intersections require specialized end-plugging methods to prevent polymer leakage under high injection pressure. Machinists drill runner passages from the manifold exterior, crossing internal junctions before plugging the outer entry holes. Threaded plugs backed by brazing or specialized metal-to-metal interference fit taper plugs seal these passages.
A failed plug allows resin to bleed into the heater pockets, destroying electrical circuits and halting production.
The hot runner manifold block must withstand continuous hydraulic internal pressures between eight hundred and two thousand bar at elevated operating temperatures. Toolmakers evaluate mechanical hoop stress across the runner bore walls. The minimum steel ligament thickness between adjacent runner bores, heater slots, and thermocouple pockets must exceed one point five times the channel diameter to prevent manifold wall rupture or plastic deformation under peak injection packing pressures.
Pre-hardened tool steels provide adequate strength for non-corrosive commodities, whereas fluoropolymers and flame-retardant resins demand electro-slag remelted stainless steels such as 1.2083 or 1.4112 hardened to fifty-two Rockwell C. Uncoated carbon steels pit rapidly when exposed to aggressive off-gassing additives, ruining internal surface polish within fifty thousand cycles.
Plugs must match the base manifold material thermal expansion coefficient identically. Toolrooms employ 1.2344 plugs within 1.2344 forged blocks, machining interference tapers to an angle of five degrees. The plug faces inside the melt bore are contour-milled flush with the runner inner diameter prior to final vacuum brazing.
Any recessed step or protruding lip generates an immediate eddy pool where stagnant material degrades.
The supplier will say that abrasive flow machining adds excessive expense to standard manifold construction and that reamed bore intersections provide sufficient surface quality for standard moulding runs.
Heaters
Thermal Zonation and Heat Sinks
Thermal homogeneity is mandatory for natural balance. An identical physical flow length fails to balance fill rates if one branch runs ten degrees colder than its symmetrical partner. Hot runner manifolds rely on swaged tubular heating elements pressed into precision-milled grooves along the top and bottom plates, or gun-drilled cartridge heaters arrayed across the steel block.
Manifold support pads and locator center pins conduct heat away from the block into the cold mould clamping plates. These contact points act as localized thermal sinks. A runner channel running adjacent to a support pillar drops in temperature, elevating the local viscosity of the resin inside that channel.
Cavities fed by this channel experience hesitations and fill delays compared to cavities fed through warmer zones.
Engineers counteract structural heat loss through calculated heater watt density profiling. Heating elements pack tighter coil spacing near outer edges and structural support blocks to offset conductive heat losses into the mold base. Independent thermocouple zones isolate branches, drops, and central sprue areas, maintaining temperature equilibrium across the steel within plus or minus one degree Celsius.
Air gaps between the hot manifold and the backing plates provide primary insulation. Toolmakers maintain a clearance gap between twelve and twenty millimeters across non-contact areas. Ceramic insulation boards or titanium support disks limit conductive losses at support points.
Titanium exhibits roughly one-third the thermal conductivity of standard mould steel, reducing parasitic heat transfer to the mould plates.
Thermocouple placement governs actual temperature control precision. Deep-well thermocouples must sit within six to ten millimeters of the melt bore wall. Positioning sensors too close to heating elements causes premature controller shutoff, leaving the melt channel cold.
Placing thermocouples too close to external air gaps causes overheating, charring the melt stream and degrading physical part properties.
What Diagnostic Checks Confirm Manifold Balance?
Validating balanced manifolds requires methodical press-side verification steps during tool commissioning. Setters rely on precise procedures to decouple thermal variation from hydraulic runner dynamics.
- Thermal soak stabilization demands bringing the manifold to operating processing temperature and holding equilibrium for a minimum of forty-five minutes before introducing resin, verifying that internal steel expansion settles and heat sink conduction stabilizes across all zones.
- Short shot progression analysis involves injecting non-packed melt steps from twenty percent to ninety-five percent fill volume with pack and hold pressures turned off, establishing volumetric fill uniformity across all cavities via high-precision mass measurement.
- Gate freeze confirmation evaluates individual cavity seal times through incremental packing duration steps, confirming that all nozzle tips freeze simultaneously under identical water cooling flow rates.
- Cavity pressure trace correlation compares peak filling pressures and pressure arrival times via piezoelectric transducers fitted behind ejector pins in every individual cavity, ensuring dynamic balance during rapid injection phases.
Thermal profiling requires multi-cavity thermocouple arrays during initial mold trials. Setters link infrared imaging of freshly ejected parts to individual cavity positions. Consistent part surface temperatures upon tool open confirm that melt arrives at identical thermal states across all gates.
Operating a sixty-four-cavity connector tool without zoned manifold regulation exposes the molder to cavity-dependent flash and sink defects. External edge drops lose heat to ambient frame components while inner drops stay insulated. The setter cannot resolve this variance by adjusting the main injection profile on the press interface.
Expansion
Thermomechanical Gaps and Structural Sealing
A hot runner manifold expands significantly from ambient assembly temperature to processing temperature. A manifold measuring five hundred millimeters in length expands by more than one millimeter when heated to two hundred and sixty degrees Celsius. Tool designs must account for thermal expansion to maintain alignment between manifold drops and stationary mould cavities.
Engineers calculate linear expansion based on the steel alloy coefficient of thermal expansion, the distance from the central locating pin, and the temperature differential between the hot manifold and the cold tool plate. Nozzle drops assemble with deliberate cold offsets. The drop bores in the manifold do not align with the gate inserts at ambient assembly room temperatures.
As the steel reaches target thermal equilibrium, the drops slide outward into alignment over the gate centres.
Sealing between manifold drops and cavity inserts relies on controlled interference preloading. Manufacturers design nozzle tips with sliding pressure collars or crush rings made from high-strength alloys like beryllium copper or hardened stainless steel. The stack dimension across the tool must produce calculated sealing force at operating temperature without yielding the steel.
A stack calculation error of zero point zero four millimeters will either crush nozzle tips under operating expansion or cause devastating plastic leakage behind the manifold plates.
Insufficient preload allows pressurised resin to breach the nozzle interface during peak injection velocity, flooding the manifold housing box with molten plastic. Excessive preload concentrates mechanical stress on the nozzle seats, causing cracked carbide tips, plastic deformation of the manifold block, or visible deflection marks across cavity show surfaces.
Backing disks and central locating dowels fix the manifold center point while permitting unrestricted outward radial growth. The central dowel secures the sprue bushing axis, forcing all thermal growth symmetrically outward toward the tool perimeter. This radial movement distributes mechanical forces symmetrically across all structural support pillars.
The mould designer manages plate deflection under clamp tonnage alongside thermal growth. When the injection press locks, clamping forces travel through the mould base backing plates, pressing support disks directly against the hot runner manifold. If the mould plates lack structural rigidity, platen deflection bends the manifold, compromising nozzle seal integrity and driving cavity weight variation.
The standard supply agreement must specify tool plate deflection under clamp tonnage to prevent sealing failures. The agreement sets allowable manifold deflection below zero point zero two millimeters across the full length of the runner block under full machine clamp force.
Amortisation
Tooling Investment and Piece-Price Realities
Precision naturally balanced hot runner manifolds carry significant tooling cost premiums over simple cold runner layouts or artificially balanced hot runner systems. Adding a sixteen-drop fully balanced hot runner system adds between twenty-five thousand and sixty-five thousand euros to the initial tool build invoice. Procurement teams must justify this capital expense against cycle time reduction and resin savings.
Cold runner systems generate solid plastic sprues that require granulating and recycling or disposal. In high-speed medical or packaging parts, cold runner volume can match or exceed finished component weight. Eliminating the cold runner removes forty to sixty percent of the shot weight, cutting raw material costs and shaving several seconds off the required cooling cycle.
Hot runners transfer melt directly into cavities without cooling thick distribution sprues.
| Tool Configuration | Cavity Count | Tool Capital Cost (EUR) | Cycle Time (s) | Scrap Rate (%) | Unit Cost at 5M Units (EUR) |
|---|---|---|---|---|---|
| Cold Runner Three-Plate | 16 | 72,000 | 18.5 | 4.2 | 0.089 |
| Artificially Balanced Hot Runner | 16 | 108,000 | 12.0 | 2.8 | 0.071 |
| Naturally Balanced Hot Runner | 16 | 134,000 | 11.2 | 0.4 | 0.064 |
| Naturally Balanced Hot Runner | 32 | 215,000 | 11.5 | 0.5 | 0.048 |
Artificially balanced manifolds use varying runner diameters or restrictor pins to force fill balance across asymmetric paths. These systems function within an exceptionally narrow processing window. When machine operators modify injection speed or when polymer lot-to-lot viscosity shifts by ten percent, the artificial balance fails.
This instability triggers cavity fill imbalances, dimensional scrap, and press downtime that wipe out the initial capital cost savings.
The capital expenditure evaluation must weigh scrap rate reduction in precision technical components. In tight-tolerance engineering assemblies, parts falling outside dimensional bands cannot be blended with virgin resin and remoulded. Symmetrical natural balance holds cavity-to-cavity dimensions inside DIN 16742 TG4 tolerance bands across millions of cycles, protecting landed part margins.
High-volume manufacturing programs break even on naturally balanced hot runner systems within months. Producing five million precision units on an unstable manifold layout costs far more in scrap, unscheduled sorting labour, and cavity lock-outs than the twenty-six thousand euro differential between an artificially balanced manifold and a fully balanced 3D-routed runner manifold.
Tool transfer disputes frequently erupt over manifold performance. Sourcing agreements must explicitly state hot runner balance metrics, defining allowable cavity part weight variance across all cavities under scientific moulding process parameters. A capable moulder accepts a maximum part weight variation of plus or minus zero point five percent across all cavities during factory acceptance trials.
Tool builders often propose artificial balancing to reduce manifold plate thickness and cut rough machining hours. This compromise saves minimal tool capital while permanently handicapping operational press stability. The procurement specialist must enforce naturally balanced geometry specifications in the tooling RFQ, rejecting artificial runner choking for any tool destined to run more than five hundred thousand shots over its production lifespan.
Qualification
Inspection Standards and Scientific Process Acceptance
Signing off on a multi-cavity precision tool demands clear acceptance protocols. Factory acceptance testing begins with a detailed steel metrology audit of the hot half, followed by dimensional verification of components produced under decoupled moulding conditions. The tool builder must demonstrate process capability indices exceeding one point six seven for all critical dimensions across all cavities simultaneously.
First article inspection reports must capture dimensional data grouped by cavity number rather than pooled into a single statistical distribution. Aggregating cavity measurements obscures systemic balance defects. A thirty-two-cavity tool displaying acceptable overall Cpk might conceal four corner cavities producing out-of-spec dimensions due to manifold thermal droop.
Clear cavity grouping exposes hydraulic and thermal imbalances instantly.
The mold qualification dossier must compile comprehensive operational proof before tool shipment.
- Channel metrology verification records computed tomography scans or endoscopic bore videos validating intersection polish, absence of drilling burrs, and exact runner split symmetry throughout the hot runner block.
- Pressure drop characterization measures manifold pressure loss using in-line melt pressure sensors under maximum rated injection velocities, confirming calculations match machine hydraulic readings.
- Short-shot weight distribution lists individual cavity weights from a series of ten consecutive unpressurized partial fill shots, proving the mass coefficient of variation remains below zero point seven five percent.
- Thermal uniformity certification details thermocouple performance logs across all zones during three continuous hours of operation, verifying steel block temperature bands hold within plus or minus one point zero degree Celsius.
- Pressure transducer overlay curves provide synchronized cavity pressure traces from all cavities showing simultaneous filling peak timing and identical packing decay rates.
A tooling agreement must protect the buyer against unserviceable hot runner assemblies. Standard contracts mandate that the supplier provide complete spare component packages including pre-wired heating elements, replacement thermocouple probes, spare nozzle tips, and seal rings manufactured within the original machining batch to ensure interchangeability.
Responsibility for scrap generated by chronic cavity imbalance rests entirely with the toolmaker if the hot runner manifold fails to meet pre-defined balance metrics. Sourcing managers enforce warranty holdbacks of ten to twenty percent of the total tool price, releasing final payment only after the tool completes a continuous production run of fifty thousand cycles at the target cycle time while holding specified statistical process capabilities.
Whether rheological balance holds across wide resin viscosity shifts remains a key consideration for future tool designs, as bio-based resins and recycled polymers enter precision engineering markets with significant batch-to-batch property variations.