Meaning
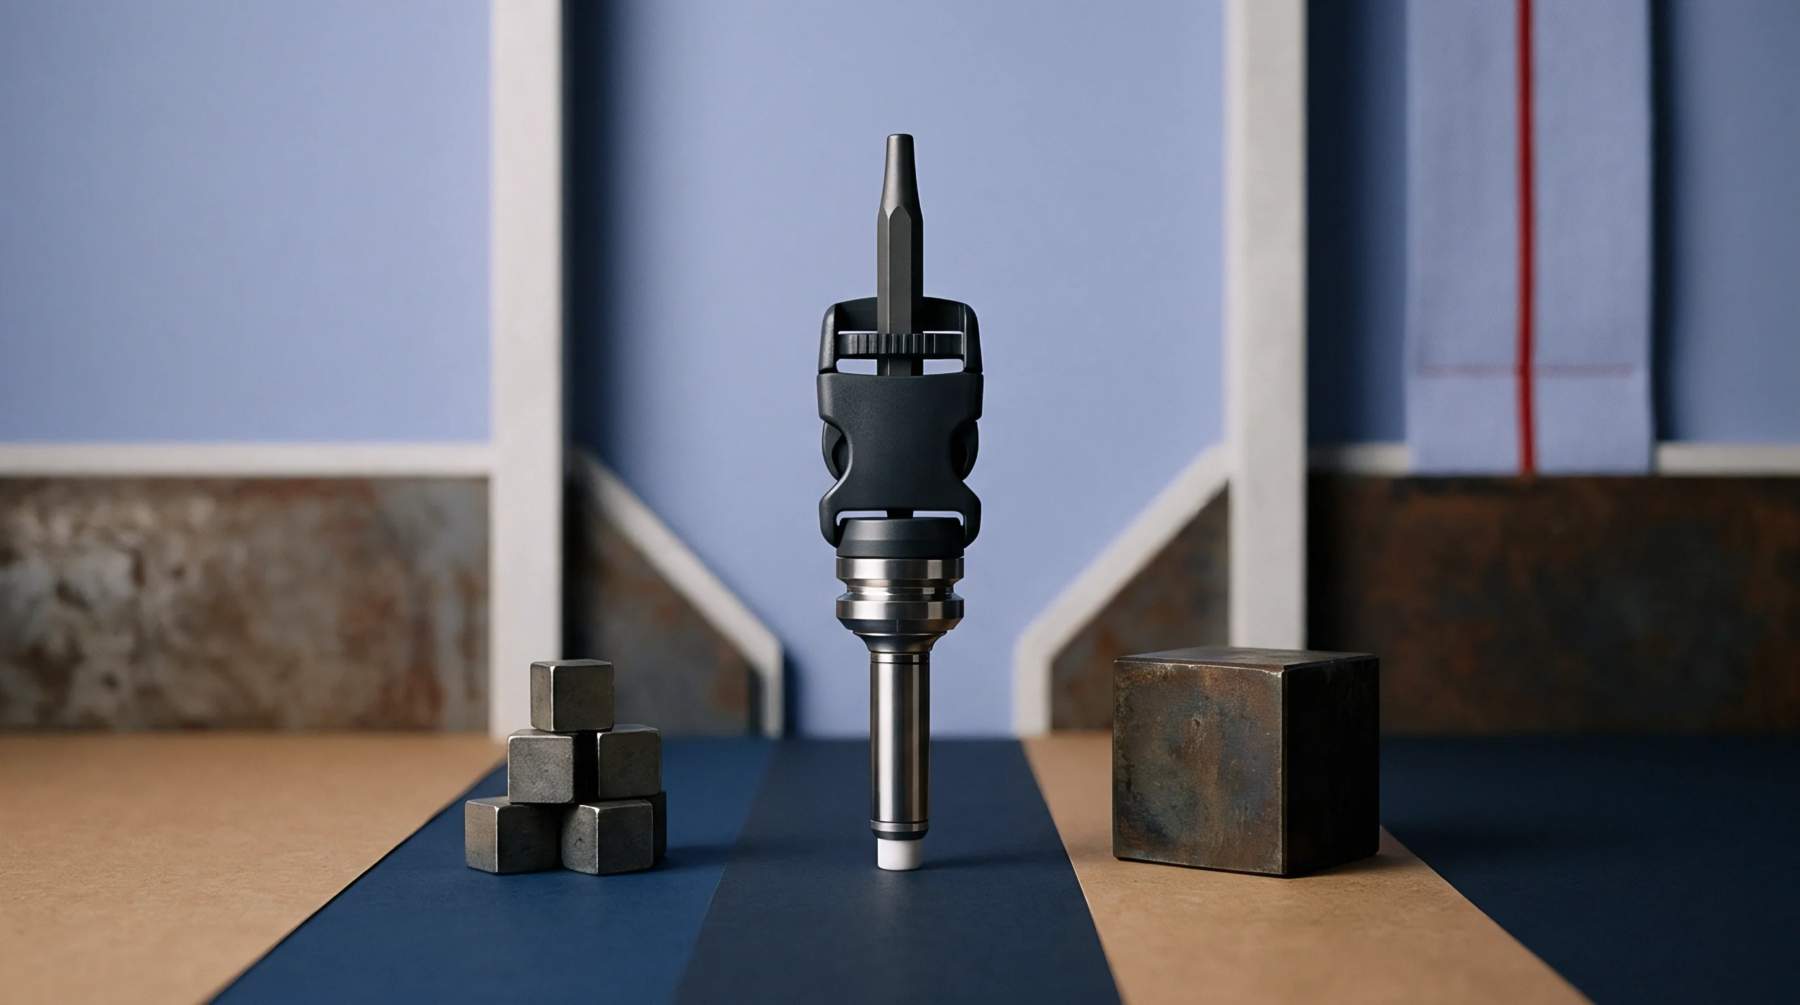
Piezoelectric sensing hardware converts mechanical force from a polymer melt into a proportional electrical signal during the injection moulding cycle. A cavity pressure transducer provides data regarding the internal conditions of a tool during the filling, packing, and holding stages. This sensor detects the actual physical state of the material inside the mould rather than relying on hydraulic line pressure measured at the machine nozzle.
Variations in material viscosity or shot volume alter the output signal, which allows for the identification of short shots or flash conditions during high-speed production.
Process Variable
Maintaining consistent pressure profiles inside the tool ensures stable part weights across extended production runs. A cavity pressure transducer monitors the transition from velocity-controlled filling to pressure-controlled packing. Fluctuations in ambient temperature or batch-to-batch variations in virgin resin density produce distinct signatures in the pressure curve.
Moulders use these signals to trigger the switch from first-stage to second-stage injection, which protects the tooling from over-pressurization. Accurate setpoints prevent the premature degradation of plastic molecules caused by shear stress during the filling phase.
Moulding Economics
Tooling investment includes the integration of sensor ports located at the gate or the end of the flow path. Regrind material exhibits different flow characteristics that force adjustments to the pressure profile compared to virgin resin. Monitoring allows for the automation of part sorting based on valid pressure ranges, which reduces the manual inspection requirement.
High scrap rates frequently occur when the process lacks a feedback loop to reject components formed outside defined pressure limits. This equipment remains a cost-effective method to increase the reliability of production output.
Signal Precision
Calibration of the sensor output against a reference load cell verifies the linearity of the measurement device. Environmental factors such as heat transfer from the heated manifold affect the sensitivity of the internal piezoelectric crystal. Proper installation requires the sensor face to sit flush with the mould cavity surface to prevent localized marking on the finished part.
Surface finish remains constant only when the pressure profile remains stable throughout the cycle. The repeatability of these signals determines the dimensional consistency of the moulded product.