Statistical Process Control Protocol for Injection Mold Parting Line Wear Tracking
Statistical process control tracking of parting line wear prevents mold shutoff hobbing and reduces plastic part flash scrap.
Statistical process control tracking of parting line wear prevents mold shutoff hobbing and reduces plastic part flash scrap.
Predictive thermal resistance modeling balances multi-cavity heat extraction across textured tool inserts to hold tight DIN 16742 tolerances.
Synchronized micro-cavity sensor arrays eliminate undetected fill imbalances and reduce scrap in micro-moulding tools by replacing complex wire harnesses with RF slot waveguides.
Cavity pressure directly controls polyamide crystallization and volumetric shrink, requiring precise transducer monitoring to hold DIN 16742 tolerances.
Managing tool steel modifications during qualification requires steel-safe initial tolerances, controlled additive or subtractive machining, and CAD-matched logging.
Wireless cavity pressure arrays quantify real-time rheological imbalance in multi-cavity molds to optimize tool steel tuning and eliminate scrap.
Match tool steel hardness and chemistry directly to committed shot counts and resin abrasiveness to prevent premature cavity failure and tooling cost overruns.
Packing pressure forces molten polymer into micro-surface roughness features, increasing thermal contact conductance up to ten-fold until solidification gap detachment occurs.
Volumetric areal parameters predict gate wear before profile roughness detects steel loss, preventing tool failure in glass-filled polymer injection molding.
Precision cavity pressure sensor selection demands matching load path dynamics with piezoelectric drift limits and verified in-situ dynamic calibration routines.
Selecting areal surface texture filter cutoffs under ISO 25178 matches transmission bandwidth to moulding replication limits, preventing false tooling rejects.
Controlled steel modifications require process window locking, metal-safe geometry audits, and metallurgical stress relief before qualified production release.
Dynamic sensor drift in high-temperature tooling stems from insulation drop and thermal charge loss; manage via matched crystals, cabling, and reset timing.
Recutting tool steel establishes a stable process window that lowers long-term scrap costs and cycle times compared to forced parameter tuning.
Optimal cavitation balances machine hourly rates, clamp tonnage, and shot capacity against thermal cooling limits and cross-cavity dimensional distribution.
In situ optical profilometry resolves sub-micron cavity wear in narrow tool ribs using fiber-coupled chromatic sensors sealed behind purged sapphire windows.
Calculated thermal expansion along tool plates dictates guide pin clearances and shut-height clamp adjustments required to prevent parting line damage.
Machining sensor bores to strict concentricity tolerances and establishing direct picoCoulomb calibration scales cavity pressure for closed-loop process control.
Coupled viscoplastic modeling of back-stress hardening and adiabatic softening allows thin-wall tooling optimization that cuts cycle times and capital spend.
Turbulent flow inside conformal cooling circuits requires managing additive channel roughness and diameter to prevent pump choking and inflated cycle times.
Injection mold land recession requires SPC tracking of shut-off steps to schedule laser micro-welding before parting line wear causes flash.
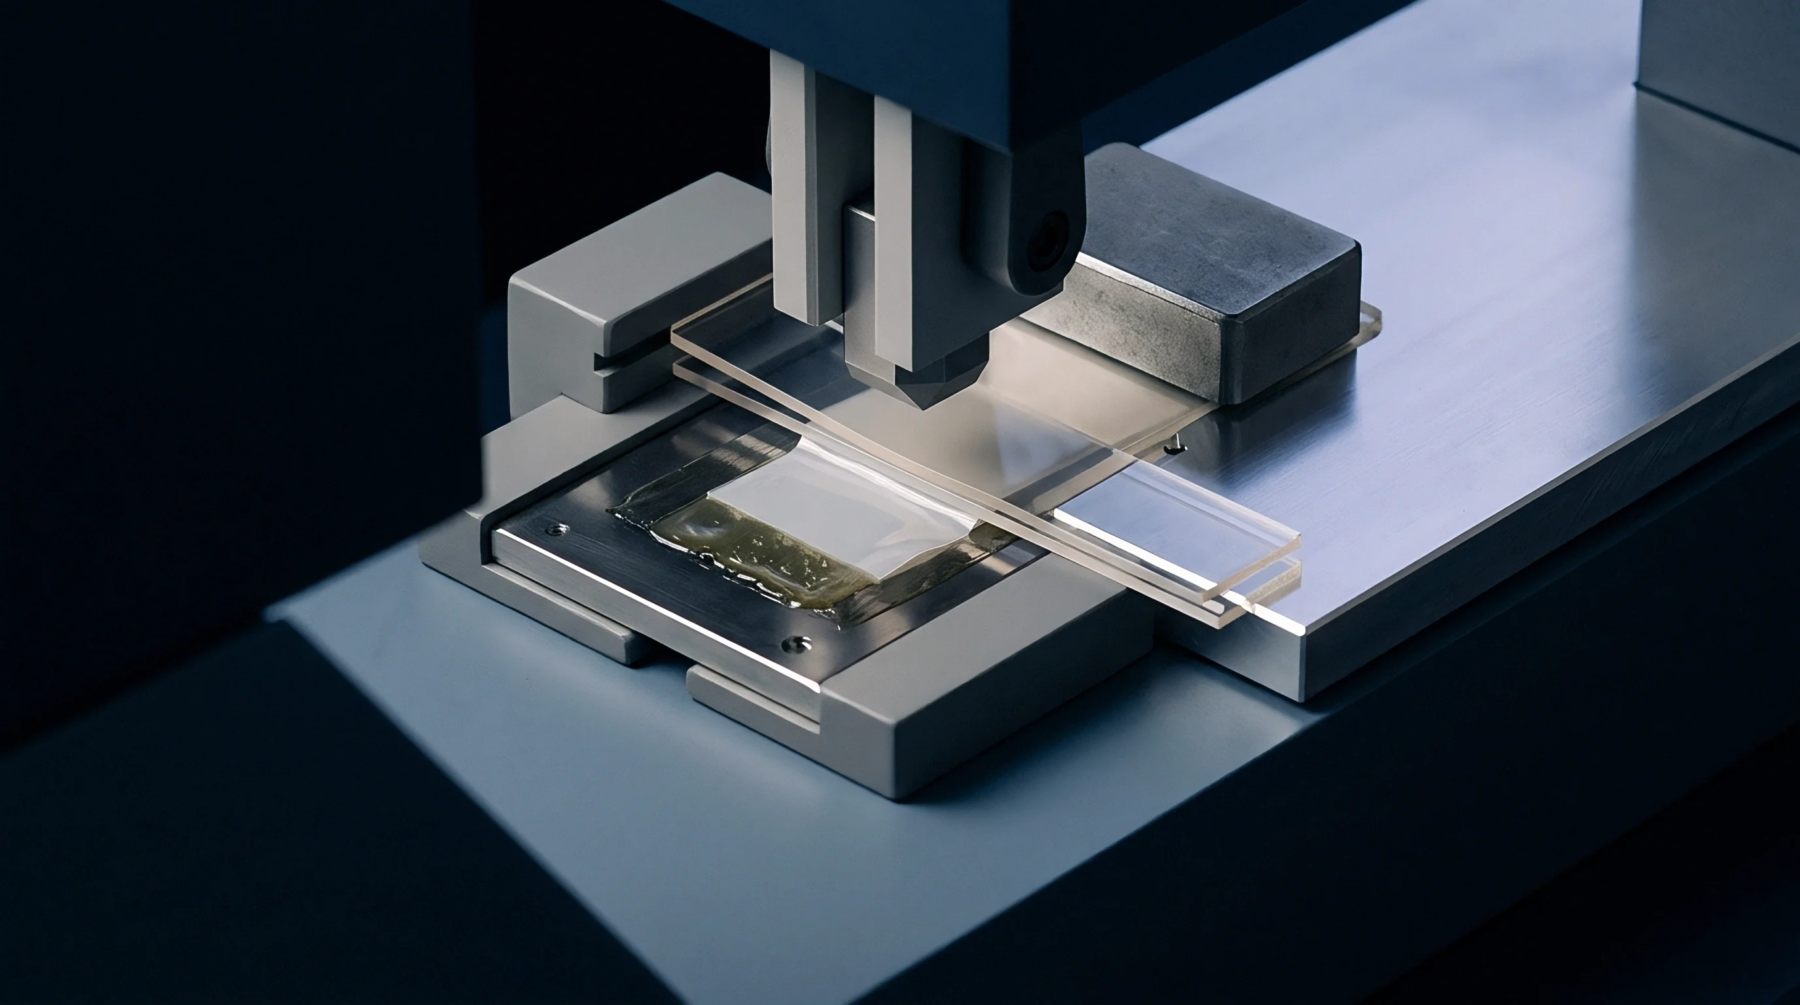
Non-linear degradation modeling protects coated carbide shutoff lands by predicting exponential wear acceleration from volatile chemical binder leaching.
Melt flow length scales with cavity thickness raised to the third power while cycle time increases quadratically, forcing tight nominal wall control.
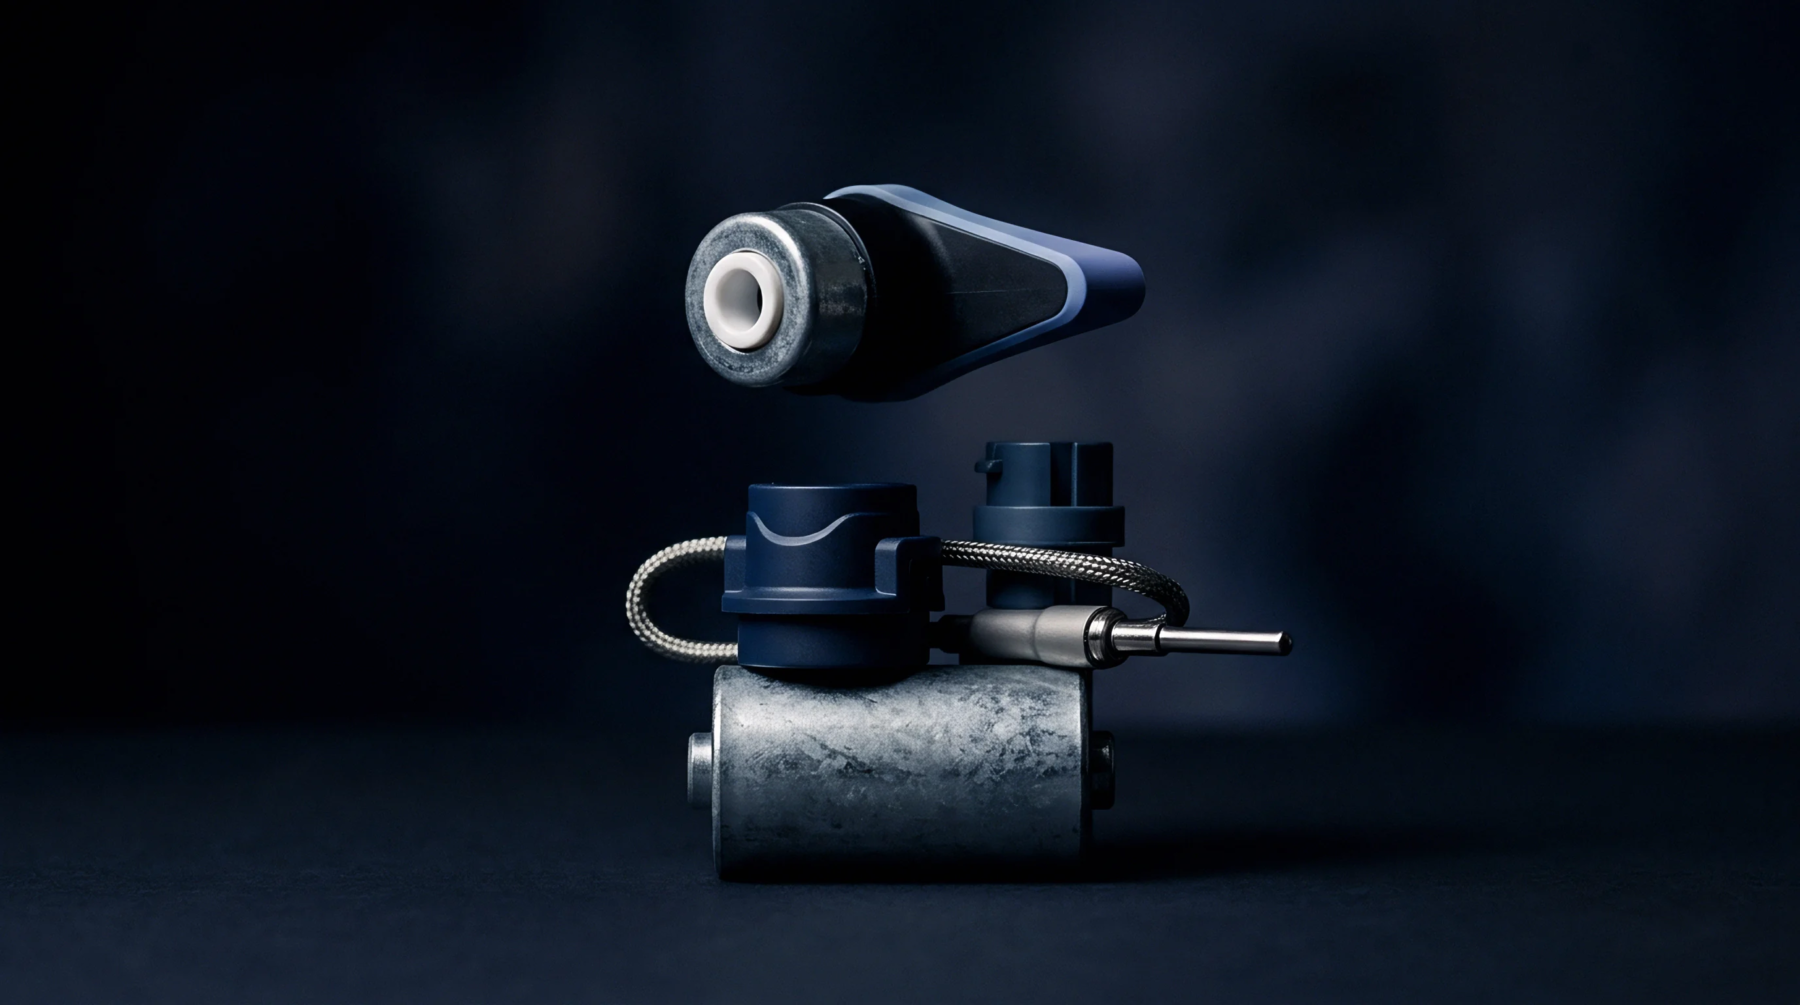
Trans-steel sensor arrays require dielectric waveguides or acoustic paths to bypass extreme RF loss, maintaining a 15 dB link margin under full clamp tonnage.
Verify shutoff lands by balancing land contact area to machine tonnage and confirming 85 percent contact via pressure film and hot-mold wire crush testing.
Map injection moulding flow tensors into Abaqus using Hill plasticity to resolve polypropylene anisotropy and prevent premature structural failure.
Integrating piezoelectric sensors into high cavitation micro tools requires precise pocket fits, shielded wiring, and 10 kHz logging to balance filling across pins.
Dynamic cavity pressure integration enables real-time verification of part density and triggers millisecond-response scrap gates before mould opening.
Plate deflection must remain under resin flash limits (typically 0.02 mm) by sizing plate thickness to the third power and preloading center support pillars.
Coupled thermo-mechanical plate deformation dictates parting breathing and cavity flash, requiring pre-loaded support columns and strict deflection limits.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.