Tool Steel Modification Mechanics for Precision Injection Tooling
Precision tool steel modifications succeed by controlling thermal gradients during deposition and EDM to eliminate brittle white layers and residual stresses.
Precision tool steel modifications succeed by controlling thermal gradients during deposition and EDM to eliminate brittle white layers and residual stresses.

Post-weld heat treatment at 550°C for two hours per inch relieves 85% of peak residual stresses, preventing mandrel cracking and parting line flash.
Mitigate core thermal fatigue by preheating substrates above 280°C, selecting maraging filler wires, and double tempering to eliminate tensile residual stress.
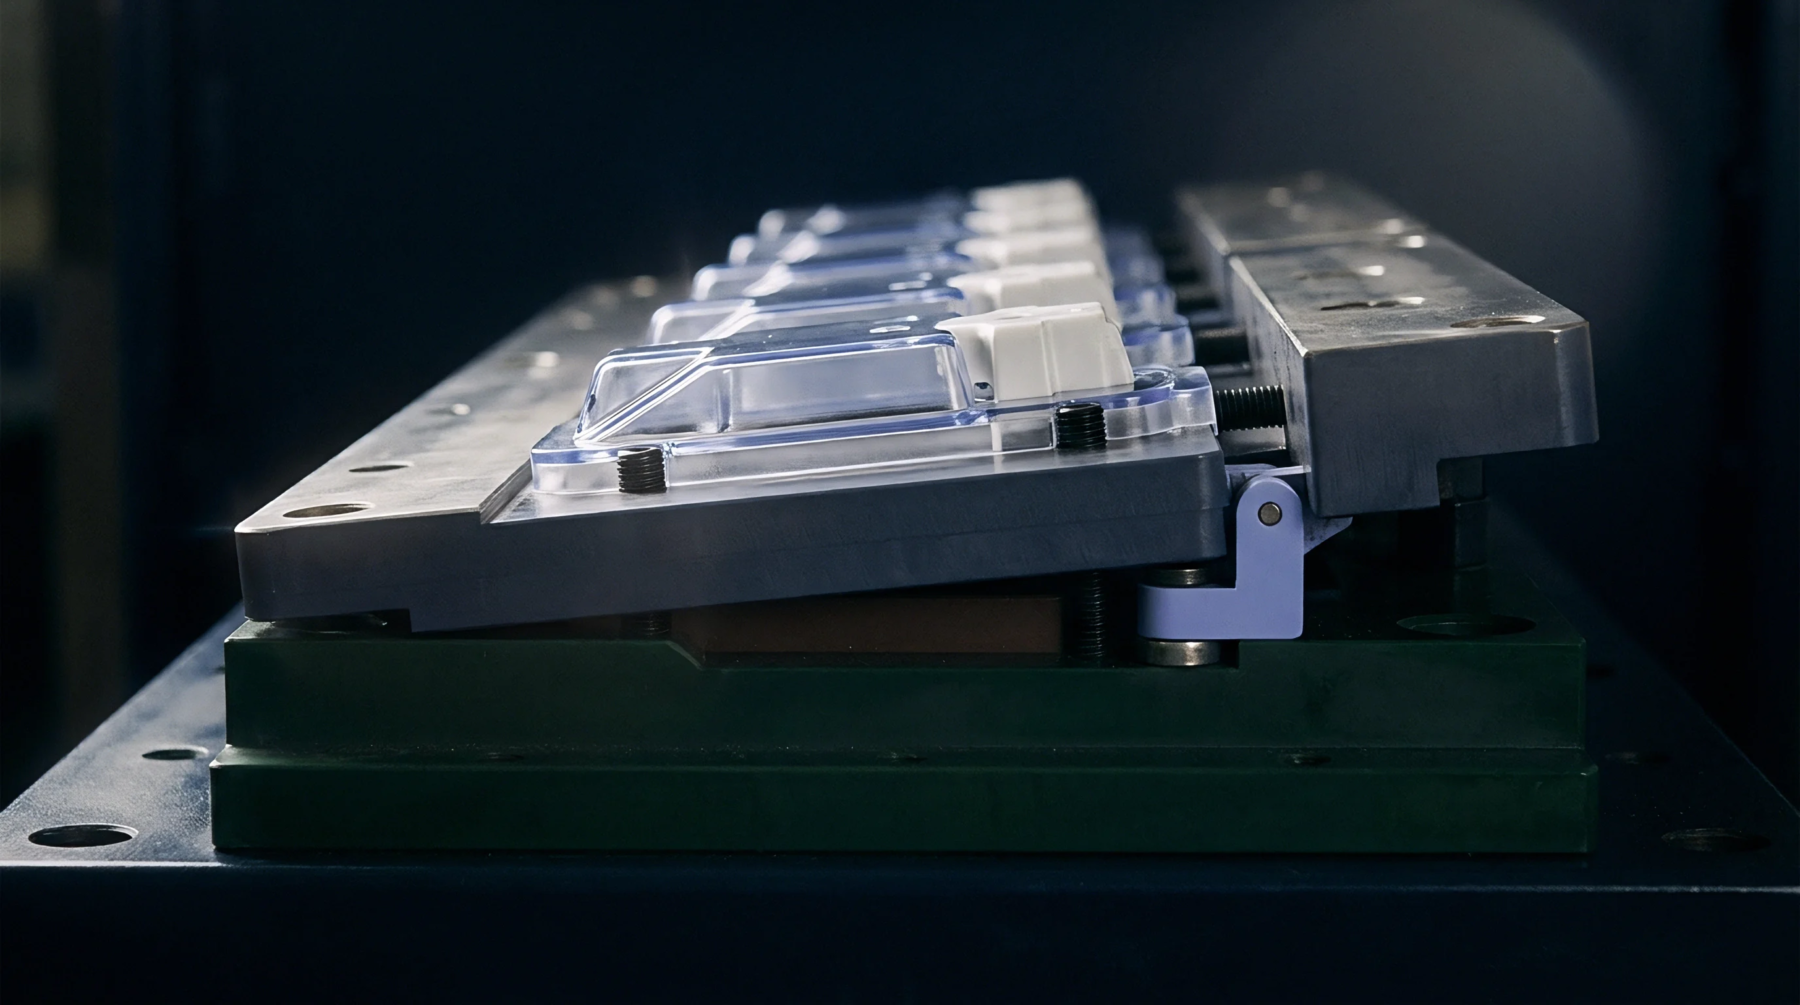
Injection mold land recession requires SPC tracking of shut-off steps to schedule laser micro-welding before parting line wear causes flash.
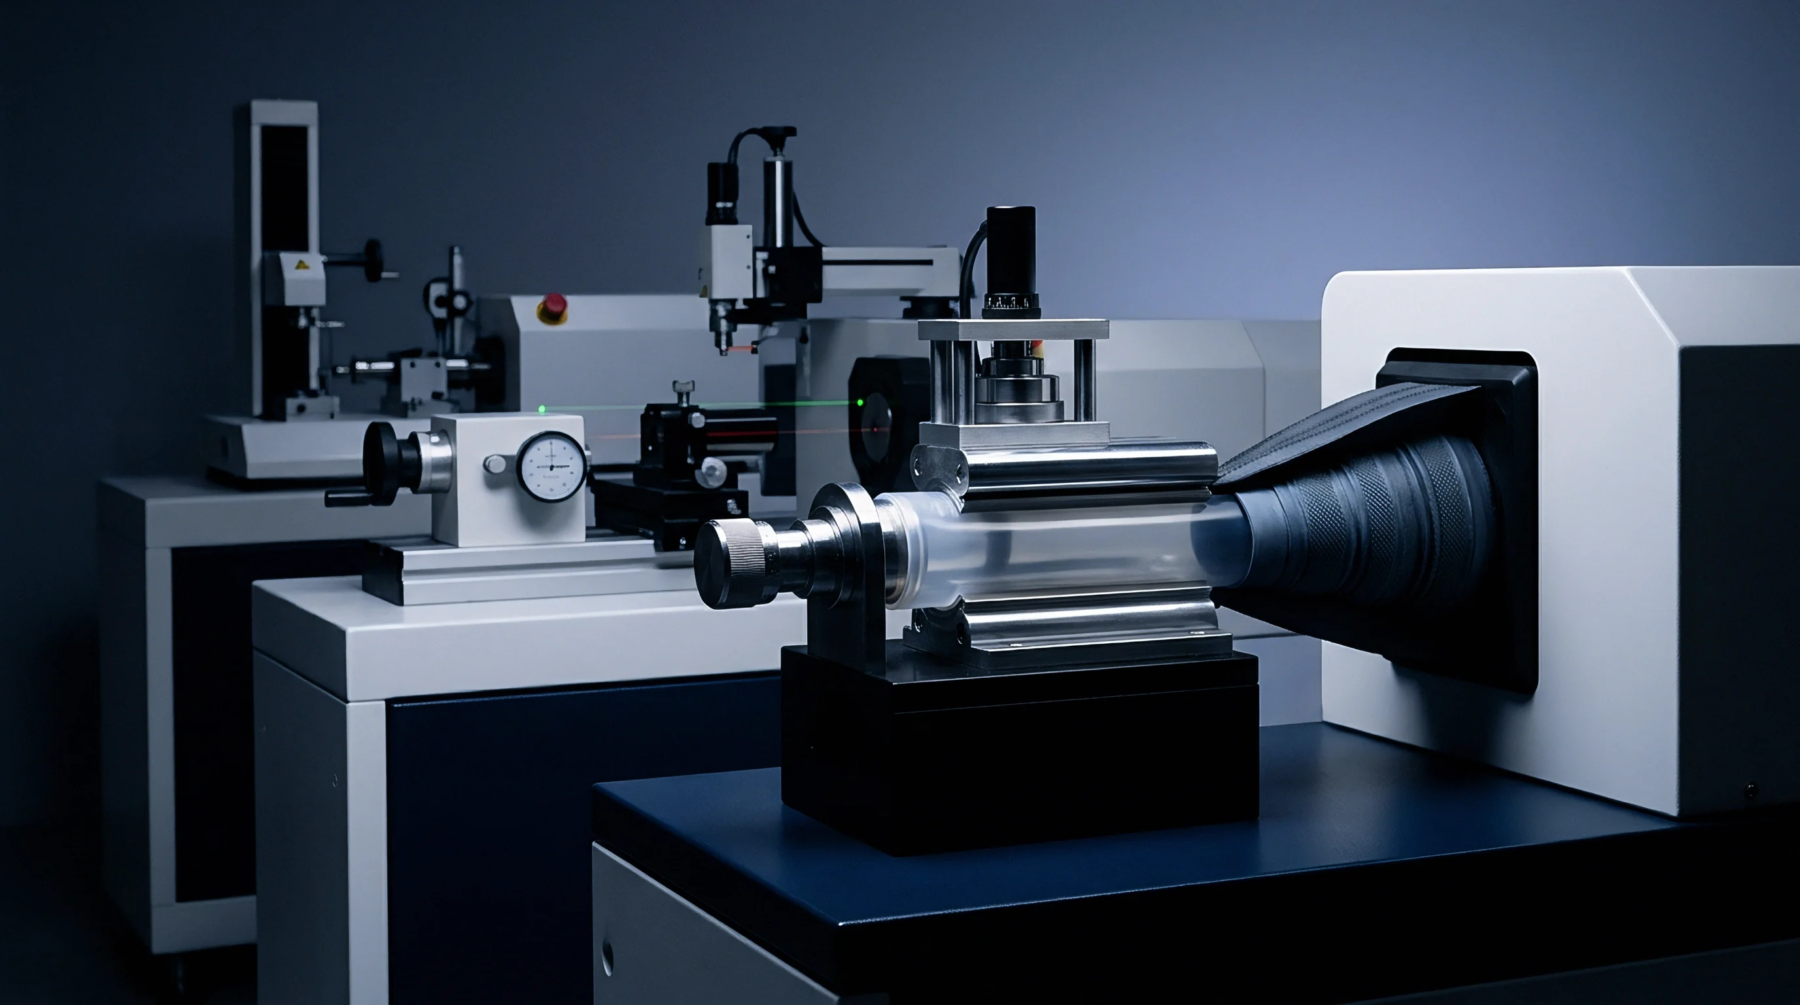
Controlled steel modifications require process window locking, metal-safe geometry audits, and metallurgical stress relief before qualified production release.
Managing tool steel modifications during qualification requires steel-safe initial tolerances, controlled additive or subtractive machining, and CAD-matched logging.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.