Meaning
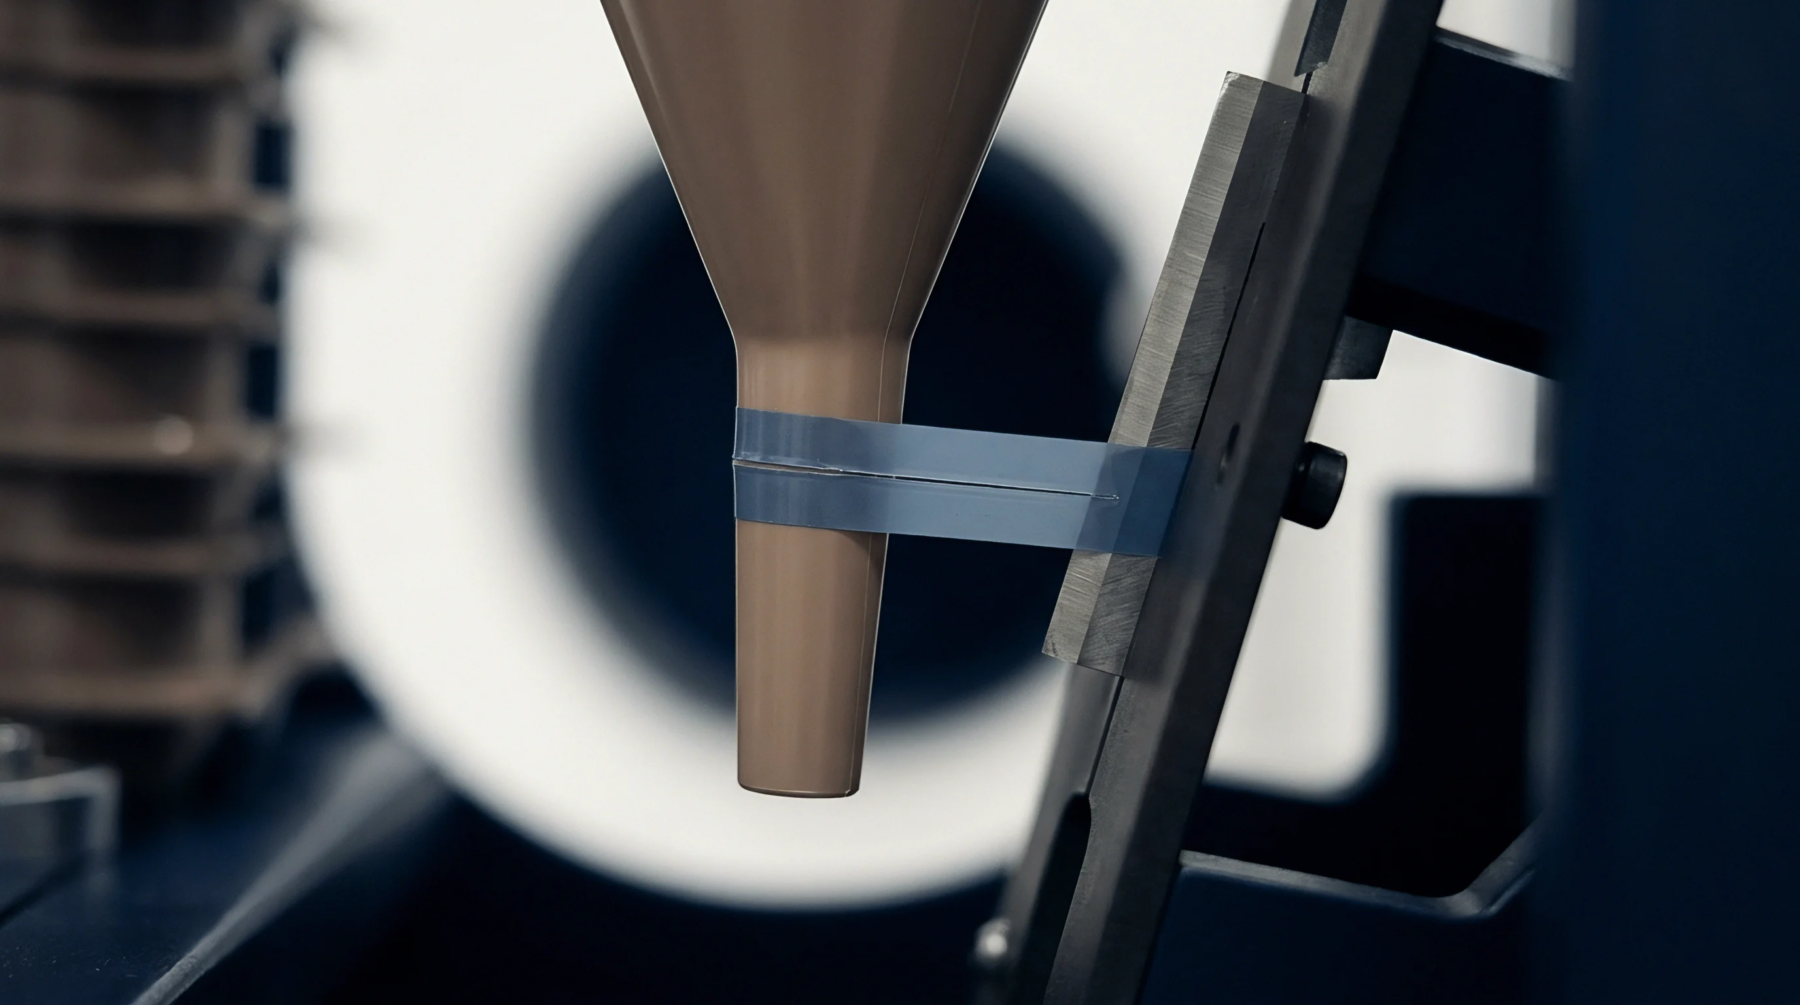
The standardized testing protocol known technically as ASTM D1238 governs melt flow rate measurements for thermoplastic polymers by forcing molten resin through a calibrated die under a specified piston load and temperature. Practitioners employ this standardized method to quantify how easily a given polymer flows during commercial processing stages like injection moulding or film extrusion. Testing procedures require operators to load polymer pellets into a heated metallic cylinder, apply a dead weight onto the internal piston, and collect extrudate over timed intervals to determine mass flow rates.
Below specified molecular weight thresholds and outside established shear rate parameters, melt flow index values fail to correlate with actual processing behavior, rendering the standard inapplicable for thermosets or heavily filled compounds.
Thermal Viscosity
Melt flow determinations establish the baseline molecular weight distribution of incoming polymer stocks before technicians clear resins for production floors. Thermal degradation occurs inside barrels when barrel heaters run too hot, causing polymer chains to break down and yield artificially elevated melt index numbers. Production schedules depend on consistent resin viscosity because shifting melt rates alter cavity filling dynamics, resulting in short shots or flash defects on finished mouldings.
Virgin raw materials typically exhibit tightly controlled melt flow ranges from resin manufacturers, whereas post-consumer regrind batches introduce variable viscosity levels that disrupt steady state machine cycles.
Processing Dynamics
Injection moulding presses require stable polymer fluidity to maintain uniform packing pressures during part formation. Higher piston weights on plastometers simulate the high shear rates experienced by resins moving through runner systems and gating orifices during fast injection cycles. Temperature fluctuations inside the barrel alter polymer density, causing the extruded mass to deviate from acceptable commercial tolerances established in material purchase specifications.
Moulders adjust holding pressures and cooling timers to compensate for minor batch variations, but severe viscosity swings demand complete machine recalibration to prevent dimensional warping in moulded components.
Economic Tolerance
Material specifications define allowable melt index bands for incoming resin shipments, whereas part specifications dictate structural performance requirements for end-use plastic components. Purchasing agents negotiate resin pricing based on melt flow consistency, knowing that off-grade batches increase scrap rates and extend cycle times during production runs. Quality control laboratories measure melt mass flow rates on every truckload of pellets to verify supplier compliance before raw materials enter plant silos.
Melt flow testing ultimately provides the financial buffer that prevents out-of-specification polymers from entering costly manufacturing operations.