Injection Mould Wall Thickness Design Rules and Flow Ratios
Melt flow length scales with cavity thickness raised to the third power while cycle time increases quadratically, forcing tight nominal wall control.
Melt flow length scales with cavity thickness raised to the third power while cycle time increases quadratically, forcing tight nominal wall control.
Standard single-load melt index tests mischaracterize high molecular weight polyethylene by ignoring shear thinning, requiring multi-load flow ratio verification.
Intrinsic viscosity loss in reprocessed PET flake is quantified by dilute solution viscometry using ASTM D4603 to prevent structural failure in preforms.
Polyethylene terephthalate trace moisture determination relies on Karl Fischer coulometric oven extraction at 170 to 180 degrees Celsius to prevent chain scission.
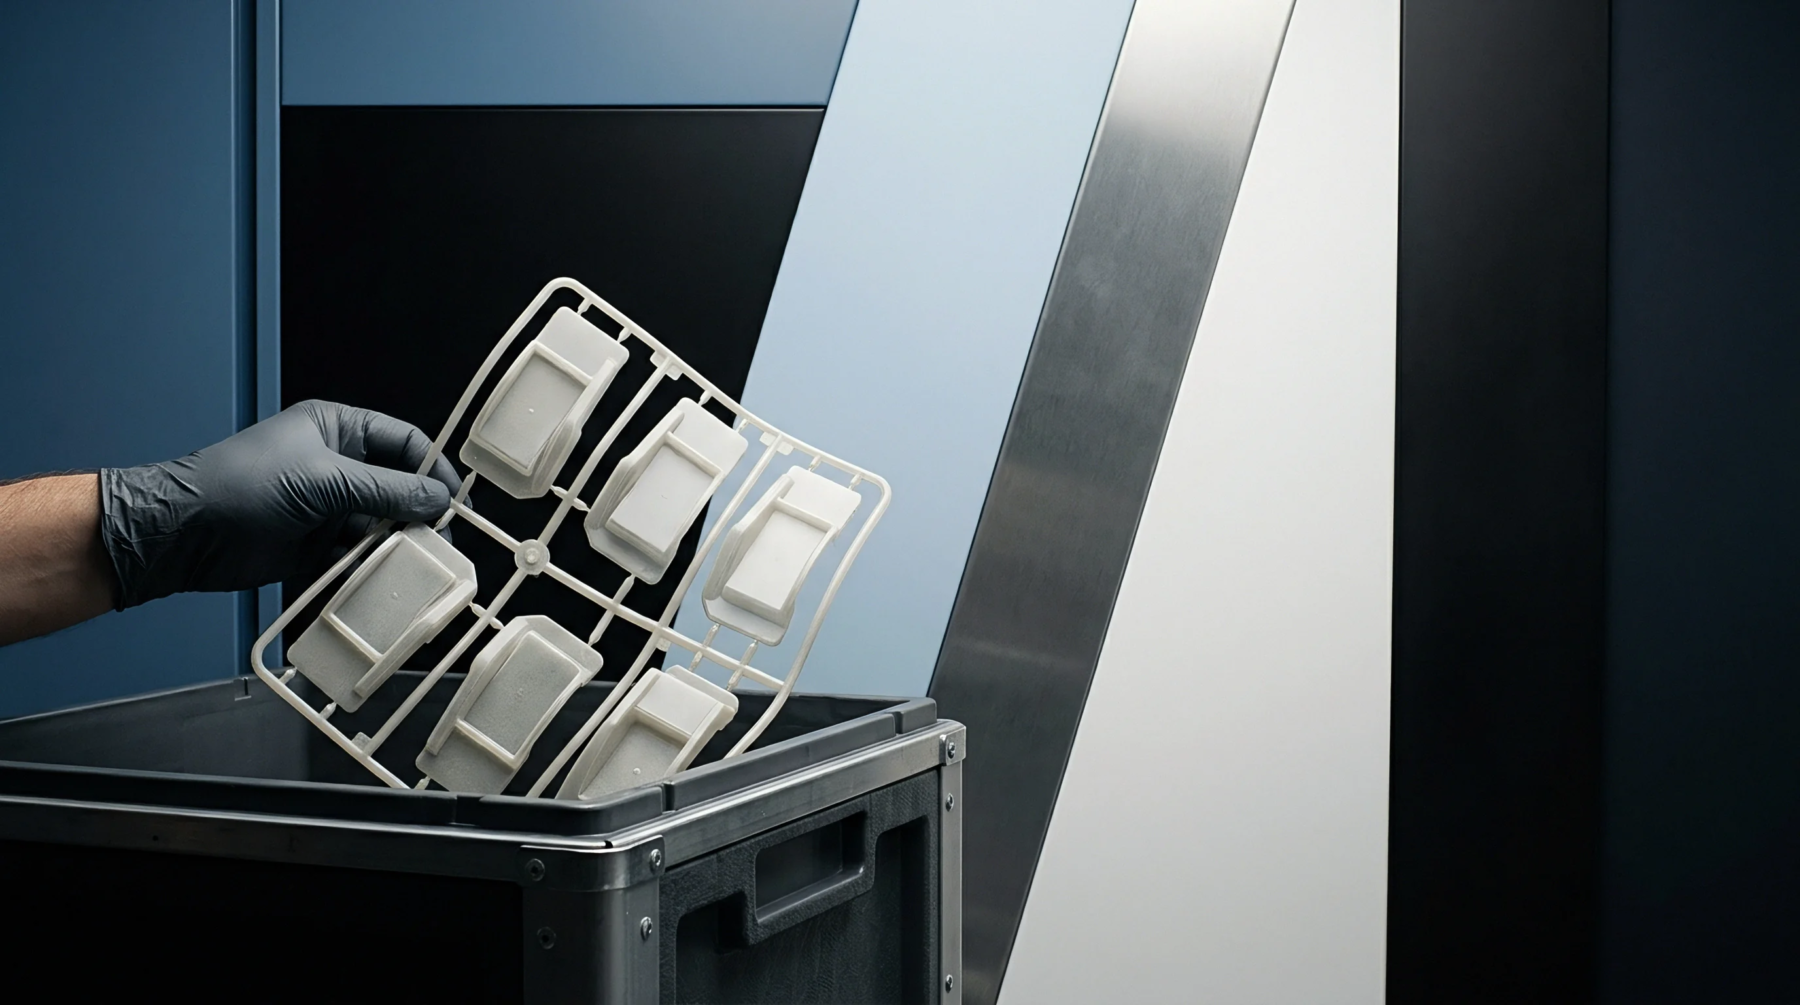
Packing pressure forces molten polymer into micro-surface roughness features, increasing thermal contact conductance up to ten-fold until solidification gap detachment occurs.
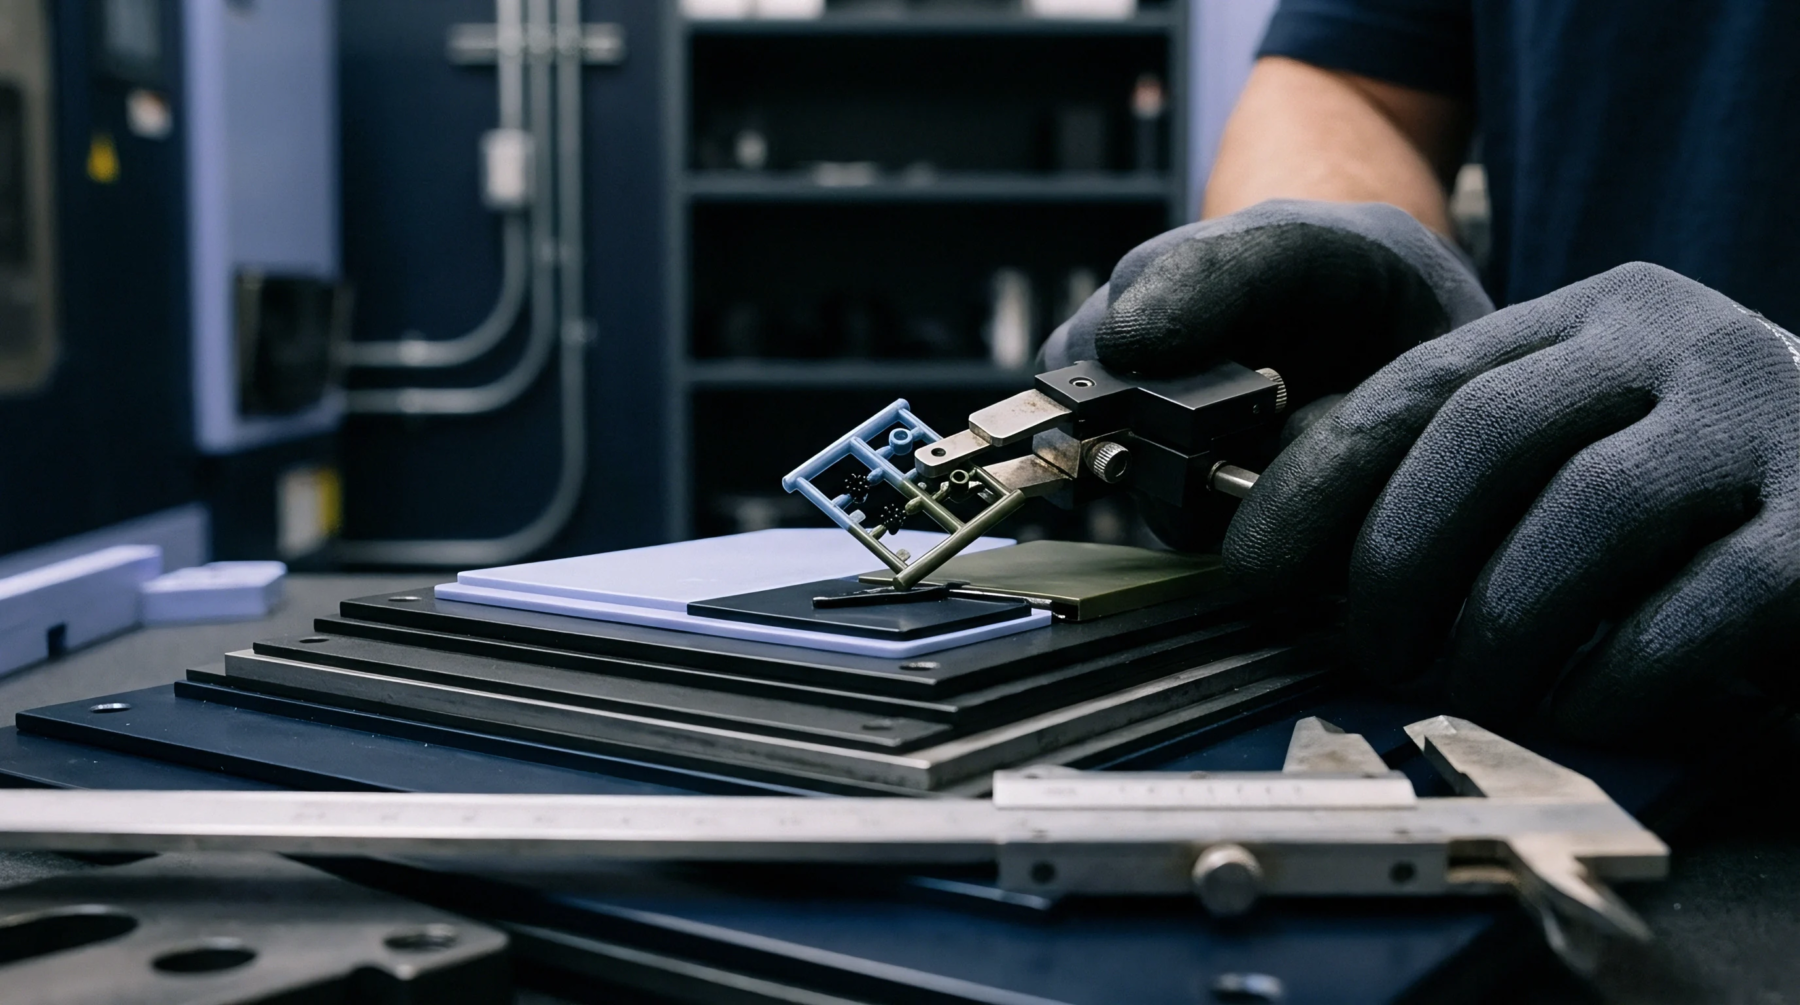
Cavity pressure measurement in micro-injection tooling decouples machine dynamics from cavity fill, eliminating part weight variance and micro-defects.
Uniform wall thickness design balances polymer flow, prevents shrink defects, cuts cycle times, and reduces landed part cost in injection moulding tools.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.