Meaning
Regulatory verification of chemical migration limits defines food contact compliance across polymer sourcing and moulding. Resins face strict migration thresholds when packaging fatty or acidic goods, and food contact compliance sets the allowable parts per billion of monomers entering consumable substances. Extrusion and injection operations must maintain precise melt temperatures to prevent thermal degradation from generating unauthorised oligomers.
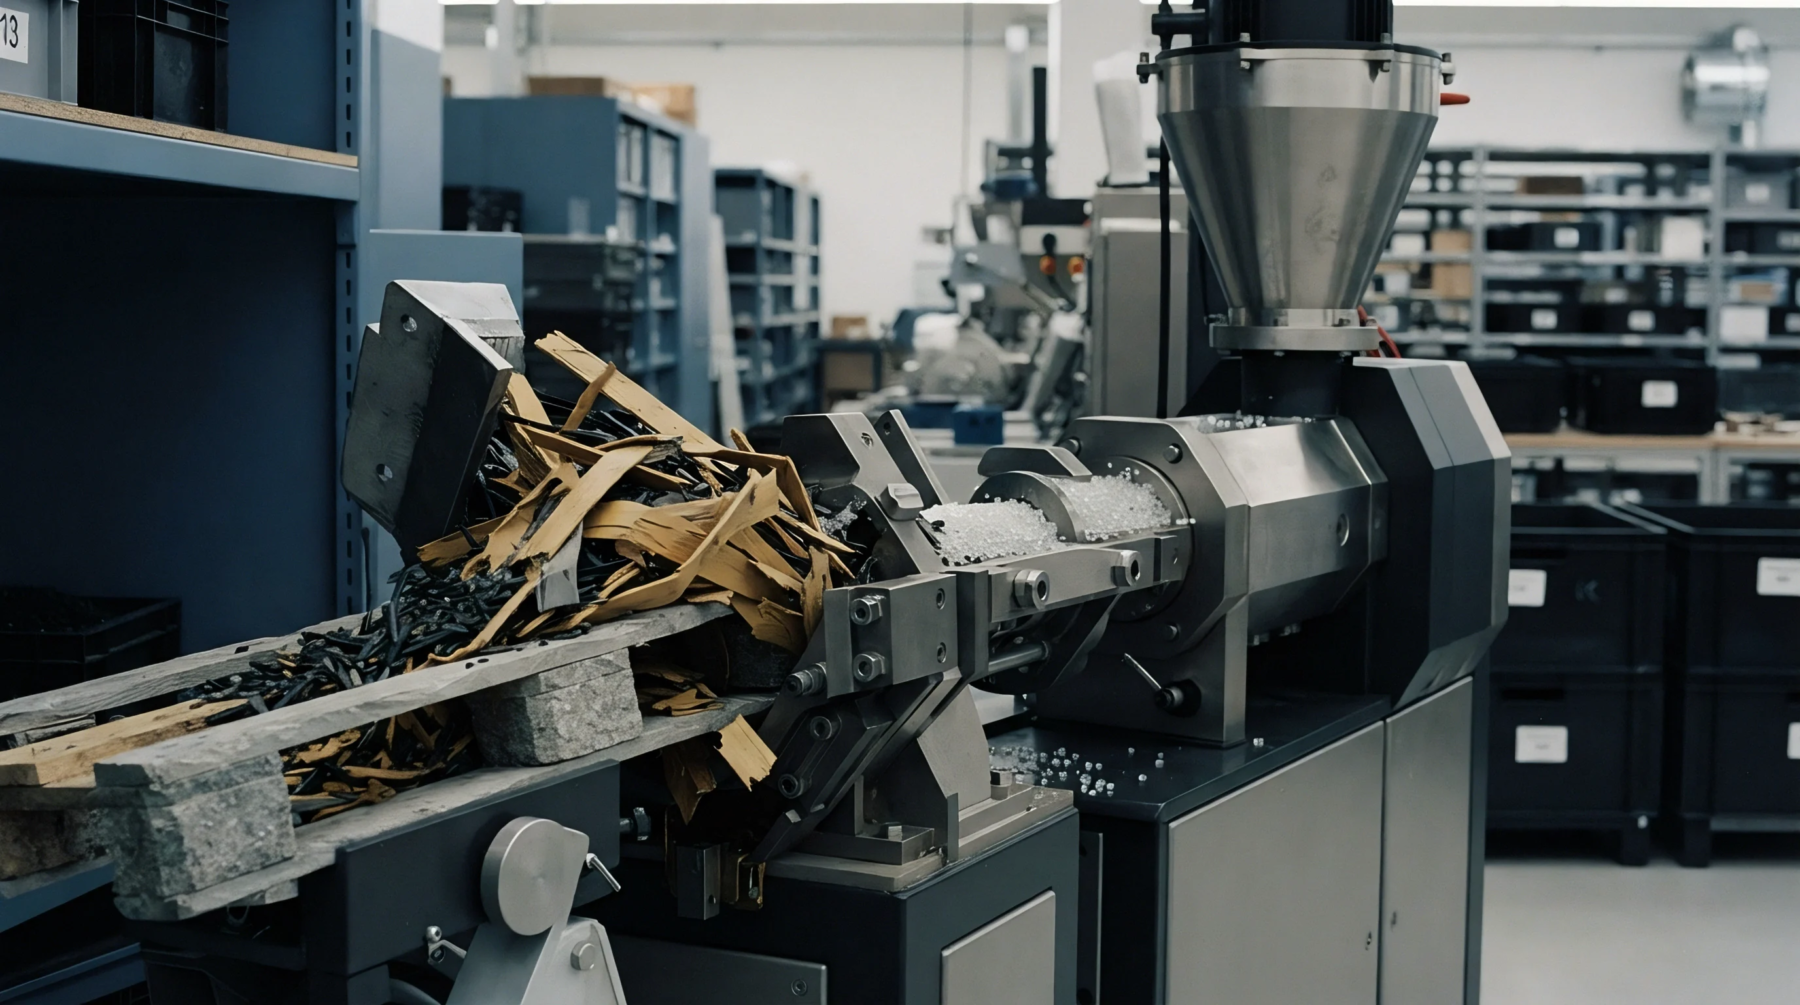
Unchecked barrel overheating generates degradation products that fail migration testing and force costly lot rejections. Virgin polymer stocks offer predictable additive packages and clean documentation chains. Regrind incorporation introduces thermal history and unknown stabilizers, which complicate migration profiles.
Processors balance resin cost reductions against the higher analytical testing expenses demanded by recycled content.
Resin Migration Thresholds
Analytical laboratories quantify extractable fractions by exposing polymer test plaques to food simulants under elevated temperatures. Molecular weight distribution dictates how readily low molecular weight fractions leach through the barrier. Resins with broad distributions carry higher risks of exceeding legal migration limits.
Moulding pressures alter part density and crystalline structure, which subsequently changes diffusion pathways for residual chemical species. Parts with high crystallinity restrict molecular mobility and reduce chemical transfer to packaged goods. Datasheet values report raw pellet properties rather than moulded article performance.
Moulders must validate final parts because cooling rates inside the tool alter crystalline growth and migration potential.
Additive Migration Risk
Polymer formulations rely on slip agents, plasticizers, and antioxidants to survive high shear forces during processing. These functional additives migrate toward the surface of moulded parts over time, particularly under thermal stress. Unbound molecules near the boundary layer transfer rapidly into packaged contents during storage.
Tooling designers select surface finishes that minimize contact area without trapping chemical residues from mould release agents. Residual cleaning agents left in barrel cavities contaminate subsequent production runs and cause unexpected analytical failures. Strict quality control protocols require resin suppliers to provide detailed migration declarations for every masterbatch formulation.
Blending virgin feedstock with post-consumer regrind introduces unverified contaminants that bypass standard certificate verification checks.
Thermal Degradation Control
Barrel residence time directly influences polymer stability and molecular chain scission during plastication. Excessive heat history breaks polymer backbones into smaller, more mobile fractions that readily migrate into food simulants. Operators monitor screw speed and back pressure to prevent localized overheating caused by excessive mechanical shear.
Automated temperature controllers maintain tight thermal zones along the barrel to protect polymer integrity throughout production. Finished parts retain internal stresses when cooling occurs too rapidly inside complex tooling geometries. Annealing processes relieve residual stresses but add manufacturing steps and increase overall component costs.
Chemical migration testing ensures moulded packaging maintains consumer safety across extended shelf life durations.