Meaning
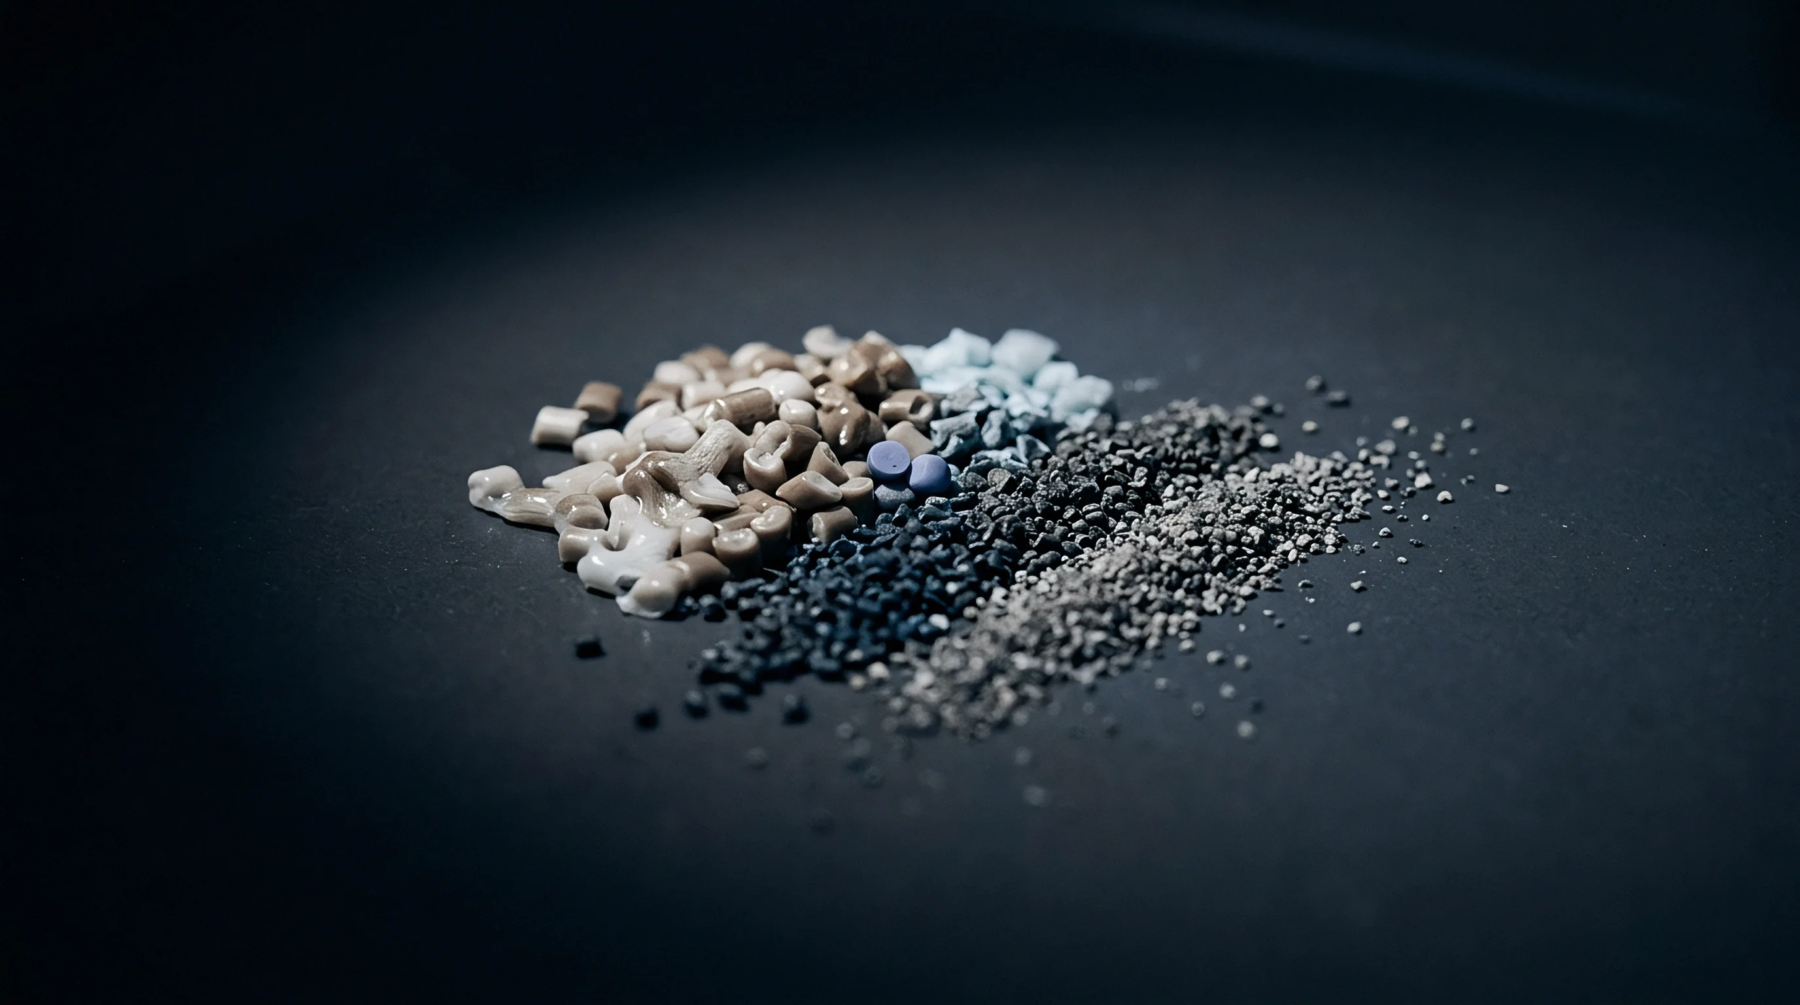
Reclaimed polymer feedstock derived from post-consumer or post-industrial waste streams forms recycled polypropylene when pelletised for subsequent thermal processing. Industrial buyers specify this secondary resin by melt flow index, contaminant tolerance, and lot consistency rather than pristine origin. Strict adherence to property boundaries prevents processing failures, because inconsistent rheological behaviour creates severe warp in finished mouldings.
Virgin material commands a pricing premium based on predictable additive packages and low volatile content. Regrind fractions introduce variability that challenges standard cycle times and mould filling dynamics. Operators must adjust barrel temperatures and injection pressures constantly to compensate for batch-to-batch viscosity shifts.
Datasheet values published by compounders rarely match the processing window observed on shop floors due to thermal degradation history.
Thermal Degradation
Polymer chains experience chain scission and cross-linking during initial moulding lives, which alters molecular weight distribution permanently. Recycled polypropylene suffers from reduced impact strength and lower elongation at break compared to virgin polymer. Extrusion lines run at lower melt temperatures to prevent further thermal breakdown during secondary pelletisation.
Shear history dictates final mechanical performance, meaning parts molded from high-shear scrap exhibit brittle failure modes. Additive packages must replenish depleted stabilisers to restore thermal resistance before commercial sale. Processors test incoming lots for melt flow rate anomalies that signal severe molecular degradation from previous thermal cycles.
Contaminant Tolerance
Extraneous polymers and non-melting particles present in waste streams create surface blemishes and structural weak points. Sorters remove incompatible plastics using near-infrared detection technology prior to melt filtration stages. Melt filters capture degraded gels and solid particulates down to micron levels during compounding extrusion.
Inadequate filtration leads to gate blockages in multi-cavity injection molds and causes catastrophic part rejection. Cross-contamination with polyethylene reduces stiffness and lowers the heat deflection temperature of molded components significantly. Quality control protocols rely on ash content testing to quantify mineral fillers and residual dirt within the resin.
Economic Yield
Sourcing secondary polymers reduces raw material expenditure while introducing higher scrap rates during part production. Moulders balance lower purchase costs against extended cycle tuning times and increased machine downtime. Part specifications dictate whether regrind percentages compromise structural integrity in load-bearing applications.
Regulatory pressures compel brand owners to incorporate post-consumer content despite processing inconsistencies and supply chain volatility. Tooling modifications compensate for shrinkage variations observed when switching between virgin and secondary grades. Commercial viability depends entirely on maintaining stable output quality across fluctuating feedstock batches.