Closed-Loop Cavity Pressure Control Implementation in Micro-Injection Moulding
Closed-loop cavity pressure control stabilizes micro-injection molding by compensating for viscosity shifts and holding part dimensions within micron tolerances.
Closed-loop cavity pressure control stabilizes micro-injection molding by compensating for viscosity shifts and holding part dimensions within micron tolerances.
Coupling cavity pressure telemetry directly to machine velocity switchover eliminates part weight variance caused by melt viscosity shifts across production runs.
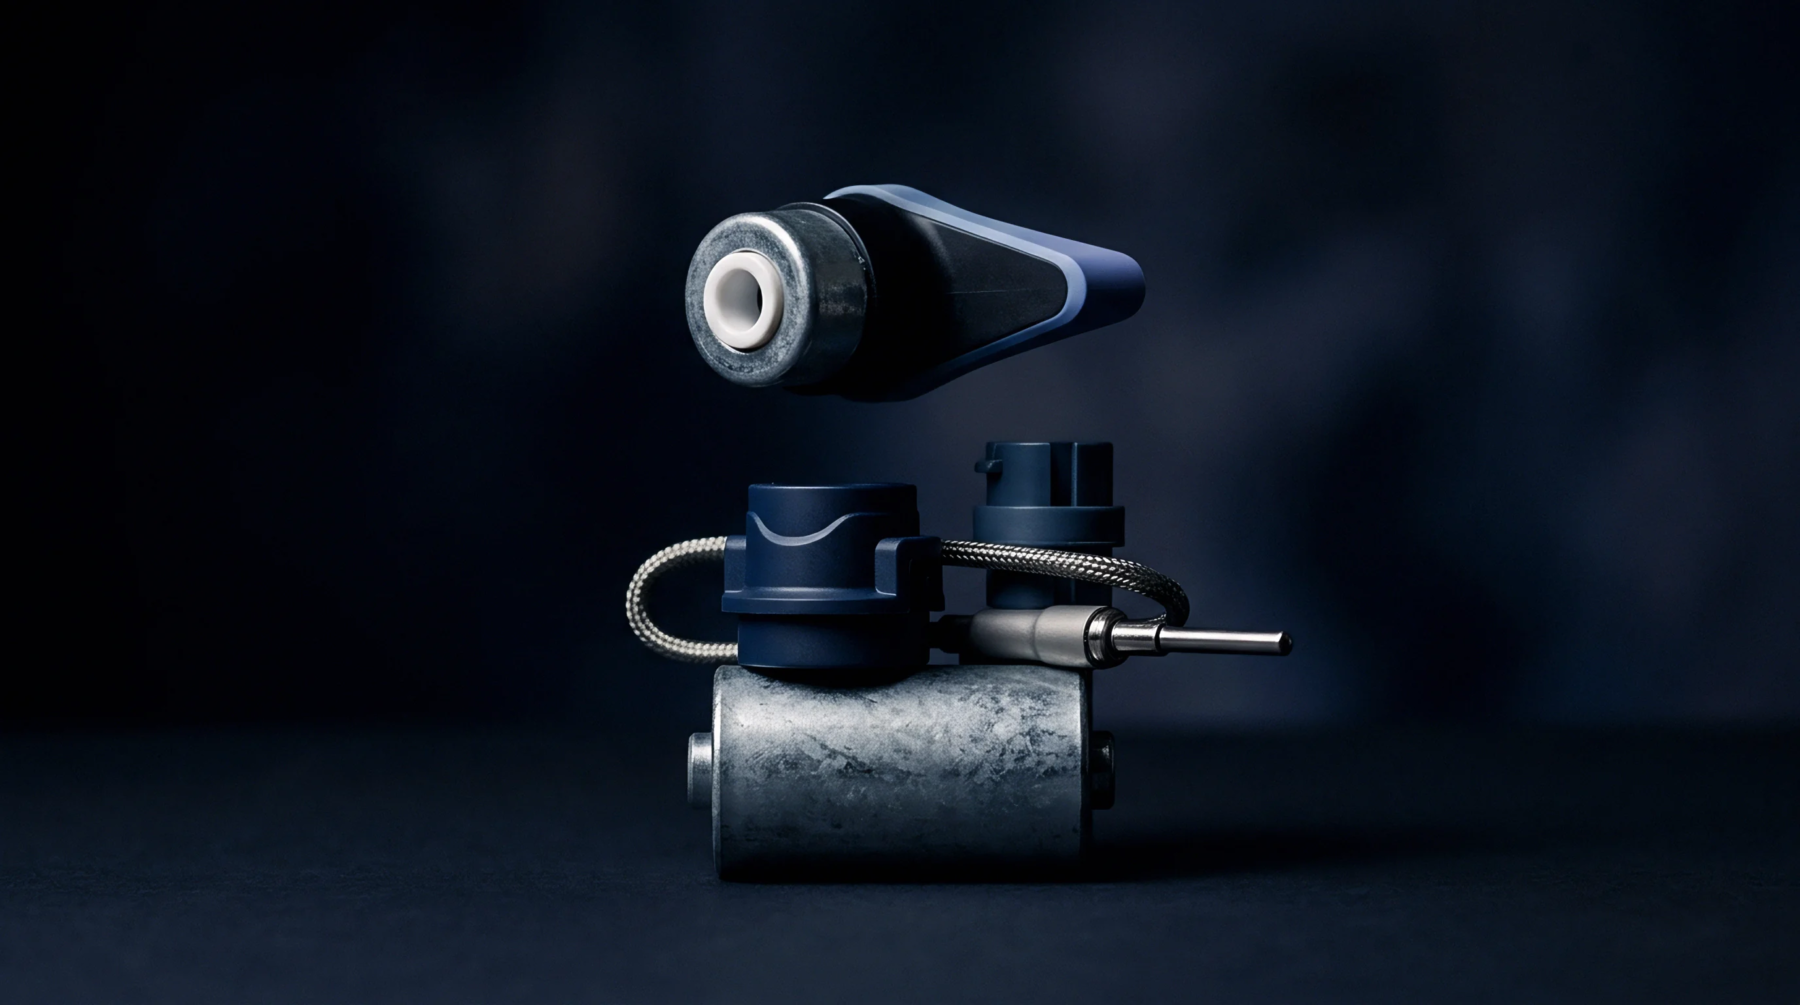
Cavity sensor integration requires rigid pocket machining, protected wire routing, and direct melt placement to decouple press dynamics from part tolerance.
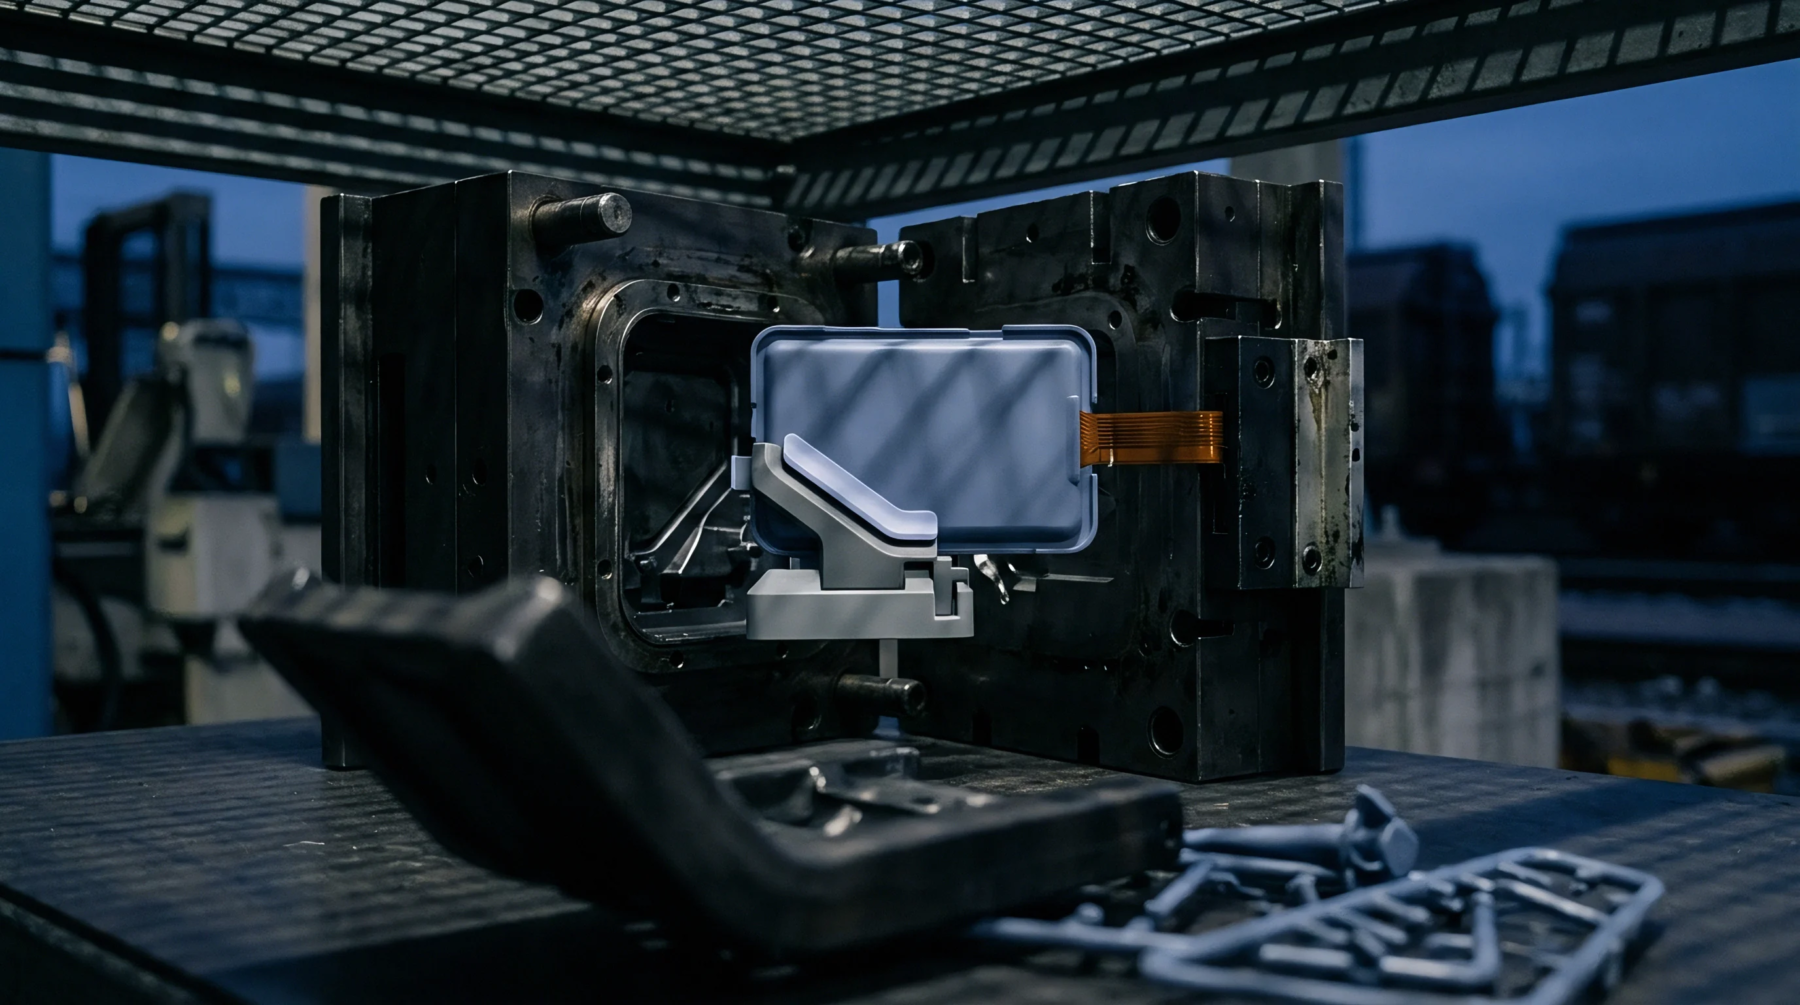
Inter-cavity thermal drift in high-cavitation steel tooling shifts part dimensions; turbulent coolant flow and conductive inserts eliminate temperature spreads.
Sub-micron micro molding tooling requires preloaded rolling alignment, rigid pocket seating, and tight thermal regulation to hold sub-five-micrometer part tolerances.
Cavity pressure measurement in micro-injection tooling decouples machine dynamics from cavity fill, eliminating part weight variance and micro-defects.
Real-time digital thermal drift compensation combined with diamond-like carbon coated pins eliminates signal hysteresis in sub-millimetre cavity sensors.
Real-time mold cavity pressure telemetry triggers automated mechanical part rejection, ensuring sub-gram defective melt profiles never enter production inventory.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.