Meaning
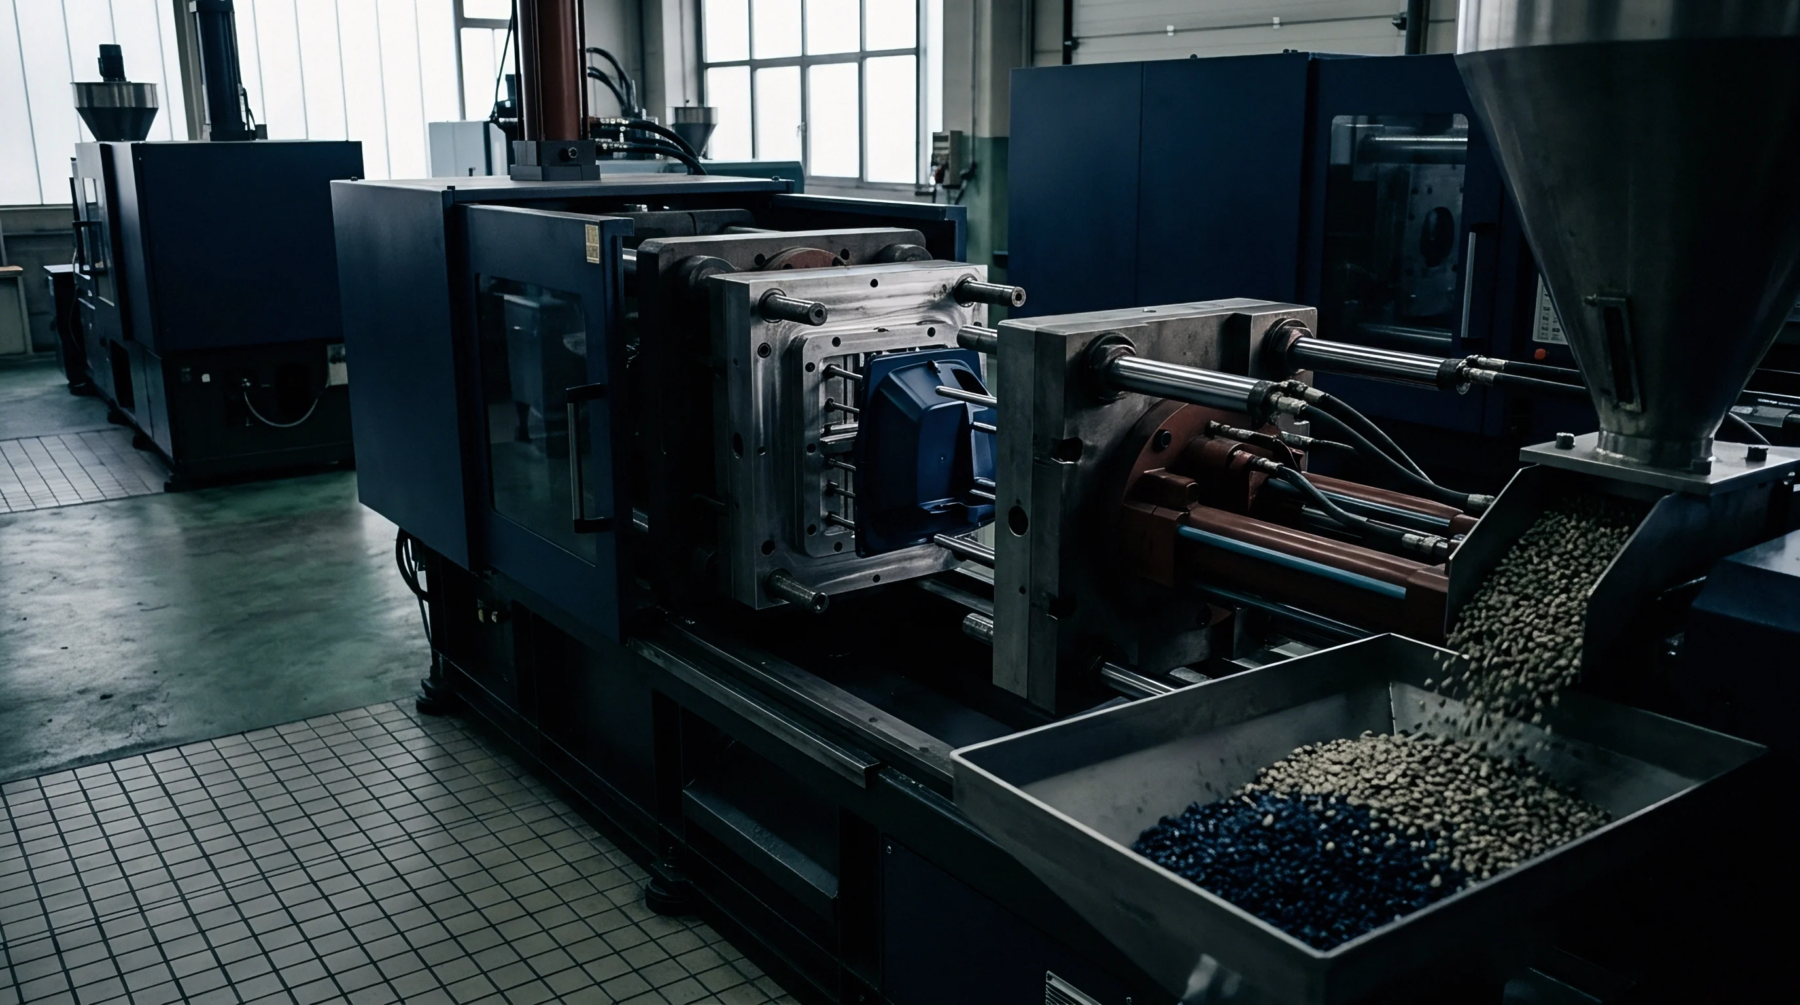
Dynamic sensor data collected from the interior of a moulding tool monitors the progression of plastic flow through a cycle. A cavity pressure trace maps force against time to reveal the exact moment the gate seals and the material reaches packing density. Engineers use this visual output to detect variations in viscosity that cause short shots or flash.
The resulting curve establishes the reference for consistent production by aligning the physical state of the resin with the machine settings.
Process Fidelity
Stability in high volume manufacturing relies on matching real time data against an established golden cycle. A cavity pressure trace identifies deviations in injection speed or holding pressure before those variances result in off specification parts. Moulders review the peak intensity and the integration of the area under the curve to verify that each shot fills the extremities of the mould.
Fluctuations in melt temperature or barrel pressure appear as shifts in the timing of the apex within the waveform. This feedback allows the automation software to divert individual units that fail to meet the preprogrammed tolerance limits. Operators maintain the system by verifying that the sensor placement remains clear of debris or thermal degradation that might damp the signal.
Precise monitoring of this waveform ensures that virgin material and regrind behave predictably throughout a long production run.
Material Response
Polymer rheology changes when additives or moisture levels drift during the injection phase. The cavity pressure trace tracks the resistance of the melt as it encounters the cold wall of the tool. Faster solidification rates shorten the duration of the curve while high molecular weight grades extend the period of peak pressure.
Variations in the cooling rate alter the internal crystallinity of the part, which manifests as changes in shrinkage or warpage. Technicians adjust the thermal control units to bring the waveform back into alignment with the established baseline. Consistent traces confirm that the material chemistry remains stable despite environmental changes in the facility.
Poor control of this variable leads to internal stresses that shorten the fatigue life of the final product.
Tooling Integrity
Mechanical health of the moulding tool remains linked to the profile of the injection stroke. A cavity pressure trace highlights excessive clamping force that prevents proper venting or restricted flow channels that cause premature cooling. Excessive spikes near the end of the stroke indicate potential damage to the mould surface or evidence of trapped gas in the cavity.
Monitoring these events protects the investment in expensive tooling by flagging wear before the steel suffers catastrophic deformation. Frequent review of the baseline allows the plant to schedule maintenance based on the actual degradation of the process rather than simple cycle counts. Every deviation in the pressure profile represents an opportunity to improve the efficiency of the plastic injection system.