Meaning
Evaluated batch resistance validation is a physical qualification procedure that exposes test specimens to aggressive chemical environments to confirm polymer integrity under stress. Polycarbonate housings and nylon brackets undergo this protocol during initial tooling sign off to determine whether molded components retain structural strength when exposed to cleaning agents or fuel blends. Production engineers execute the procedure immediately after injection molding trials stabilize cycle parameters.
Environmental stress cracking appears quickly if residual melt tension remains high or if annealing cycles prove inadequate. Virgin polymer compounds withstand standard chemical exposure thresholds during these trials without surface degradation, whereas high regrind ratios frequently develop microscopic fissures under identical load conditions. Material specifications define raw resin resistance through standardized tensile bars, while part specifications govern the actual geometry produced in production molds.
Laboratory test values reported on resin datasheets reflect ideal conditions achieved on pristine plaques, but actual components molded on shop floors often fail to hold those limits due to localized orientation and gate stress. Failure occurs when solvent exposure initiates micro cracks that propagate rapidly through amorphous zones until complete structural collapse takes place.
Thermal Drift
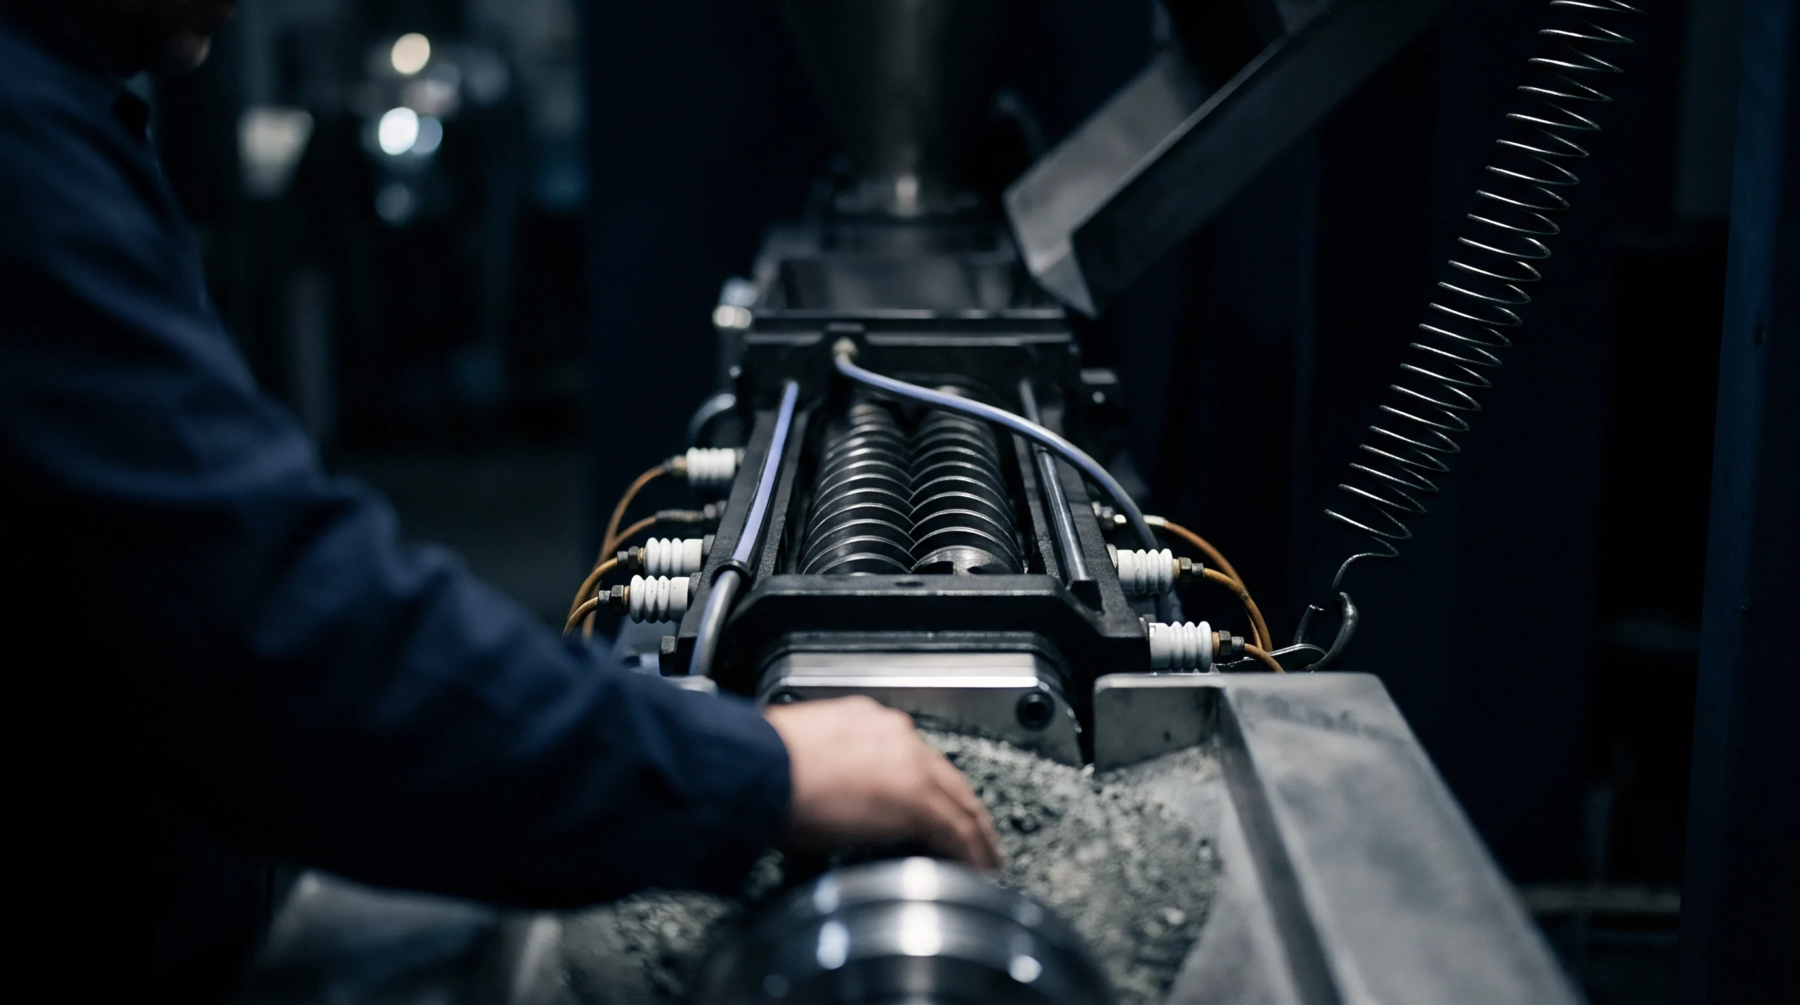
Melt temperature variations during injection molding alter molecular alignment and directly impact polymer performance during environmental exposure. Cylinder heating zones must maintain precise thermal stability because minor fluctuations change viscosity and induce internal stress within molded walls. Screw rotation speed and back pressure settings establish the shear rate applied to thermoplastic pellets prior to cavity injection.
Excessive barrel heat degrades polymer chains and weakens the final part against chemical attack. Cooling channels inside steel mold halves must circulate water at controlled flow rates to extract thermal energy uniformly across complex geometries. Toolmakers position these thermal circuits close to thick wall sections to prevent differential shrinkage and localized sink marks.
Pressure Gradient
Cavity packing pressure determines how densely polymer chains pack together during the final phase of injection molding. Hydraulic pressures applied by injection units govern the mass flow rate entering the mold tool during production runs. Inadequate holding pressure leaves internal voids that compromise structural integrity and accelerate chemical penetration during aggressive solvent exposure.
Clamping tonnage prevents mold halves from separating under high injection forces and maintains consistent wall thickness across every cavity. Part weight measurements verify that material density remains uniform throughout continuous production shifts.
Cost Impact
Scrap rates increase significantly when molded components fail environmental stress qualification protocols during initial quality sign off. Material waste accumulates on the shop floor whenever process parameters drift outside validated limits and cause premature part degradation. Tooling modifications required to correct internal stress patterns demand expensive machining alterations and extend production lead times before commercial release.
Resin selection strategies balance the lower cost of high regrind percentages against the elevated risk of failure during harsh chemical testing. Finished parts must survive aggressive exposure without losing mechanical performance to justify production economics across long manufacturing runs.