Meaning
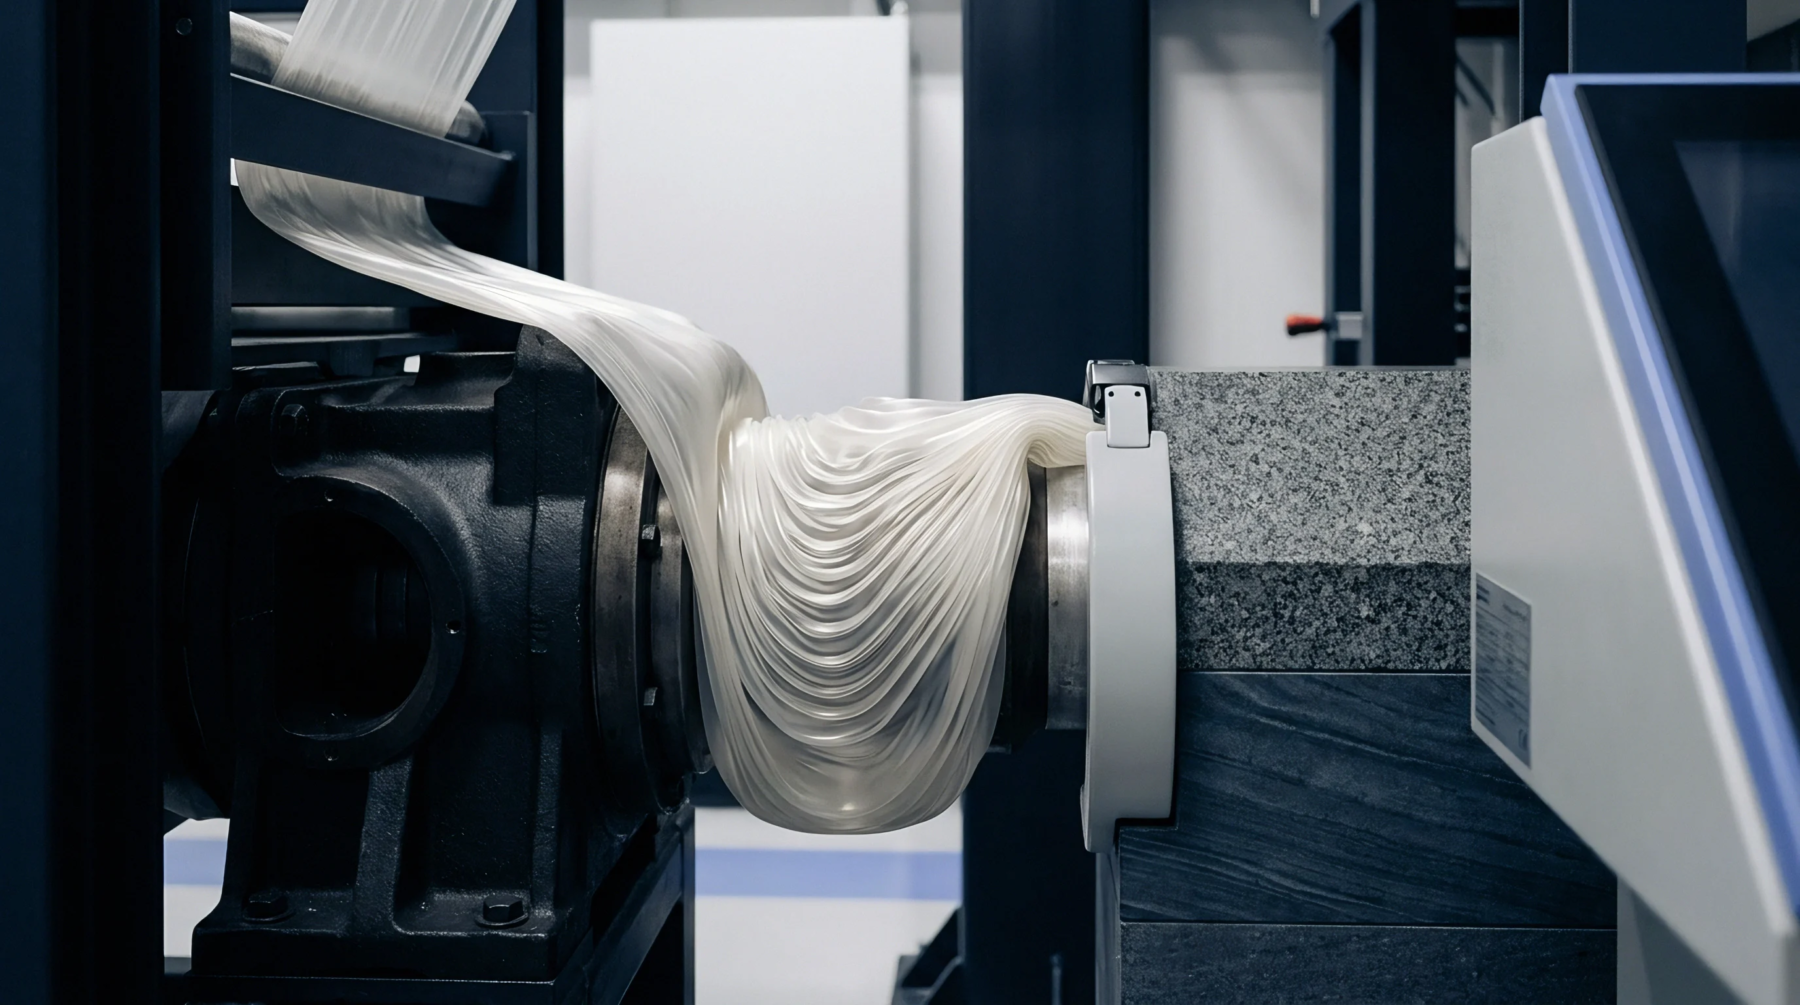
A quantitative property of molten polymers that represents the limit of Newtonian flow behavior observed as the shear rate approaches zero during high temperature processing. Within the rheological profile of a resin, zero-shear viscosity quantifies the internal friction of polymer chains at rest or under negligible deformation. It characterizes the material resistance to flow before shear-thinning effects dominate the mechanical response.
This metric defines the upper plateau of the viscosity curve and establishes the baseline for evaluating molecular weight distribution and branching levels in thermoplastic materials. Manufacturers rely on this value to predict how a melt will behave during low speed shaping operations or under gravitational forces alone. The property stops applying when high frequency strain rates induce chain orientation and disentanglement.
Rheological Bound
The parameter governs the sag resistance of parisons in blow moulding and the stability of extruded profiles before they enter a cooling stage. Proper control ensures that a resin maintains dimensional integrity when the cooling rate remains slow. If the value drops too far below the target for a given grade, the molten structure collapses under its own weight.
High values indicate strong melt strength while lower values allow for easier flow into complex mould geometries. Process engineers adjust temperature settings to keep this material attribute within the required range for stable production. Deviation from the expected range often causes wall thickness irregularities and non-uniform part weight across the output.
Moulding Performance
Virgin resins exhibit consistent performance levels compared to regrind batches where chain scission reduces the characteristic flow resistance. Datasheet values provide a standardized reference point obtained under controlled laboratory conditions using rotational rheometers. Moulders must translate these bench results into practical pressure requirements for injection equipment because actual machine conditions involve temperature gradients.
A stable value across a production run signals uniformity in raw material feed and consistent chemical stability within the hopper. Fluctuations during long cycles identify potential degradation or moisture contamination that necessitates immediate line intervention. Lower values allow for shorter cooling times in fast cycling applications but demand higher precision in holding pressure to prevent sink marks.
Processing Impact
Cost structures shift when a moulder selects a grade with different flow characteristics to optimize throughput. Higher zero-shear viscosity requires more energy to move the melt through the nozzle and gate regions during the initial stages of a cycle. Optimizing for this variable reduces the energy expenditure per unit produced by aligning the material flow resistance with the capability of the press.
Excessively high resistance causes structural stress or incomplete filling if the injection unit reaches its force limit. Precision in these metrics keeps machine wear predictable by preventing overpressurization during the filling phase. Successful control of this material property represents the fundamental limit of efficient thermoplastic processing.