Meaning
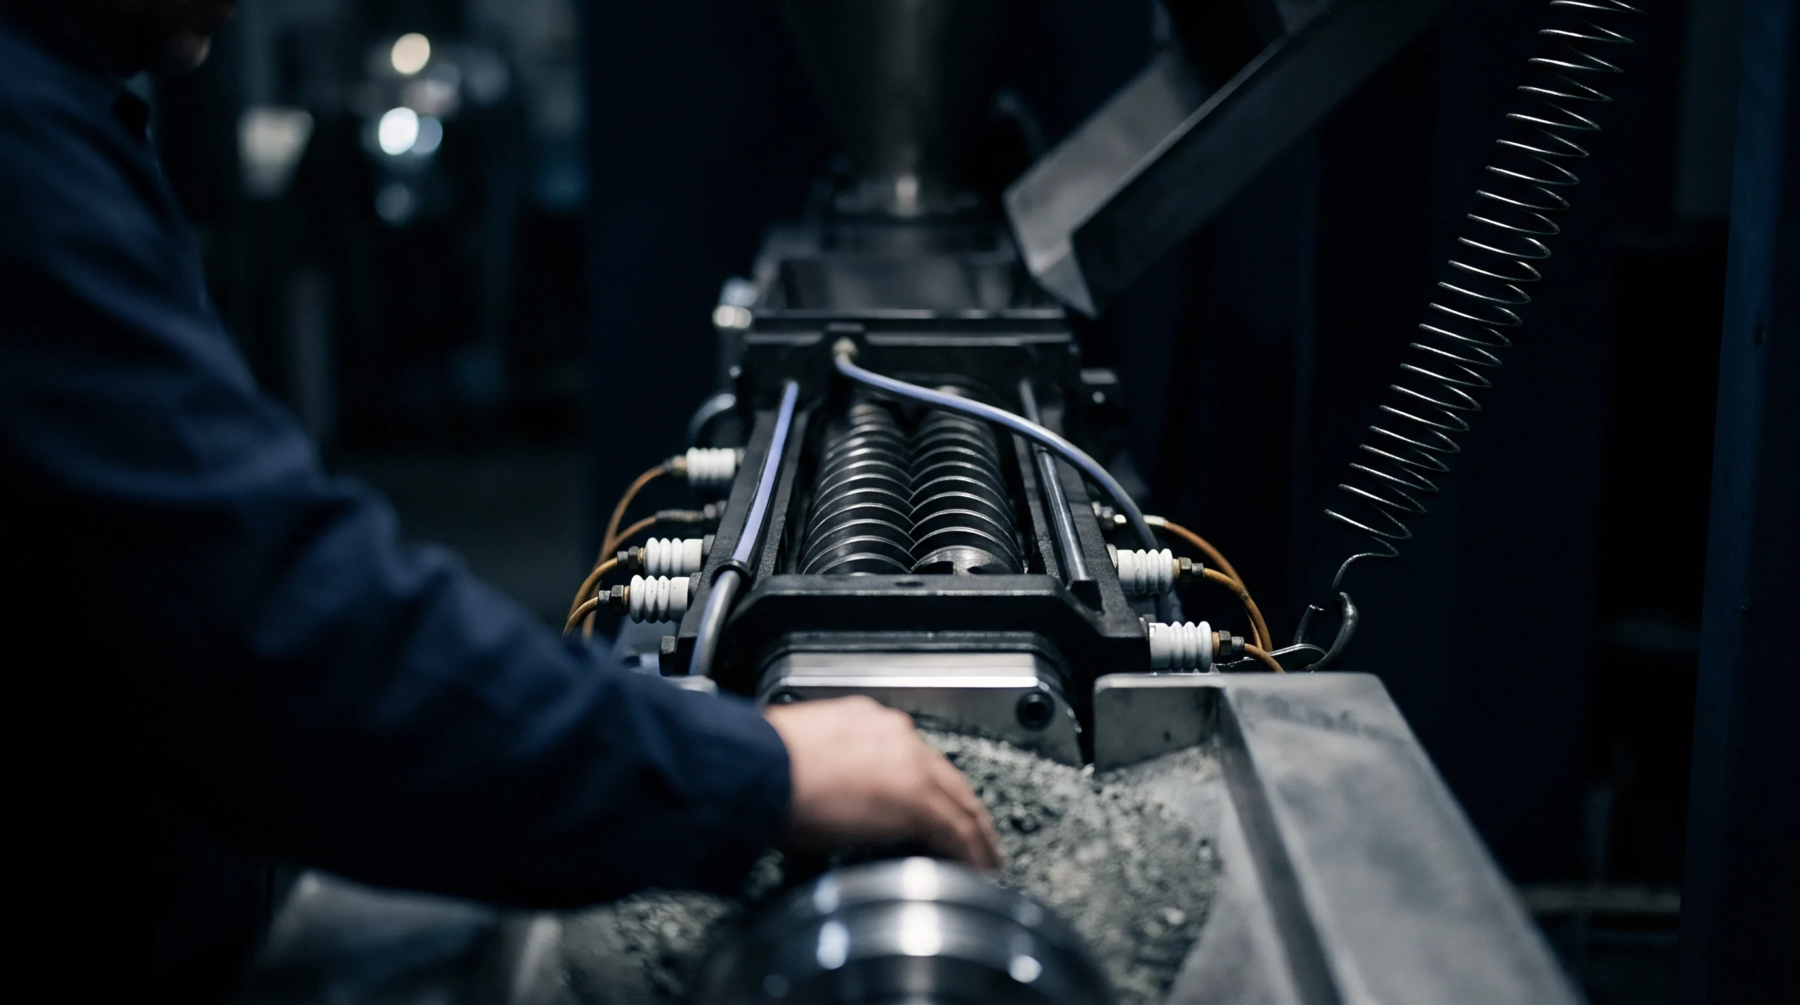
Continuous melt-mixing manufacturing processes utilize two intermeshing, co-rotating or counter-rotating screws housed within a modular barrel to blend additives, reinforcements, and modifiers into molten polymer matrices. Industrial twin screw compounding disperses color pigments, flame retardants, impact modifiers, and chopped glass fibers into base resins with high distributive and dispersive mixing efficiency. The equipment allows precise control over shear energy, melt temperature profiles, residence time distributions, and devolatilization across multiple barrel zones.
The process ceases to apply to single-screw homogenizing extruders that lack modular kneading elements, co-rotating intermeshing wiping actions, and multi-port sidestream feeding capabilities.
Melt Homogenization
Modular screw shafts allow compounders to assemble customized configurations of forward conveying elements, reverse kneading blocks, and specialized mixing gears tailored to specific resin rheologies. As solid polymer pellets enter the feed throat, conveying elements transport the material into high-shear kneading zones where mechanical energy and external barrel heaters melt the polymer rapidly. Utilizing twin screw compounding ensures that additives achieve uniform spatial distribution throughout the viscous melt stream.
Self-wiping co-rotating screw geometries prevent material stagnation on barrel surfaces, minimizing thermal degradation risks during processing of heat-sensitive engineering polymers.
Additive Dispersion
Downstream side feeders introduce delicate mineral fillers or chopped glass fibers directly into the fully molten polymer stream, minimizing mechanical attrition and screw wear. High-shear dispersive mixing elements break down pigment agglomerates into primary sub-micron particles, ensuring uniform color strength and surface aesthetics in the final compound. For rubber-toughened formulations, precise shear fields govern the domain size distribution of elastomeric impact modifiers within the rigid matrix.
Controlling specific mechanical energy input during mixing preserves fiber aspect ratios, maximizing the tensile and impact strength of structural engineering compounds.
Degassing Stage
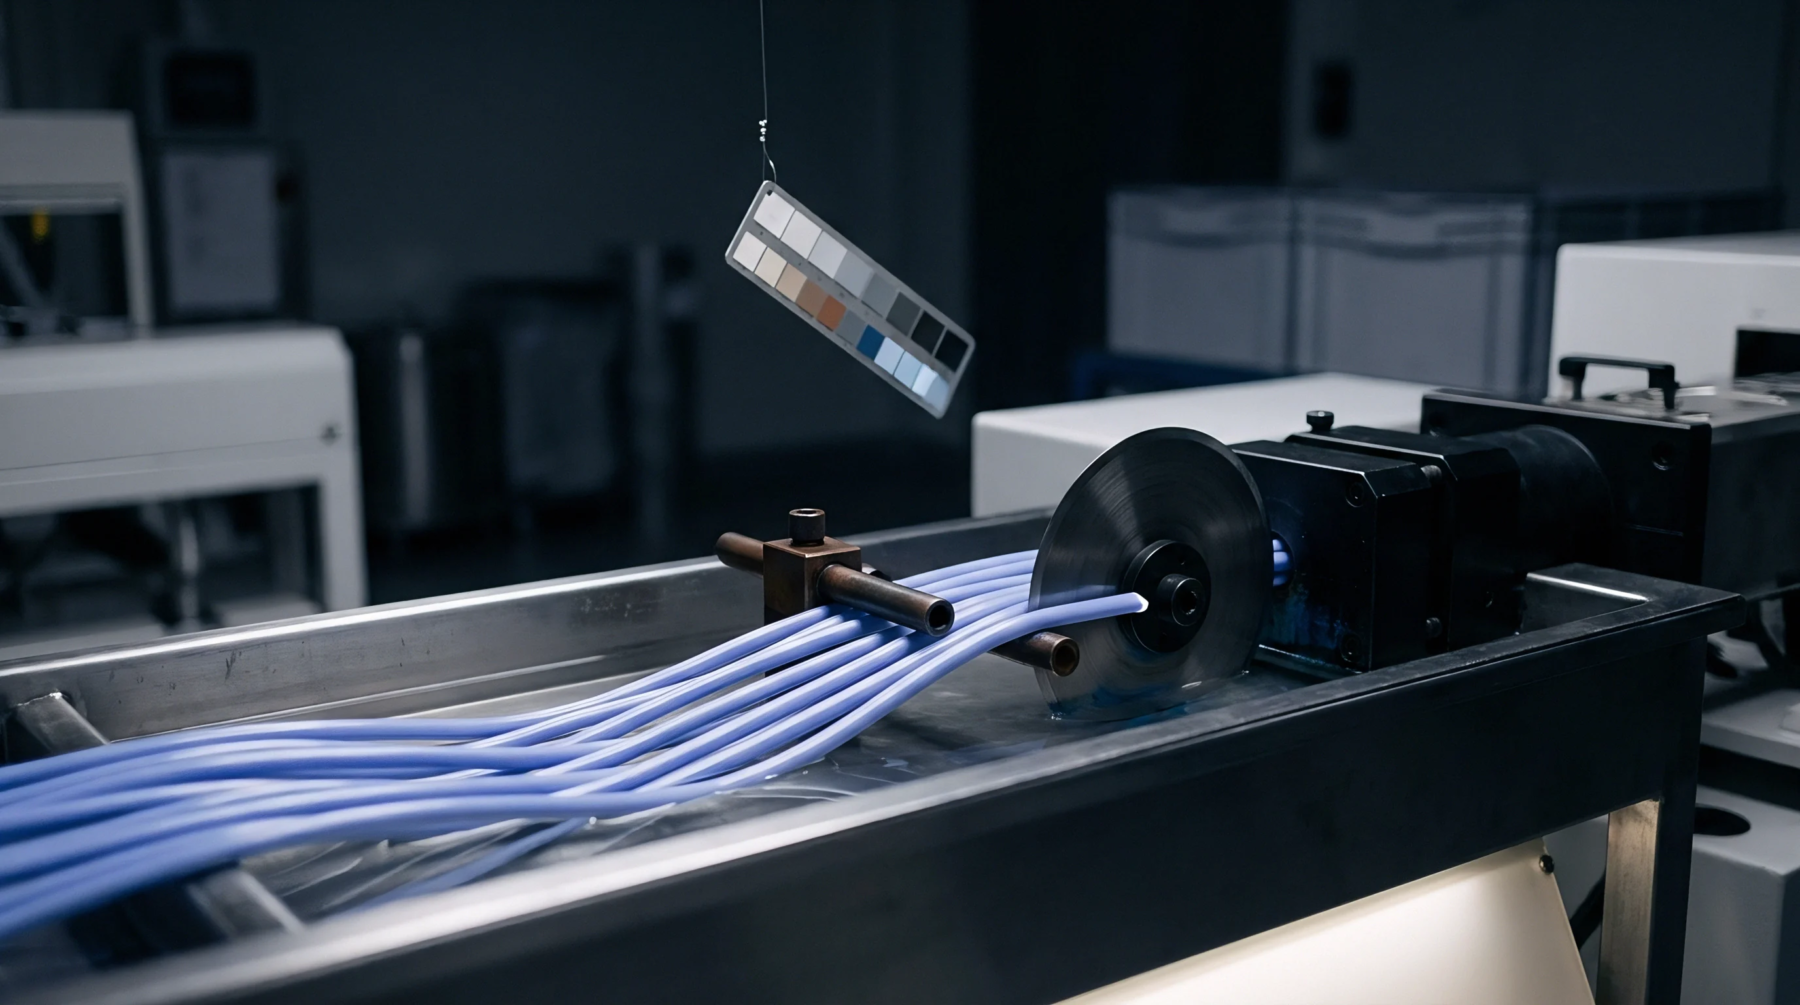
Multiple atmospheric and vacuum venting ports along the barrel strip away moisture, entrapped air, residual monomers, and volatile degradation products from the melt before pelletization. Efficient devolatilization prevents internal foaming, porosity, and hydrolytic degradation during subsequent injection moulding or profile extrusion processes. At the end of the barrel, a high-pressure melt pump or metering screw zone forces the homogenous blend through a multi-hole strand die into water cooling baths and high-speed strand pelletizers.
Twin screw compounding remains the primary industrial technique for formulating high-performance polymer compounds and masterbatches.