
Quantifying Inter Cavity Thermal Drift Rates in High Cavitation Tool Steel Assemblies
Inter-cavity thermal drift in high-cavitation steel tooling shifts part dimensions; turbulent coolant flow and conductive inserts eliminate temperature spreads.
Inter-cavity thermal drift in high-cavitation steel tooling shifts part dimensions; turbulent coolant flow and conductive inserts eliminate temperature spreads.
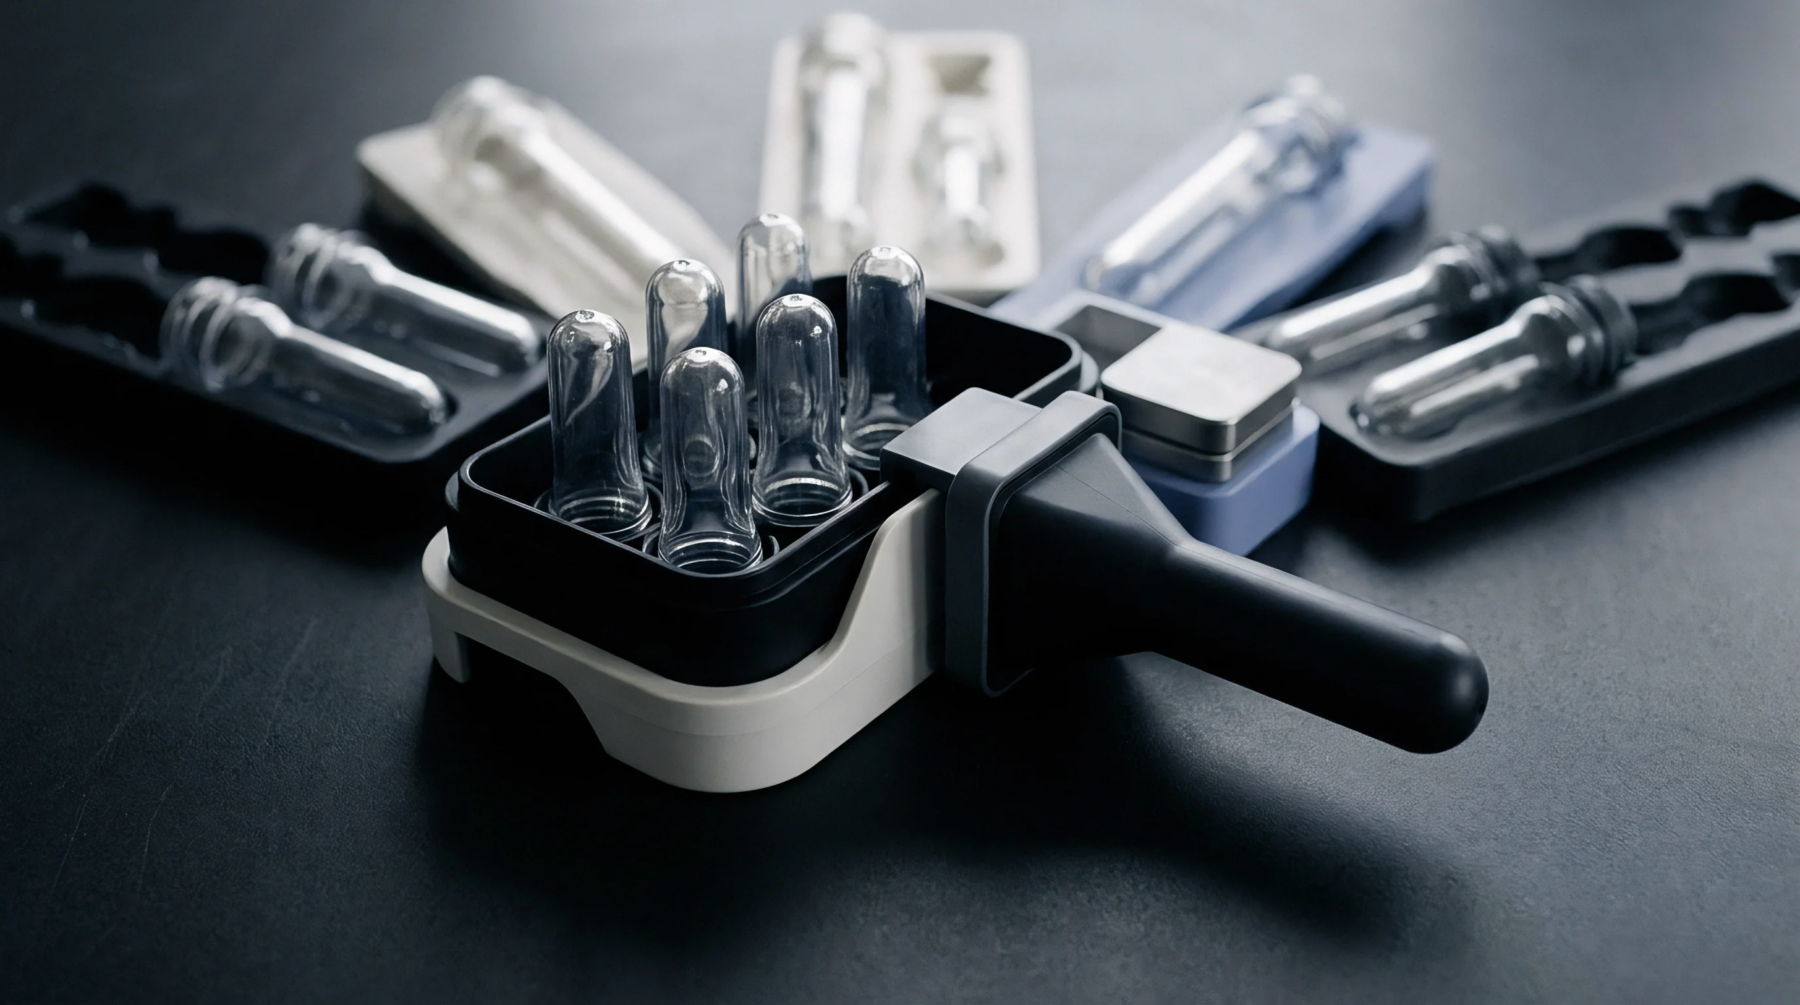
Optimal cavitation balances machine hourly rates, clamp tonnage, and shot capacity against thermal cooling limits and cross-cavity dimensional distribution.
Decoupled molding isolates fill velocity from hold pressure to neutralize resin viscosity variations and hold precision tolerances across volume runs.
Cooling circuit design dictates actual injection cycle time; quotes assuming unrealistically fast cooling cause part warpage or forced piece-price increases.

Non-uniform tool steel thermal expansion creates spatial cavity temperature deltas that drive measurable dimensional drift across multi-cavity molds.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.