Managing Polymer Volumetric Shrinkage Anisotropy during Tool Cavity Steel Adjustment
Decouple shrinkage into longitudinal and transverse vectors, retain steel-safe cavity stock, and adjust EDM offsets after measuring first-shot parts.
Decouple shrinkage into longitudinal and transverse vectors, retain steel-safe cavity stock, and adjust EDM offsets after measuring first-shot parts.
High packing stress forces polymer skins into steel micro-grooves, increasing heat transfer while elevating ejection drag through viscoelastic keying.
Sub-millimetre telemetry cavity accuracy requires compensating for steel expansion and polymer dielectric drift via real-time press-side calibration.
Managing shear imbalance across high-density cavities depends on rotating channel boundary layers at runner splits to equalize melt viscosity before gating.
Real-time hydraulic and cavity pressure integral evaluation isolates sub-gram part variations within a 10-millisecond window to automate defect rejection before mold open.
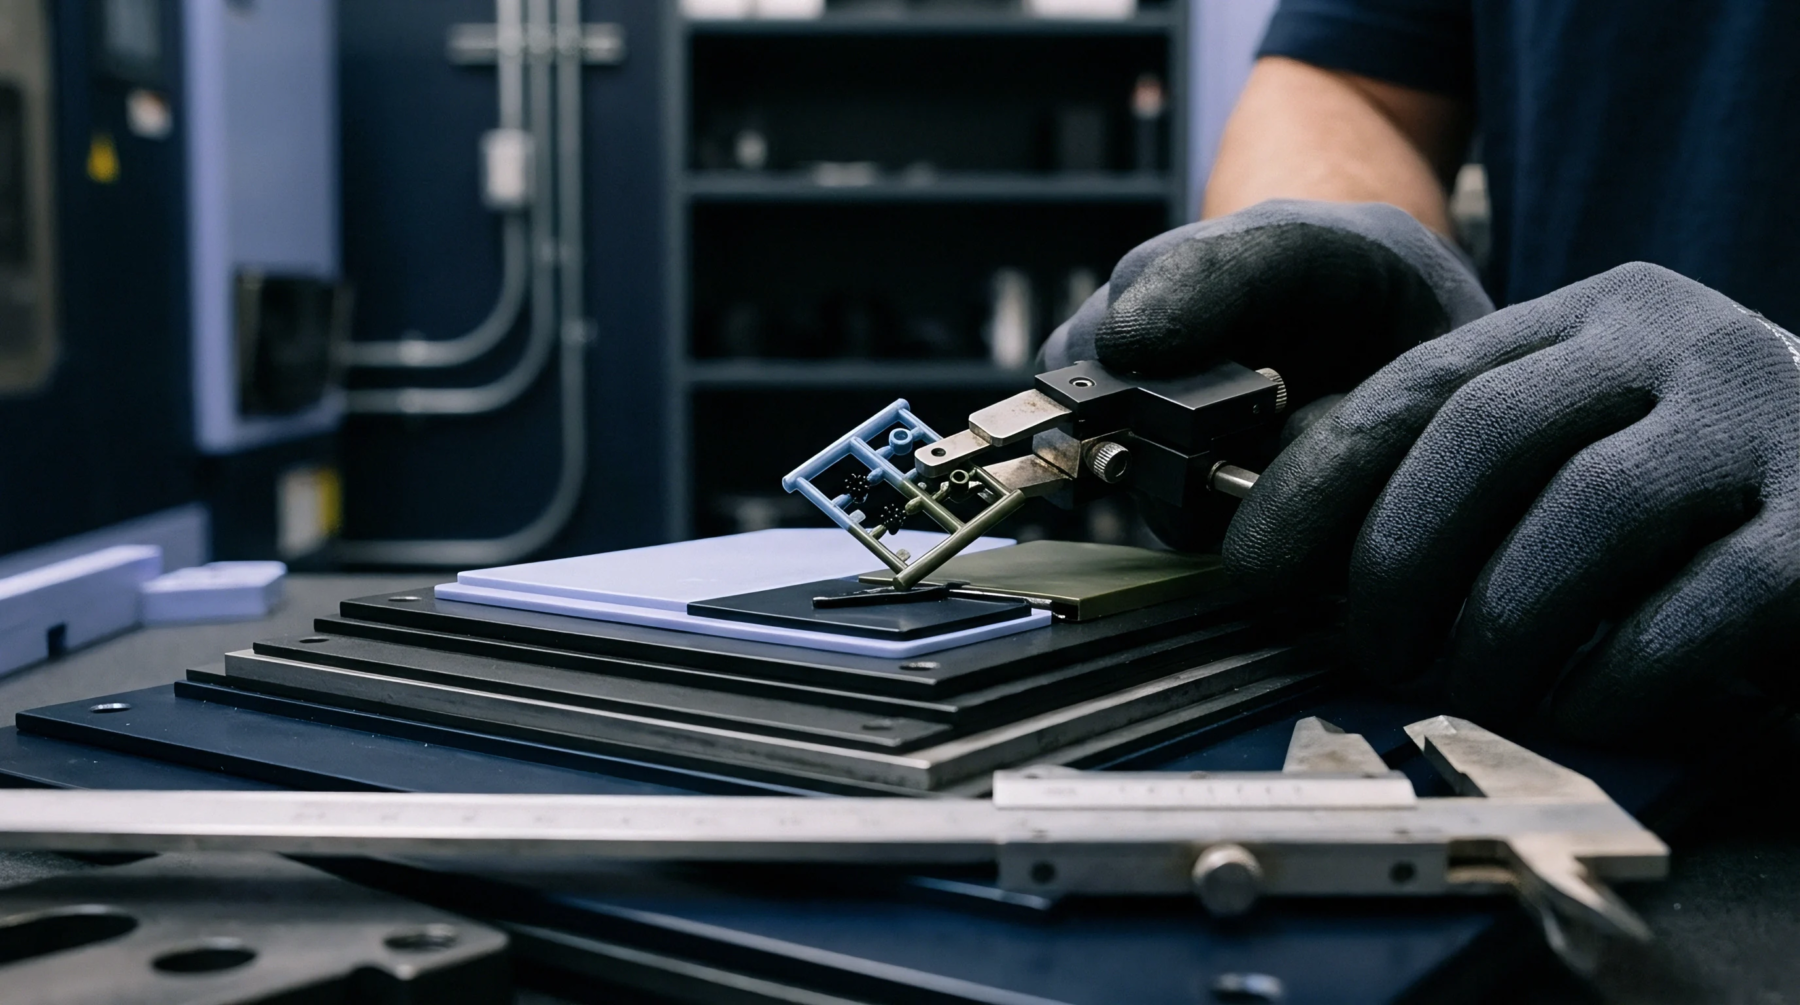
Cavity pressure measurement in micro-injection tooling decouples machine dynamics from cavity fill, eliminating part weight variance and micro-defects.
Non-uniform tool steel thermal expansion creates spatial cavity temperature deltas that drive measurable dimensional drift across multi-cavity molds.
Press-side verification requires dynamic fill balance testing, telemetry pressure mapping, and individual cavity Cpk qualification before tool release.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.