Determining Polyamide Moisture Content Limits before Processing
Polyamide processing demands moisture below 0.15 percent for standard molding and 0.05 percent for structural grades to prevent irreversible chain cleavage.
Ceiling
Incoming polyamide resin arrives with moisture specifications dictated by polymer backbone chemistry and the target conversion process. Unfilled polyamide 6 and polyamide 66 tolerate an upper processing limit of 0.20 percent water by weight for standard commercial injection moulding, while technical components carrying structural load call for a tighter ceiling of 0.10 to 0.12 percent. High-temperature semi-aromatic grades and short-chain aliphatics behave with far less forgiveness.
Polyamide 46 cleaves chains rapidly above 0.05 percent moisture, and polyphthalamide formulations demand moisture levels below 0.03 to 0.04 percent prior to screw intake. Extrusion operations establish an even narrower operating band than moulding. Sheet, tube, and profile lines operate between 0.03 and 0.07 percent moisture to prevent surging, foaming, and melt collapse at the calibration die.
Water functions as an aggressive plasticizer and reactant within molten polyamides. As melt temperature climbs past 260 degrees Celsius in PA66 or 300 degrees Celsius in PPA, excess moisture drives equilibrium hydrolytic scission across the amide bonds. The process halves the polymer number-average molecular weight inside ninety seconds of barrel residence time.
Melt viscosity drops precipitously. The moulder observes splay, drool at the nozzle tip, and flash along parting lines. When dry-as-moulded parts exit the tool, tensile strength and elongation at break fall thirty to sixty percent short of technical datasheet values.
| Polymer Chemistry | Melting Temperature | Injection Moulding Ceiling | Extrusion Ceiling | Degradation Mechanism |
|---|---|---|---|---|
| Polyamide 6 | 220 °C | 0.20 wt% | 0.05 wt% | Hydrolytic scission, flash |
| Polyamide 66 | 262 °C | 0.15 wt% | 0.04 wt% | Rapid cleavage, splay mark |
| Polyamide 46 | 295 °C | 0.05 wt% | 0.02 wt% | Extreme chain fragmentation |
| Polyamide 12 | 178 °C | 0.10 wt% | 0.04 wt% | Die drool, bubble collapse |
| Polyphthalamide | 310 °C | 0.04 wt% | 0.02 wt% | Explosive outgassing, voiding |
Setting moisture boundaries also guards against over-drying. Removing water past 0.02 percent in unreinforced PA66 generates severe operational disruptions through solid-state post-condensation. Molecular weight increases inside the machine barrel.
Melt viscosity spikes unpredictably. Thin-wall tool cavities exhibit short shots, excessive shear heating scorches the additive package, and screw recovery times lengthen. A balanced moisture target maintains mechanical integrity while preserving stable rheology.
Procurement teams evaluate grade specifications against these physical limits before releasing purchase orders. Resin data sheets quote dry-as-moulded mechanical metrics achieved strictly within target moisture windows. Parts moulded from pellets exceeding these water concentration ceilings shatter under dynamic impact loads during secondary assembly, leaving the moulder with unrecoverable finished-goods scrap and immediate commercial liability.
Steam
Atmospheric exposure converts dry polyamide granules into water-laden processing hazards within brief operational windows. The polar amide linkages throughout the polymer chain form rapid hydrogen bonds with ambient water vapor. Unfilled polyamide 6 pellets absorb water at an initial rate exceeding 0.10 percent per hour when staged in open air at 23 degrees Celsius and 50 percent relative humidity.
Saturated equilibrium values reach up to 9.5 percent total moisture in PA6 and 8.0 percent in PA66. Slower-absorbing long-chain chemistries such as polyamide 11 and polyamide 12 level off between 1.5 and 2.0 percent saturation, protected by their longer aliphatic hydrocarbon spacers.
Polyamide 66 exposed to 50 percent relative humidity at 23 degrees Celsius absorbs 0.20 percent moisture by weight within four hours of unsealed hopper exposure.
Pellet morphology determines sorption velocity. Extruded cylindrical granules carry high surface-area-to-volume ratios that pull water molecules into outer crystalline boundaries within minutes. The core remains glassy while the outer shell plasticizes.
When these pellets hit the heated screw, surface moisture transforms into high-pressure vapor pockets inside the feed zone. The vapor forces its way through the melt pool, ripping molten polymer streams apart.
Why Do Equilibrium Isotherms Dictate Residence Windows?
Sorption isotherms govern how rapidly dried inventory regains ambient moisture once staging bags rupture. Desiccant-dried granules discharged from a hopper at 0.04 percent moisture begin re-equilibration immediately upon contact with ambient shop floor air. Moisture uptake follows Fickian diffusion kinetics in the initial phase, accelerated by high factory ambient temperatures.
Moulding operations without closed-loop nitrogen conveyance or dry-air blanketed machine hoppers experience uncontrolled drift. A machine operator staging twenty-five-kilogram open containers at 60 percent relative humidity injects wet resin into the throat before the shift ends. The melt flow index climbs across the production run as barrel residence water levels double.
Parts moulded at noon display brittle fracture modes absent from early-morning shots.
Molten water molecules split amide links at processing temperatures before cavity pressure develops.
Unfilled resins absorb water faster than reinforced formulations. Glass fiber additions act as inert mass, reducing the active polymer volume per kilogram of material. A thirty-percent glass-filled PA66 absorbs roughly thirty percent less total ambient water by weight than neat resin over identical staging intervals.
The critical moisture ceiling on neat resin weight remains unchanged, meaning the allowable water mass measured on the composite pellet scales down accordingly.
Current research leaves unresolved whether non-uniform water concentration gradients between pellet core and pellet surface accelerate thermal degradation faster than homogeneous moisture distributions of identical total mass fraction.
Titration
Accurate laboratory quantification of moisture in polyamides demands analytical techniques that isolate water from volatile compounding additives. Standard loss-on-drying halogen balances heat samples to 160 degrees Celsius and measure total mass loss. This crude thermal approach fails on polyamide compounds.
Heat volatilizes caprolactam monomers, oligomeric waxes, lubricants, and thermal stabilizers alongside water vapor. A loss-on-drying balance routinely overstates true moisture content by 0.08 to 0.25 percent, leading technicians to scrap good resin or over-dry incoming lots.
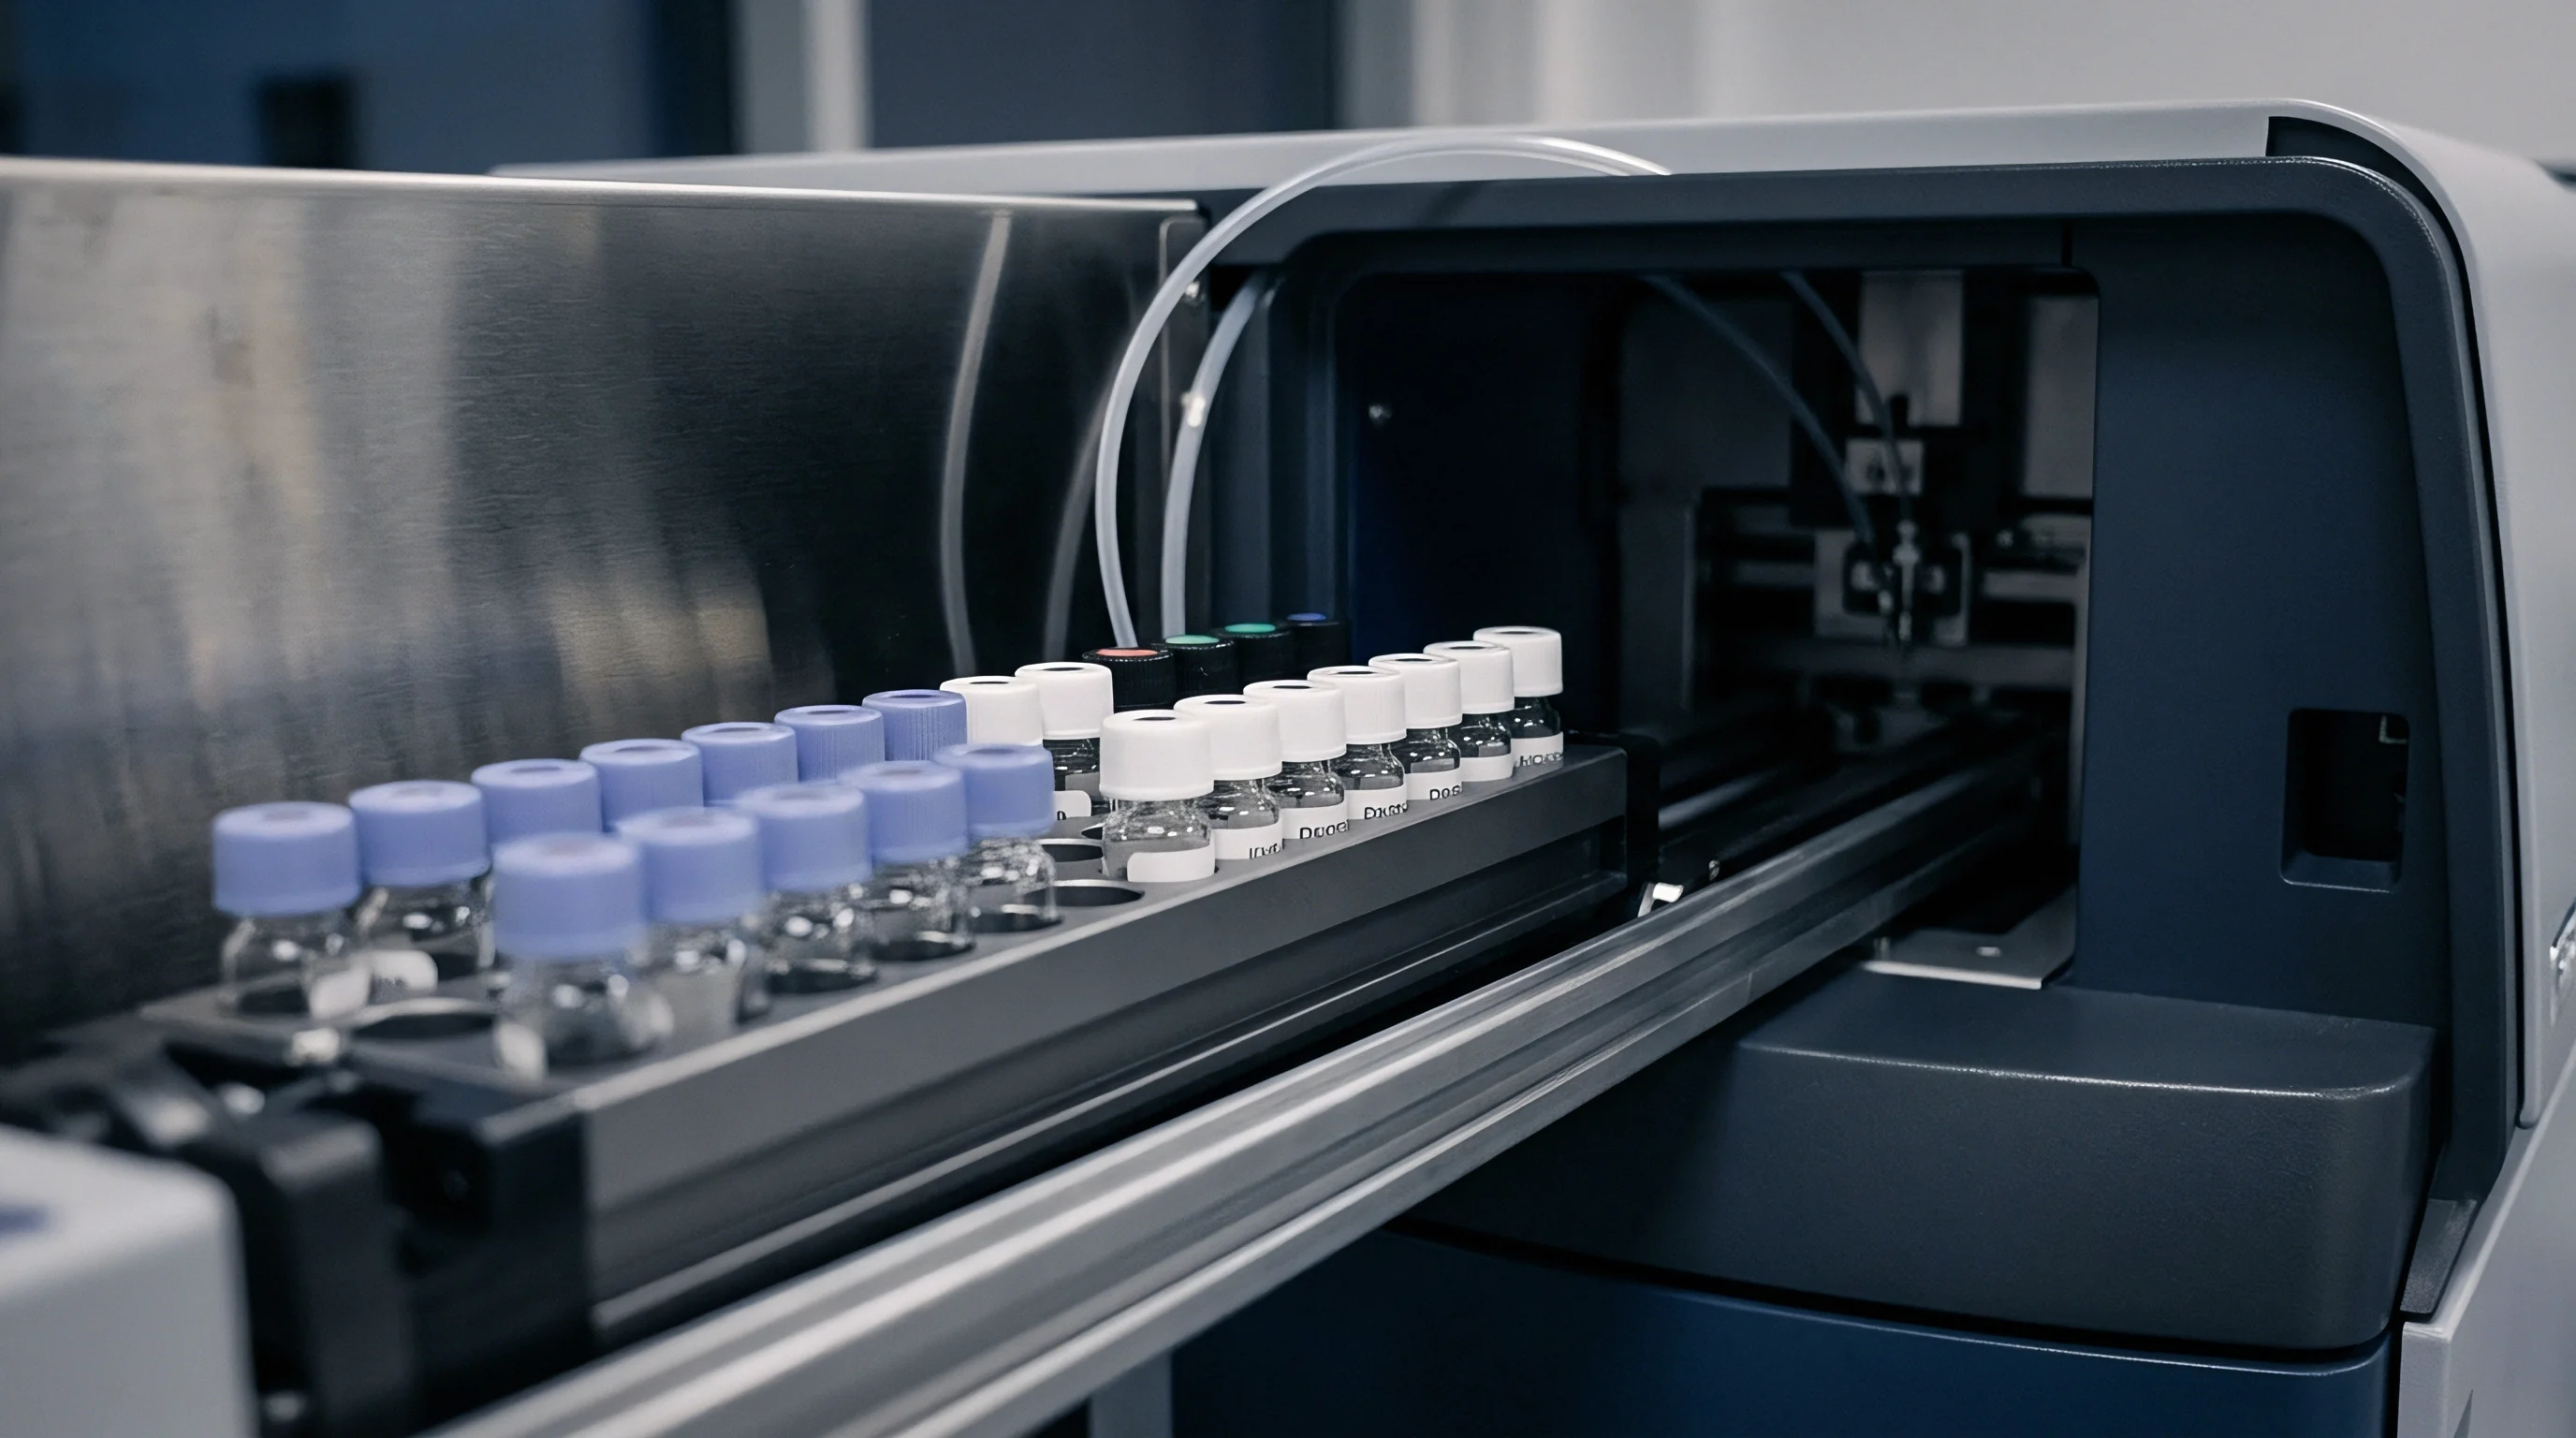
International standard ISO 15512 establishes the definitive reference methods for water content determination across technical polyamides. Method B, incorporating coulometric Karl Fischer titration with an integrated vaporization oven, delivers the industry standard for precision. Solid granules enter a sealed heating tube operating between 180 and 220 degrees Celsius.
Dry carrier gas transports vaporized moisture directly into a titration cell filled with iodine-generating reagent. Coulometric titration calculates absolute water mass based on the electric current consumed during electrochemical reaction with iodine.
- Sample collection proceeds at the staging dock using an airtight moisture sampling bottle filled to capacity and capped within twenty seconds of opening the shipping bag.
- Analytical balance weighing establishes raw specimen mass between 0.500 and 2.000 grams with precision down to 0.1 milligrams.
- Thermal extraction vaporizes water inside the tube furnace at 200 degrees Celsius under a regulated dry nitrogen sweep rate of 300 milliliters per minute.
- Coulometric detection records total iodine consumption until the endpoint reaction current drops below five micrograms of water per minute.
- Blank subtraction removes ambient atmospheric carrier interference from the final calculated moisture percentage.
The field relies alternately on water-specific sensor instruments defined under ISO 15512 Method C. These analyzers pass dry carrier gas over heated pellets into an electrolytic phosphorus pentoxide cell or an optical infrared sensor. Phosphorus pentoxide selectively binds water molecules and electrolyzes them into hydrogen and oxygen. The consumed current provides direct, selective water mass calculation without interference from organic volatiles.
Cycle times drop to under fifteen minutes, providing shop-floor technicians with real-time verification before hopper loading.
| Method Designation | Measurement Principle | Temperature Window | Selectivity to Water | Typical Cycle Time |
|---|---|---|---|---|
| ISO 15512 Method A | Extraction with boiling alcohol | Reflux temperature | High specificity | 120 to 180 minutes |
| ISO 15512 Method B1 | Vaporization oven into Karl Fischer | 180 °C to 220 °C | Absolute specificity | 10 to 20 minutes |
| ISO 15512 Method B2 | Direct liquid reagent injection | Ambient dissolution | Absolute specificity | 30 to 45 minutes |
| ISO 15512 Method C | Thermal desorption into P2O5 sensor | 160 °C to 200 °C | High specificity | 12 to 18 minutes |
| Loss on Drying | Thermogravimetric balance mass drop | 120 °C to 160 °C | No specificity | 15 to 30 minutes |
| Loss on drying methods volatilize caprolactam monomers, lubricants, and low-molecular additives, distorting measurements across all aliphatic polyamides. | ||||
ASTM D6869 provides the parallel North American operating standard for coulometric extraction. Incoming inspection operations execute verification tests according to standardized sampling plans. Technicians draw material from the bottom, center, and top thirds of an incoming gaylord or bulk bag.
Single-point surface sampling yields false wet readings from condensation or false dry readings from desiccated top layers.
Purchase contracts governed by DIN EN 10204 Type 3.1 inspection certification bind suppliers to Karl Fischer Method B results, superseding warehouse balance readings whenever moisture disputes trigger formal freight rejection.
Barrel
Inside the plastification zone, trapped water triggers rapid chain fragmentation under combined shear stress and thermal energy. High temperatures accelerate the thermodynamic reversal of the polycondensation reaction that initially built the polymer chains. Hydrolytic scission breaks the main polymer backbone, transforming high molecular weight polymer into short oligomers terminated by amine and carboxylic acid end groups.
Dynamic viscosity falls precipitously. The polymer melt flows like oil through hot runner manifolds.
Pellets cut clean under a blade show dry centers, while pellets that smear or tear carry trapped core moisture.
Viscosity loss destabilizes cavity filling patterns. Tool cavities flash at nominal clamp tonnages. Material drools uncontrollably from the nozzle during screw recovery, fouling sprue bushings and delaying automated robotic part take-out.
Operators combating drool often introduce excessive suck-back distances. Suck-back draws ambient air through the nozzle tip, introducing cold air pockets that oxidize the remaining melt pool. Degraded resin builds dark, burnt deposits on the screw flights and check ring assemblies.
Is Melt Depolymerization Reversible inside the Screw?
Machine barrel residence times do not permit solid-state re-condensation of cleaved polyamide chains. Polycondensation releases water as a byproduct, demanding vacuum extraction and extended residence times measured in hours to rebuild polymer chains. The injection barrel functions as a closed, pressurized reactor with zero vacuum venting along the metering zone.
Cleaved chains remain degraded throughout the filling, packing, and cooling phases.
Extrusion lines with dual-vented vacuum degas zones remove vapor prior to the metering section. Vented screws reduce trapped steam bubbles but cannot restore chains cleaved in the melting transition. The initial breakdown occurs in the compression zone where unmolten pellets contact high-temperature barrel walls.
Molecular degradation remains locked into the polymer matrix.
- Silver splay patterns streak radially outward from the gate across cosmetic surfaces where trapped steam bubbles burst against the chilled mould steel.
- Internal microvoiding forms porous cellular pockets within thick structural ribs, creating localized stress risers that nucleate premature fatigue fractures.
- Molecular weight loss reduces intrinsic viscosity, causing parts to fail Izod impact tests and snap under minor deflection loads.
- Parting line flash escapes past steel gaps as low melt viscosity allows fluid polymer penetration into shut-offs.
- Additive precipitation emerges on the component finish as liberated oligomers and unbonded waxes migrate to the cooling surface.
Impact-modified and flame-retardant polyamide compounds suffer compounded damage. Water hydrolyzes maleic anhydride functional groups on elastomer impact modifiers, preventing rubber droplets from bonding to the polyamide matrix. Impact performance collapses.
In brominated or red-phosphorus flame-retardant grades, moisture generates acid byproducts at 280 degrees Celsius. These acidic vapors pit high-grade chrome mould steels, stripping cavity polish and destroying production tools.
A continuous process runs smoothly only when pellets enter the feed throat dry enough that the purge bead drops glassy, uniform, and free of foam.
Penalty
Processing wet resin generates immediate financial losses across production and assembly operations. The primary loss appears as scrap generation during start-up and steady-state moulding. Parts exhibiting silver splay, flash, or voiding cannot enter commercial inventory.
In high-volume automotive moulding, a scrap rate jump from 1.5 percent to 8.0 percent caused by unmonitored dryer dew-point drift destroys shift profitability. Scrap regrind cannot offset this loss. Regrinding hydrolytically degraded polyamides doubles thermal degradation during the second heat history, forcing moulders to downgrade or discard contaminated sprues.
ISO 15512 Method B water determination figures override carrier loss-on-drying printouts when settlement disputes reach arbitration.
The catastrophic commercial exposure lands when degraded parts pass visual inspection and ship to end customers. Polymeric hydrolytic cleavage does not change the dry-as-moulded visual color or surface gloss when moisture remains marginally below the splay threshold, between 0.22 and 0.28 percent. Parts fill the mould cleanly.
Dimensions match drawing tolerances. Impact performance, however, collapses.
A typical structural automotive bracket moulded from thirty-percent glass-reinforced PA66 provides a clear illustration of this hidden exposure. Assume a forty-tonne resin order converted into 200,000 structural brackets valued at 4.50 dollars per unit. Pellets processed at 0.28 percent moisture due to a saturated desiccant bed lose forty percent of their notched Izod impact resistance.
Tensile elongation drops from 3.5 percent to 1.8 percent. The defect escapes visual factory checks.
Secondary automated screwdriving lines snap the mounting bosses during assembly four weeks later. The automotive customer halts assembly lines, charges back downtime penalties reaching tens of thousands of dollars per hour, and mandates a complete product containment sort. The total liability exceeds 900,000 dollars on a resin purchase order that cost 140,000 dollars.
Resin suppliers deny warranty claims when their shipping documents prove resin left the compounding plant within 0.10 percent moisture specifications in intact, foil-lined barrier packaging.
Packaging integrity preserves or destroys the resin asset during ocean transit and long-term storage. Polyamide grades packed in multi-wall paper bags without hermetic aluminum barrier foil liners absorb 0.50 percent moisture per month during maritime transport across high-humidity sea lanes. Sourcing teams purchasing spot resin lots at warehouse discounts inherit moisture liabilities that exhaust dry-air drying capacity on the shop floor.
Desiccant dryers running four hours at 80 degrees Celsius consume significant energy while fighting high moisture loads, raising landed processing costs per good part.
Incoming inspection procedures with verified water testing protect processing margins before material enters the production stream. Staging dry pellets, sealing hoppers, monitoring dryer dew points at minus forty degrees Celsius, and enforcing strict moisture limits eliminate the invisible chain cleavage that turns technical polyamide parts into assembly line failures.