Standard Coulometric Moisture Determination Methods in Polyester Quality Control
Coulometric Karl Fischer titration with thermal vaporization quantifies micro-ppm moisture in polyesters to prevent hydrolytic chain scission during processing.
Cell
Direct coulometric titration relies on stoichiometric electrochemical reactions where generated triiodide reacts with moisture in an anolyte solution. In thermoplastic polyester quality control, measuring trace moisture requires electrochemical precision because polyesters such as polyethylene terephthalate and polybutylene terephthalate undergo rapid hydrolytic degradation during thermal processing when absorbed water exceeds specific thresholds. Water molecules at elevated melt temperatures cleave the ester linkages along the polymer backbone, reducing molecular weight and causing severe mechanical failure in molded parts.
Stoichiometric Iodine Generation
Electrolysis converts iodide ions into elemental reagent within the closed vessel. The coulometric process generates iodine anodically from an anolyte solution containing iodide ions, sulfur dioxide, an amine base such as imidazole, and an alcohol solvent. When a sample containing water enters the reagent mixture, iodine reacts strictly according to the classical Karl Fischer reaction mechanism.
Iodine oxidation follows Faraday law.
One mole of water reacts quantitatively with one mole of iodine. The anodic oxidation reaction generates iodine at a rate proportional to the electric current passed through the generator electrode. The total charge required to reach the end point directly determines the mass of water present in the reaction vessel.
Coulometric cell current integration measures water masses down to one microgram when purged with dry gas flowing at constant pressure.
Micro-PPM Sensitivity Limits
Polymeric resins require moisture measurement capabilities down to single-digit mass fractions. Volumetric Karl Fischer methods suffer from burette delivery resolution limits and titrant standardization drift when quantifying moisture levels below one hundred parts per million. Coulometric determination eliminates titrant volume measurement entirely by calculating moisture mass directly from integrated current over time.
Water calculation requires current integration. Anodic generation produces two moles of electrons for every mole of water consumed. A charge of 10.72 Coulombs corresponds to exactly one milligram of water.
Cell current stays steady. Current resolution in microamperes enables the detection of water quantities as small as one microgram. This sensitivity makes coulometry the definitive method for verifying ultra-dry polyester pellets prior to melt compounding or injection molding.
Base additions maintain electrolyte balance. The stoichiometric capacity of the anolyte depends on maintaining appropriate pH levels between five and seven. Acidic drift slows reaction kinetics, while basic drift triggers side reactions that consume iodine independently of water content.
Maintaining clean electrode surfaces and fresh anolyte solution prevents reagent depletion during continuous sampling runs.
Oven
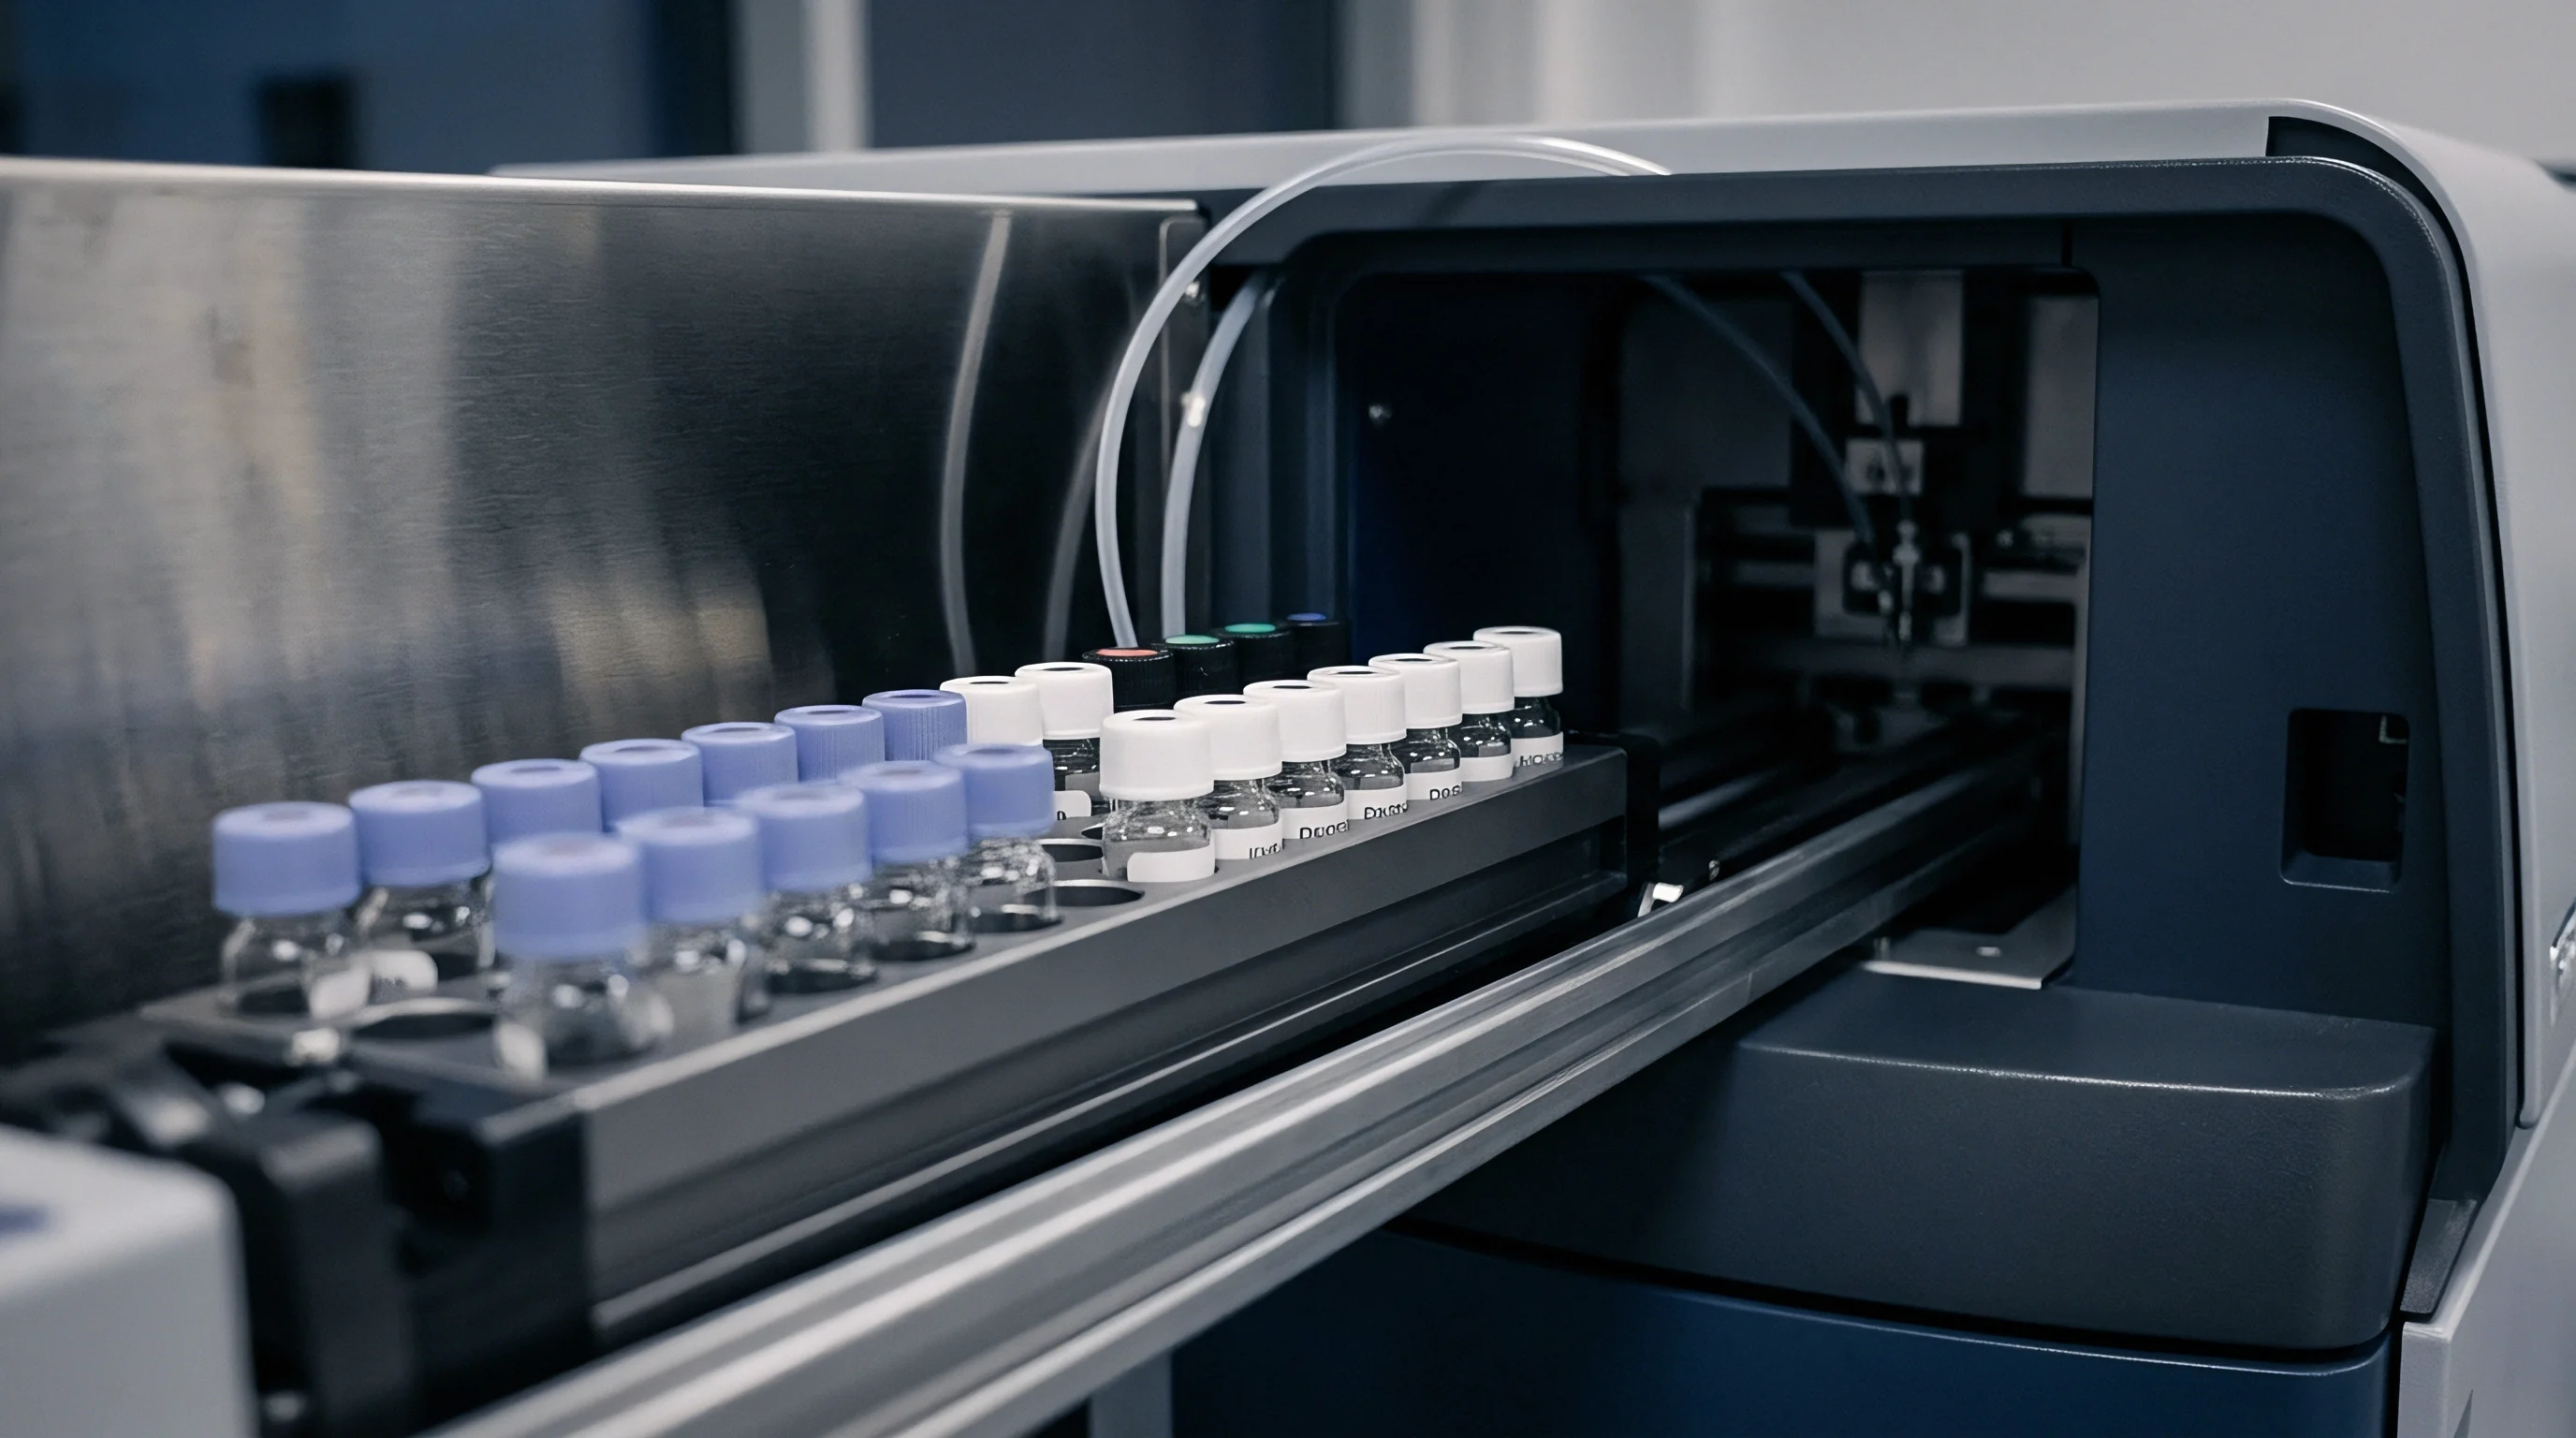
Solid polyester resins cannot undergo direct titration due to insolubility in standard Karl Fischer anolyte formulations. Polyester pellets insoluble in alcohols at ambient temperatures require thermal extraction to liberate trapped moisture without dissolving the polymer matrix. A thermal vaporization unit combined with a coulometric cell isolates the sample, heating pellets inside a sealed furnace while a dry carrier gas transfers evaporated water directly into the titration reagent.

Thermal Evaporation Test Parameters
ISO 15512 Method C mandates heating temperature zones calibrated to resin melting points. The sample furnace must heat pellets above their glass transition temperature to promote rapid diffusion of absorbed moisture from the pellet interior to the surface. Heating must remain below the thermal decomposition temperature of the polymer to prevent chemical breakdown.
Nitrogen purges the heating chamber.
Oven seals prevent ambient infiltration. The transfer line connecting the thermal furnace to the titration cell requires constant heating, typically held between one hundred ten and one hundred thirty degrees Celsius, to prevent vaporized water from condensing along the internal walls of the tubing prior to entering the titration cell.
| Resin Type | Furnace Temperature Range | Recommended Sample Mass | Carrier Gas Flow Rate | Test Duration |
|---|---|---|---|---|
| Polyethylene Terephthalate | 170 °C to 185 °C | 1.0 g to 3.0 g | 80 mL/min to 100 mL/min | 10 min to 15 min |
| Polybutylene Terephthalate | 160 °C to 175 °C | 2.0 g to 4.0 g | 70 mL/min to 90 mL/min | |
| Polyethylene Naphthalate | 180 °C to 200 °C | 1.0 g to 2.0 g | 80 mL/min to 100 mL/min | 12 min to 18 min |
| Glycol Modified PET | 150 °C to 165 °C | 2.0 g to 5.0 g | 60 mL/min to 80 mL/min | 8 min to 12 min |
Sample Transfer Sequence
Minimizing atmospheric exposure protects resin pellets during loading into heating chambers. Standard testing procedures demand rapid handling sequences to prevent ambient humidity absorption on pellet surfaces during sample transfer.
- Purge the empty glass sample vial or quartz boat with dry nitrogen gas for at least sixty seconds inside the conditioning chamber.
- Weigh the purged empty container on an analytical balance with a readability of 0.1 milligrams and record the tare weight.
- Transfer approximately two grams of dry polyester pellets directly from the sealed moisture-proof sampling bag into the container.
- Seal the container immediately using a PTFE-lined silicone septum cap to isolate pellets from ambient humidity.
- Record the gross mass to determine precise net sample weight prior to insertion into the heating furnace.
- Place the sealed container into the thermal furnace drive mechanism and initiate the carrier gas flow purge cycle.
- Lower the sample needle mechanism into the vial septum, establishing an uninterrupted gas path through the cell.
- Start the electrochemical current integration timer once carrier gas flow stabilizes and initial baseline drift returns to pre-injection levels.
A transfer tube held below the furnace setpoint traps vapor before measurement occurs.
Calculated moisture updates batch records. Incomplete extraction occurs when heating times fall short of the required diffusion period, resulting in artificially low moisture readings that mask true polymer degradation risks.
Insufficient heating leaves bound moisture inside the polymer core, causing processing lines to run wet resin and yield brittle molded parts that fail impact testing.
Side
Secondary chemical reactions at elevated temperatures generate additional moisture that distorts analytical results. Thermoplastic polyesters undergo thermal degradation and continued esterification when exposed to heat inside the furnace chamber. Understanding these side reactions enables analysts to separate absorbed physical water from chemically generated water.
Thermal Decomposition Mechanisms
Heating PET or PBT resins near two hundred degrees Celsius promotes ester bond cleavage. Uncapped carboxylic acid end groups react with hydroxyl end groups in residual polycondensation reactions, releasing stoichiometric water as a byproduct. High temperatures trigger polymer degradation.
Excessive heating generates stoichiometric water. This chemically generated water evaporates into the carrier gas stream, passing into the titration cell and registering as absorbed moisture. The resulting values falsely inflate the calculated pellet moisture level, leading operators to over-dry resin batches or reject dry polymer shipments unnecessarily.
ISO 15512 Method C specifies carrier gas moisture levels below two parts per million to prevent continuous baseline oxidation.
Should Nitrogen Carrier Gas Flow Rates Exceed One Hundred Milliliters per Minute?
Gas velocity directly controls the transit time of liberated moisture from the furnace into the titration chamber. Excessively high carrier gas flow rates push volatile compounds into the titration cell faster than the electrochemical system can oxidize generated water, leading to localized concentration spikes and incomplete titration end points. Conversely, low flow rates permit moisture accumulation inside cold spots along the delivery tubing.
Optimal carrier gas velocities sit between sixty and one hundred milliliters per minute. Operating within this window ensures complete sweep efficiency while preventing volatile organic interferences from overwhelming the anolyte solution.
- Acetaldehyde Volatilization occurs during thermal degradation of PET, introducing volatile aldehydes into the cell that react with methanol solvents to produce secondary water.
- Polymer End Group Esterification generates stoichiometric water when furnace temperatures exceed resin stability limits during extended heating cycles.
- Additive Volatilization releases low molecular weight esters, plasticizers, or flame retardants that coat cell electrodes and decrease electrochemical sensitivity.
- Carrier Gas Contamination introduces external atmospheric humidity into the sample chamber when supply lines lack active desiccating gas purifiers.
Whether keto-enol tautomerization in modified glycol copolymers contributes significant interfering water at lower temperature thresholds remains unresolved across current analytical literature.
Variance
Analytical repeatability depends on quantifying background ingress from carrier gas streams and glass joints. Coulometric titrators constantly register small amounts of ambient moisture leaking into the titration vessel. Drift rates exceed target thresholds when seals degrade or gas lines absorb ambient water, compromising measurement accuracy for low-moisture resins.
Calibration Standard Selection
Sodium tartrate dihydrate contains a fixed chemical water content of fifteen point sixty-six percent by weight. Solid calibration standards provide stable reference points for validating oven extraction efficiency and electrochemical cell response. Liquid water standards injected directly into the cell verify cell electrolysis factor accuracy, whereas solid standards verify the complete extraction path including furnace delivery lines.
| Moisture Level Band | Target Content Range | Repeatability Standard Deviation | Reproducibility Standard Deviation |
|---|---|---|---|
| Ultra Low Moisture | 10 ppm to 30 ppm | 1.8 ppm | 4.2 ppm |
| Standard Dry Moisture | 31 ppm to 100 ppm | 3.5 ppm | 7.8 ppm |
| Slightly Wet Moisture | 101 ppm to 300 ppm | 8.1 ppm | 15.4 ppm |
Drift Control Routine
Baseline subtraction accounts for residual environmental ingress entering the system continuously. Titrators measure baseline drift rates prior to sample injection, subtracting this background microgram-per-minute baseline value from total measured water throughout the titration duration.
Atmospheric exposure during pellet sample transfer inflates measured water content by ten parts per million for every thirty seconds of open air handling.
Pellet transport introduces room air. Effective quality control routines mandate systematic checks to isolate background instrument noise from true polymer moisture content.
- Gas Line Purging requires continuous flushing of nitrogen carrier lines for thirty minutes prior to running daily calibration standards.
- Septum Inspection demands replacing furnace transfer septa after twenty injections to prevent pinhole atmospheric leaks.
- Anolyte Exchange occurs when total accumulated water in the titration vessel reaches one hundred milligrams or when drift stays above fifteen micrograms per minute.
- Baseline Drift Audit verifies that vessel background drift stabilizes below five micrograms per minute before loading sample boats.
Resin producers frequently argue that moisture spikes in delivered lots stem entirely from customer storage hopper humidity rather than poor drying before silo loading.
Penalty
Residual moisture in polyester pellets causes immediate hydrolytic degradation during melt extrusion and injection molding. Polymer chains undergo hydrolytic scission. When PET resin enters an injection molding screw at two hundred eighty degrees Celsius with a moisture content of two hundred parts per million, water molecules break ester linkages instantaneously, causing a drop in intrinsic viscosity that destroys structural performance in finished components.
Hydrolytic Chain Scission Economics
Every ester link severed by water molecules during melt processing reduces molecular weight. Intrinsic viscosity drops correlate directly with processing moisture levels. A PET resin entering a preform molding machine with an initial intrinsic viscosity of 0.82 deciliters per gram experiences a drop down to 0.68 deciliters per gram if processed at two hundred parts per million moisture.
Drying reduces hydrolytic scission. Processing resin above fifty parts per million moisture causes top-load failure in packaging containers, environmental stress cracking in automotive PBT connectors, and high rejection rates during quality checks.
| Moisture Level at Ingestion | Intrinsic Viscosity Drop | Part Scrap Rate Percent | Drying Energy Cost | Net Financial Loss |
|---|---|---|---|---|
| 25 ppm (Properly Dried) | 0.01 dL/g | 0.3% | $1,850 | $0 Baseline |
| 50 ppm (Specification Limit) | 0.03 dL/g | 0.8% | $1,420 | $1,100 |
| 120 ppm (Under-Dried) | 0.09 dL/g | 4.5% | $980 | $9,400 |
| 250 ppm (Saturated Pellet) | 0.18 dL/g | 18.2% | $450 | $38,600 |
Dispute Resolution Contract Clauses
Commercial supply agreements define explicit moisture thresholds linked to ISO 15512 Method C protocols. When incoming railcar deliveries test above fifty parts per million moisture upon arrival at a converting plant, formal commercial claim mechanisms activate. Buyers issue rejections based on coulometric certificate of analysis records.
Standard purchasing contracts specifying ISO 15512 Method C with a maximum allowable moisture limit of fifty parts per million convert incoming batch rejections into seller-funded return freight and material replacement.