Characterizing Non Isothermal Viscoelastic Response in Polypropylene Sheet Stretch
Polypropylene sheet stretch requires strict core-to-surface thermal balance near 160C to exploit crystalline strain hardening and prevent wall thinning.
Furnace
Polypropylene sheet thermoforming fails most expensively when the oven bank passes an incoming extruded roll into the forming station with a thermal gradient across its thickness. A core running at 152 degrees Celsius wrapped inside surfaces at 164 degrees Celsius delivers an unstable stretch kinematic under the plug. The semi-crystalline morphology of polypropylene means that within a narrow window of roughly five to eight degrees Celsius below the nominal melting temperature of 165 degrees Celsius, the tensile modulus collapses by two orders of magnitude.
Clamping frames pull unevenly, sag control systems register non-linear droop, and pneumatic prestretch creates localized wall thinning that no downstream tool cooling adjustment can rescue.
Melt flow rate selection establishes the baseline stretch behavior before heating ever begins. Extrusion sheet converters run homopolymer or impact copolymer grades with melt flow rates between 0.5 and 2.0 grams per 10 minutes measured at 230 degrees Celsius under a 2.16-kilogram load according to ISO 1133. Low melt flow rates provide the long polymer relaxation times and high melt strength necessary to prevent catastrophic sheet sag during radiant heating.
High melt strength grades incorporate long-chain branching or multimodal molecular weight distributions. These structural modifications yield strain hardening under biaxial extension, preventing strain localization during deep-draw pocket formation.
A sheet core lagging eight degrees behind the skin doubles wall variation across a deep-draw thermoformed pocket.
Processing windows depend heavily on radiant element tuning and cycle timing. Ceramic infrared heaters, medium-wave quartz emitters, and fast-response carbon heaters deposit energy differently into the polymer thickness. Polypropylene exhibits distinct infrared absorption bands around 3.4, 6.8, and 7.3 micrometers, corresponding to carbon-hydrogen stretching and bending vibrations.
Medium-wave quartz emitters operating between 2.0 and 3.5 micrometers match these absorption bands effectively, generating penetrating volumetric heat. Long-wave ceramic elements heat primarily by surface absorption followed by conductive thermal transport into the core, demanding longer soak times to prevent steep through-thickness thermal gradients.
Tool builders often absorb the blame when molded parts display side-wall banding or optical haze. The press operator adjusts plug timing, vacuum delay, and air blow pressure to correct the flaw. If the extruded sheet possesses an uneven thermal history from the oven, these press adjustments simply shift the thin spot from the corner radius to the floor flange.
Stable processing demands that the incoming polymer sheet arrive at the tool clamping line with an isotropic, characterized viscoelastic state. A supplier unable to verify through-thickness temperature uniformity within positive or negative 1.5 degrees Celsius across the blank delivers unpredictable cycle scrap.
Rheology
Characterizing the non-isothermal viscoelastic behavior of polypropylene sheet requires separating time-dependent viscous flow from elastic recovery across a shifting temperature field. Dynamic mechanical analysis, rotational shear rheometry, and true biaxial extension benches furnish the constitutive data for finite element thermoforming simulations. Solid-state dynamic mechanical analysis conducted per ISO 6721-4 reveals the alpha-relaxation transition occurring between 60 and 120 degrees Celsius.
This relaxation involves chain mobility within the crystalline lamellae, defining the initial softening stage before true melting.
As the temperature enters the alpha-transition zone, crystalline domains slip under mechanical stress. When the sheet reaches forming temperatures between 150 and 160 degrees Celsius for solid-phase sheet forming, or 162 to 168 degrees Celsius for melt-phase forming, the uncoiling of amorphous chains between crystallites dictates the initial stress rise. High-speed biaxial stretch tests demonstrate that the engineering stress versus stretch ratio curve is governed by deformation rate as much as absolute temperature.
Increasing the strain rate from 0.1 per second to 10 per second shifts the true yield point upward by up to 40 percent at an identical test temperature.
Dynamic Modulus across the Melting Window
Storage modulus curves plot the rapid decay of mechanical integrity as melting approaches. The loss modulus peaks near the onset of crystalline disruption, indicating the temperature where viscous dissipation outpaces elastic retention. Rheological characterization using parallel-plate oscillatory shear at 1 Hertz under a nitrogen blanket maps this boundary precisely.
The test requires rapid data acquisition to track the structural transition without thermal degradation of the unstabilized test coupon.
| Temperature (Degrees C) | Storage Modulus G prime (kPa) | Loss Modulus G double prime (kPa) | Loss Factor Tan Delta | Melt Strength (cN) |
|---|---|---|---|---|
| 140 | 145000 | 18200 | 0.126 | 42.5 |
| 148 | 68000 | 12400 | 0.182 | 31.0 |
| 154 | 21000 | 6500 | 0.310 | 18.4 |
| 158 | 4200 | 2100 | 0.500 | 10.2 |
| 162 | 380 | 395 | 1.039 | 4.1 |
| 166 | 12 | 48 | 4.000 | 1.2 |
The crossover point where the loss factor tan delta equals unity marks the transition from predominantly solid viscoelastic response to fluid-like melt behavior. For standard isotactic homopolymer grades, this crossover occurs within a narrow two-degree band around 161.5 degrees Celsius. In contrast, broad molecular weight distribution copolymer resins extend this transition across a span of six to ten degrees Celsius.
This broader transition widens the allowable forming window on the factory floor, mitigating the impact of minor heater zone drifts across continuous production runs.
Equibiaxial Extension Dynamics
Uniaxial tensile testing provides inadequate input data for numerical stretch simulations. During vacuum forming, the sheet experiences equibiaxial extension at the dome apex and planar extension along the wall sections. Dynamic biaxial stretch fixtures grip square specimens with multiple independently actuated hydraulic or servo-electric clamps.
Heating the specimen via high-intensity infrared lamps while translating the grips at programmed velocity profiles generates true stress against true strain data under realistic industrial acceleration rates.
Strain hardening emerges prominently at high stretch ratios when stretching temperatures remain below 160 degrees Celsius. The crystallite fragments act as physical crosslinks, preventing chain slippage and forcing amorphous segments into taut alignments. This strain-hardening behavior stabilizes the wall thickness during rapid drawing.
If the local sheet temperature rises beyond the crystallite melting point, strain hardening disappears. The material then thins uncontrollably at the thinnest section, producing the defect known as necking or blow-out.
Constitutive modeling captures these physical dynamics using hyperelastic and viscoelastic mathematical formulations. The Ogden model, paired with a non-linear viscoelastic Prony series, represents both the large-strain stiffness and time-dependent stress relaxation observed during the stretch sequence. The temperature dependence of the relaxation times follows the Williams-Landel-Ferry equation above the melting point, while an Arrhenius relationship characterizes the response below the onset of crystal breakdown.
Failing to incorporate the cooling rate into these constitutive equations invalidates the simulation results. As the hot sheet moves from the oven to the forming press, ambient radiation and forced convection rapidly chill the exterior. The sheet surface cools at rates between 5 and 15 degrees Celsius per second before tool contact occurs.
A simulation executing an isothermal viscoelastic model underpredicts draw forces by more than 50 percent, skewing tooling stress analysis and yielding inaccurate wall thickness predictions.

Tooling
Tooling design for polypropylene sheet forming accounts for thermal contraction, localized contact cooling, and selective draft angles. Polypropylene exhibits volumetric shrinkage between 1.5 and 2.5 percent, depending on resin crystallinity and nucleating agent content. Semi-crystalline shrinkage varies significantly between the machine direction and transverse direction due to molecular orientation induced during the flat-die sheet extrusion process.
Toolmakers must apply differential shrinkage compensations across the mold geometry: typically 1.8 percent along the extrusion flow direction and 1.4 percent across the transverse direction for standard homopolymer grades.
DIN 16742 Group 140 dictates broad dimensional tolerances unless tool cavity temperatures remain controlled within three degrees Celsius.
Machined 6061-T6 aluminum serves as the standard material for thermoforming molds, offering high thermal conductivity to remove heat rapidly from the shaped part. Cast aluminum tools provide an economical alternative for large, low-cavitation components, though internal porosity can complicate vacuum venting micro-drills. Cooling channels drilled into the aluminum core must pass within 15 millimeters of the cavity surface, maintaining coolant flow rates with Reynolds numbers exceeding 10,000 to ensure fully turbulent heat transfer.
- Cavitation layout sets the initial commercial baseline by balancing total sheet clamp frame width against the maximum allowable extrusion width of the feeding line. Cavity spacing must preserve minimum web bridges of 25 to 35 millimeters to retain structural clamping rigidity during deep forming.
- Syntactic foam plugs reduce localized cooling when the assist plug contacts the sheet prior to vacuum application. Plugs constructed of copolymer syntactic materials with low thermal conductivity prevent sheet freezing, allowing deep material penetration into the cavity floor.
- Perimeter vent geometry prevents air entrapment defects while avoiding surface marking on the part. Micro-vent holes with diameters between 0.35 and 0.50 millimeters exhaust trapped air without allowing molten polypropylene to extrude into the vent apertures under standard vacuum levels of 0.85 bar.
- Trim-in-place integration eliminates part shrinkage variations caused by post-demolding ambient cooling. Progressive cutting dies integrated directly into the forming station cut the perimeter seal flange while the part remains clamped over the water-cooled mold core.
Plug assist mechanics represent the most critical physical interface in the forming station. An unheated aluminum plug pulls heat out of the contacting sheet within 50 milliseconds, immobilizing the polymer and creating a heavy bottom floor with thin side walls. Syntactic foam tooling inserts exhibit a thermal conductivity below 0.15 Watts per meter-Kelvin, ensuring the polymer sheet stretches uniformly around the plug without freezing the contact footprint.
Process cooling rates within the mold govern the development of crystalline spherulites. Rapid quenching against chilled aluminum running at 15 degrees Celsius yields fine spherulites with high optical clarity and superior impact resistance. Slow cooling against a warm mold running at 65 degrees Celsius promotes large spherulitic crystal structures.
These larger spherulites increase tensile modulus and thermal stiffness but severely embrittle corner radii, elevating scrap rates during downstream assembly operations.
Press
Stabilizing a thermoforming press during continuous polypropylene production demands continuous thermal monitoring and cycle repeatability. Cycle time fluctuations as small as 0.3 seconds change the conductive heat dissipation into the sheet clamp rails, shifting the edge-to-center temperature distribution. Modern forming lines utilize multi-zone closed-loop pyrometer arrays to read sheet temperatures at the oven exit.
If the core sheet temperature drops below 158 degrees Celsius, the machine controller triggers an automatic dwell extension in the final heating bank.
Troubleshooting Non-Isothermal Stretch Defects
Defects encountered during tool trials indicate clear breakdowns in thermal conditioning or kinematic timing. The setter must isolate the physical mechanism before adjusting press parameters.
- Corner thinning stems from localized overheating in the sheet blank or an undersized assist plug profile. The molten polymer draws prematurely toward the vacuum holes before the plug finishes its stroke, exhausting material from the structural corners.
- Optical distortion bands appear when the plug assist speed mismatches the vacuum pull rate. If the plug drives through the sheet faster than the relaxation rate of the resin, unrelaxed mechanical shear creates birefringence patterns that appear as cloudy bands under polarized light.
- Flange warpage occurs when the part is stripped from the mold before crystallization completes. If the ejection temperature exceeds 80 degrees Celsius, post-mold crystallization induces differential stress gradients between the inner tool-facing surface and the exposed cavity-side skin.
- Webbing between cavities indicates excessive sheet temperature, insufficient clamping pressure, or tight cavity spacing. The molten polymer sags excessively, causing adjacent cavity draws to merge into folds before seating against the mold walls.
Process Window Qualification
Quantifying the allowable processing window requires evaluating part quality across temperature and strain-rate boundaries. In a representative packaging application forming 1.2-millimeter polypropylene sheet into a 100-millimeter deep container, the operational window spans only a narrow set of thermal and pneumatic conditions. Outside these parameters, mechanical performance declines rapidly.
| Sheet Temperature (Degrees C) | Plug Velocity (mm/s) | Minimum Wall (mm) | Cycle Time (s) | Primary Failure Mode |
|---|---|---|---|---|
| 152 | 150 | 0.21 | 8.2 | High forming tonnage, corner blowout |
| 156 | 250 | 0.34 | 7.6 | Incomplete detail replication |
| 160 | 350 | 0.48 | 7.1 | Stable forming window, zero defect |
| 164 | 350 | 0.38 | 6.8 | Excessive sag, optical haze |
| 168 | 400 | 0.18 | 6.5 | Webbing, excessive bottom thickness |
Operating near 160 degrees Celsius yields maximum wall thickness uniformity and minimizes scrap. Moving the process four degrees higher drops the minimum wall thickness down to 0.38 millimeters due to loss of melt strength. When the sheet drops to 152 degrees Celsius, the machine pneumatic systems struggle to draw the stiff sheet into the tool radii, producing incomplete parts and blown-out corners where local elongation limits are exceeded.
Forming air pressure dynamics interact directly with material elasticity. Applying high-pressure air at 4 to 6 bar immediately after plug stroke completion drives the hot sheet against the aluminum mold cavity, suppressing the relaxation of elastic orientation. This rapid contact cooling preserves the molecular orientation developed during the draw phase, maximizing container top-load crush strength.
Delaying the air application allows viscoelastic stress relaxation to occur, lowering molded residual stresses but reducing the structural rigidity of the finished article.
Resin lot variance frequently compromises the press setup. A fractional melt resin with a broad molecular weight distribution tolerates minor thermal swings across the sheet width. If the purchasing office substitutes an off-spec commodity homopolymer with a narrow molecular weight distribution to reduce resin cost, the allowable temperature window contracts.
The setter must then slow the entire press line to maintain through-thickness thermal saturation, increasing unit manufacturing costs.
Yield
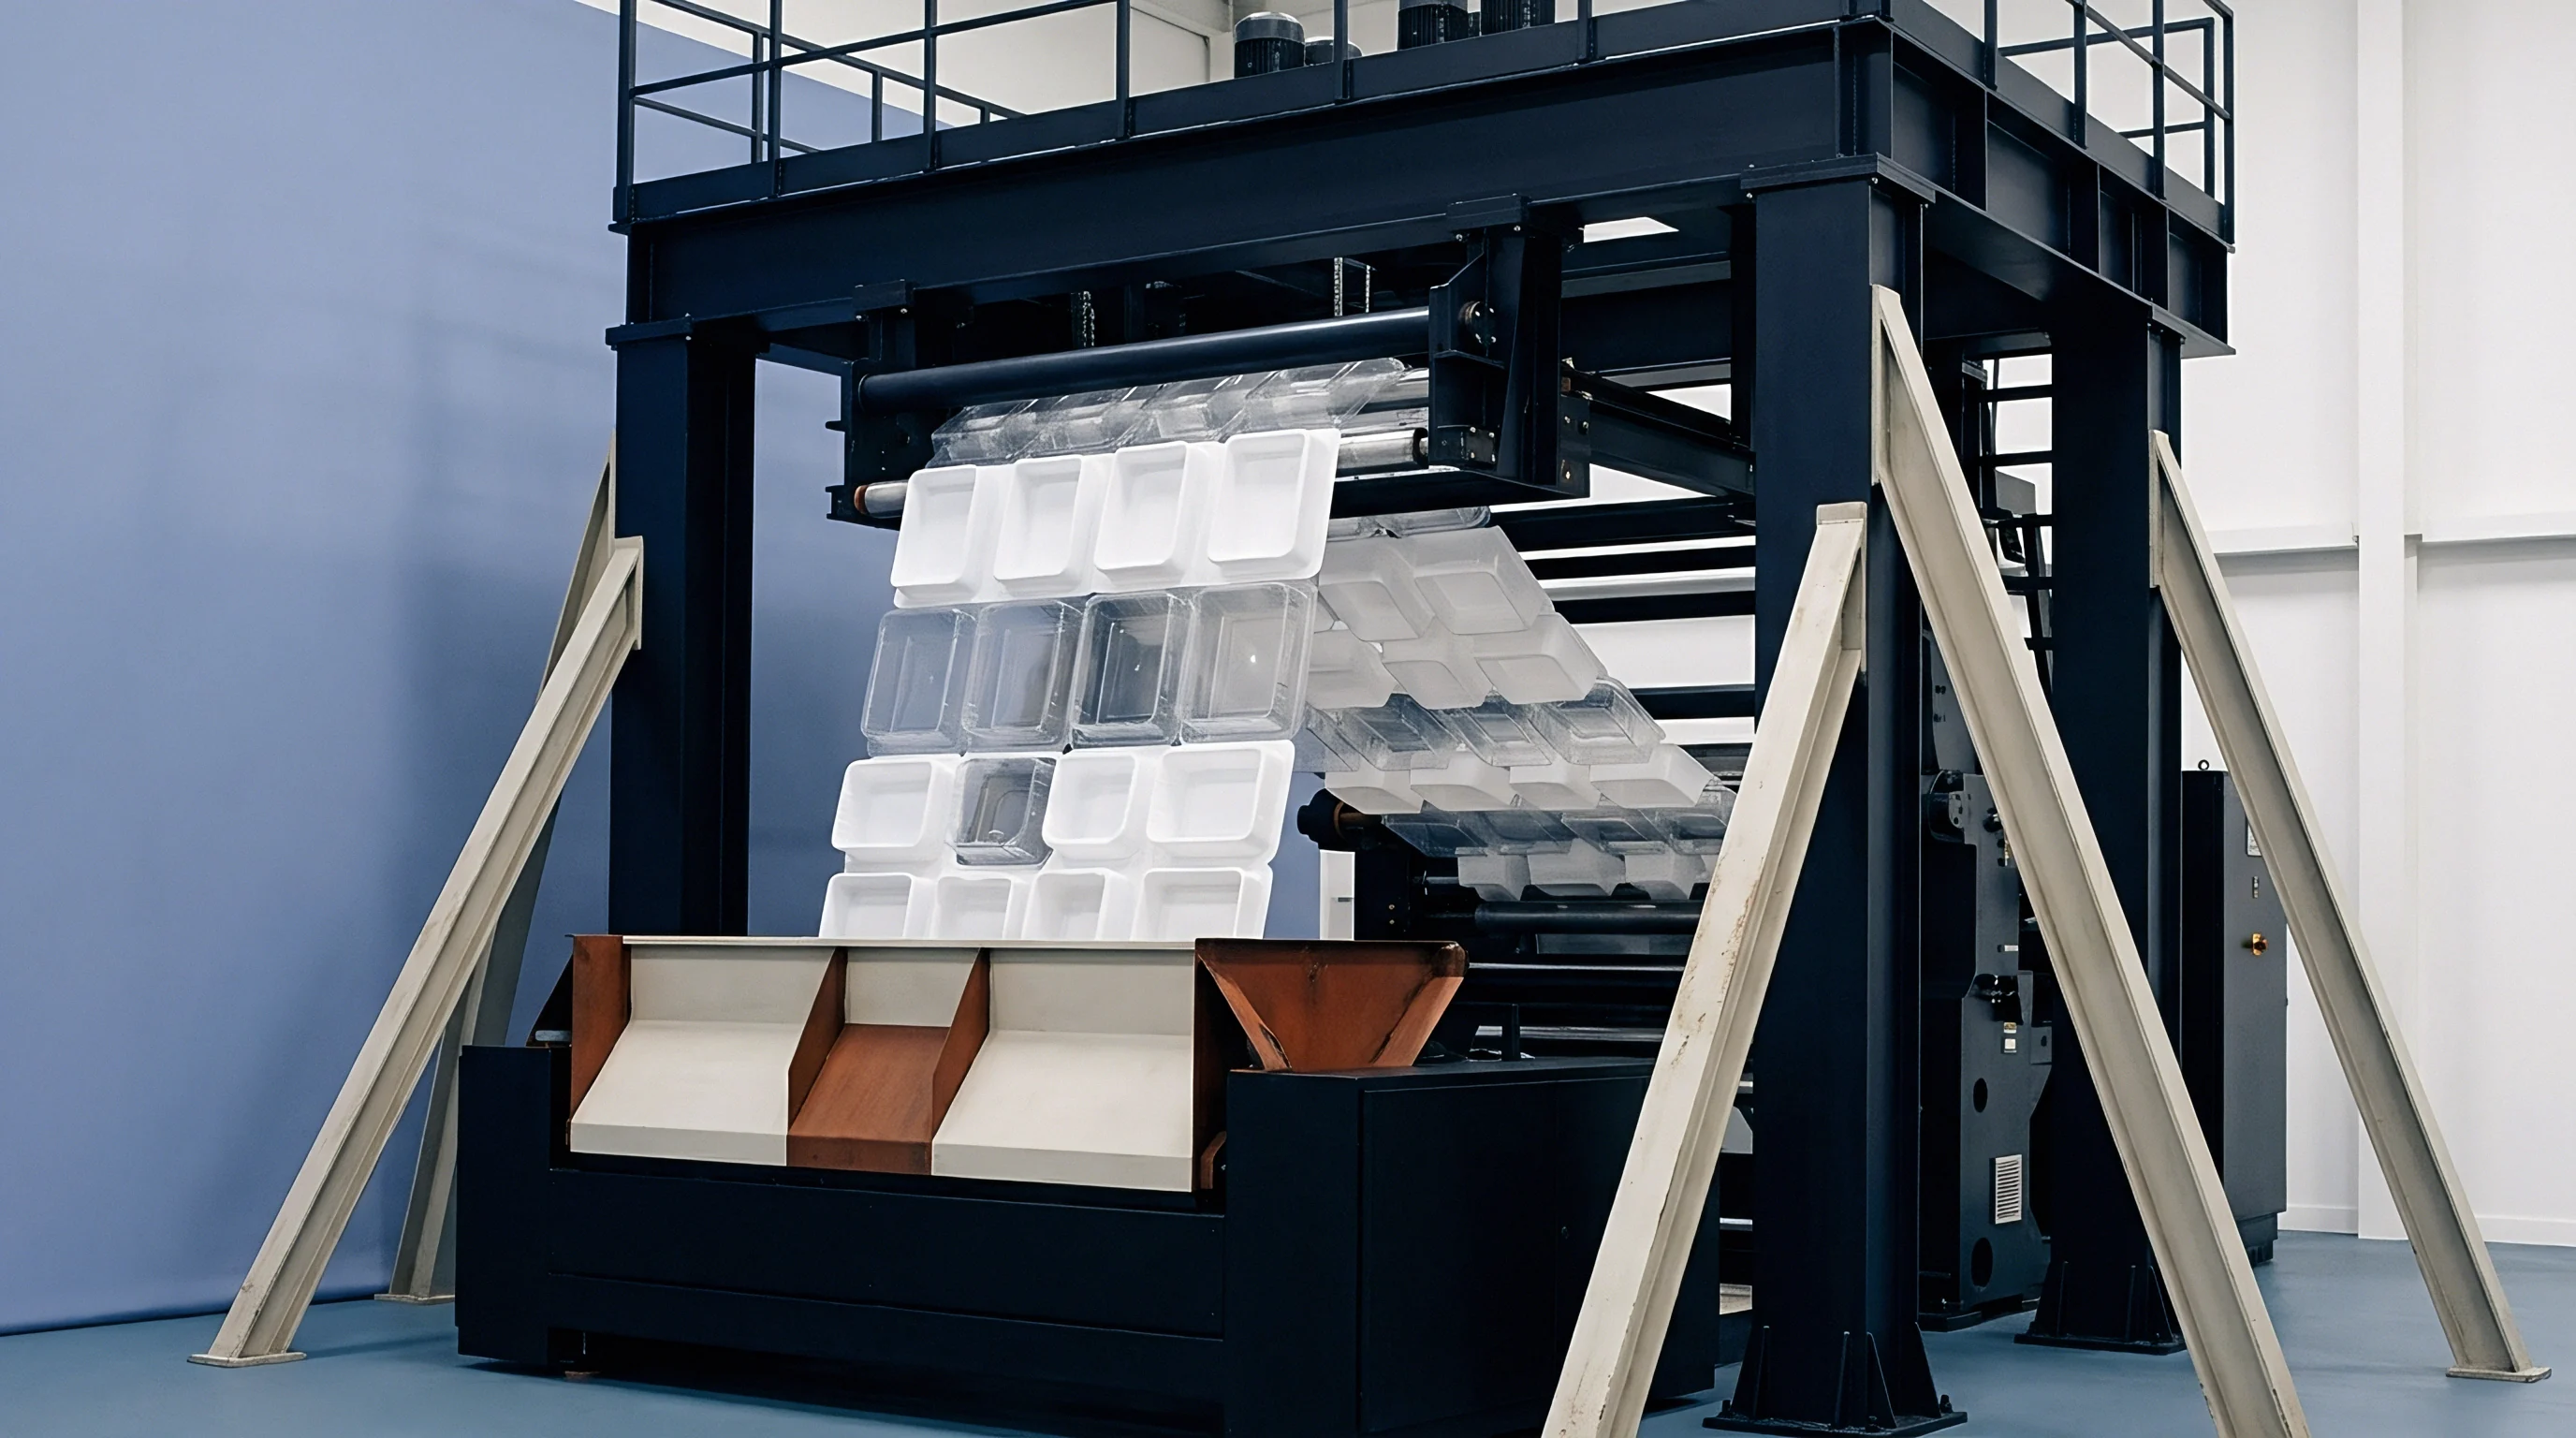
Commercial performance in polypropylene sheet thermoforming hinges on total material efficiency, cycle time amortisation, and scrap reclamation economics. Extrusion sheet lines feed thermoforming equipment either in-line, where the hot extruded sheet runs directly into the forming station, or roll-fed, where master rolls cool to ambient temperature before transport to discrete forming presses. In-line systems conserve massive quantities of thermal energy, utilizing the residual heat from the extrusion barrel to execute the draw.
However, an operational stop on the forming station backs up the continuous extruder within minutes, generating large piles of scrap purge.
A cycle time delay of 0.8 seconds across a sixty-cavity tool erodes processing margins faster than a five-percent raw resin price spike.
Roll-fed processing provides decoupled operational security, allowing the extruder and forming press to operate at independent efficiencies. The significant commercial penalty is the energy required to reheat semi-crystalline polypropylene sheet from ambient temperature back to 160 degrees Celsius. Polypropylene exhibits a high specific heat capacity of approximately 1.9 kiloJoules per kilogram-Kelvin in the solid state, which jumps to roughly 2.7 kiloJoules per kilogram-Kelvin once melted.
Reheating standard sheet rolls accounts for roughly 12 to 18 percent of total machine operating overhead.
Amortisation and Tooling Economics
Tooling capital represents a primary cash expenditure committed long before the first production run ships. A sixty-cavity thermoforming tool incorporating water-cooled 6061-T6 aluminum inserts, beryllium copper thermal pinch trims, and syntactic foam plugs routinely commands a tooling invoice between 140,000 and 220,000 dollars. Amortising this investment over production volume requires precise forecasting of cavitation output and operational press speeds across production shifts.
Consider a practical packaging manufacturing run producing 50,000,000 shallow containers annually from 0.80-millimeter virgin polypropylene sheet. Evaluating tooling cavitation and cycle time parameters highlights the direct connection between press performance and financial returns.
- Machine configuration pairs a 40-cavity tool running at 22 cycles per minute against a 60-cavity tool running at 16 cycles per minute to deliver comparable total output volume.
- Tooling capital cost tallies at 135,000 dollars for the 40-cavity mold versus 195,000 dollars for the 60-cavity system, driven by additional plug actuators and complex internal cooling manifolds.
- Sheet skeletal scrap claims between 30 and 42 percent of the input web weight, depending directly on cavity layout density and perimeter edge-trim clamp allowances.
- Regrind recovery efficiency dictates whether recycled skeletal scrap can be fed directly back into an in-house sheet extrusion co-extrusion core layer at 30 percent ratios without degrading mechanical properties.
The 40-cavity configuration running at high speed generates 52,800 parts per gross production hour. The 60-cavity tool running at lower speed yields 57,600 parts per hour. If the high-cavitation tool suffers from non-isothermal temperature variations across its broad 1100-millimeter web width, edge cavities produce parts with defective wall thicknesses, driving internal reject rates up by 3.5 percent.
Under these conditions, the 60-cavity advantage evaporates entirely, demonstrating that tooling cavitation without thermal control guarantees financial loss.
Resin scrap reclaim systems heavily dictate the final landed cost per thousand parts. Polypropylene degrades via beta-scission under excessive thermal and shear exposure during repeated extrusion cycles. Each extrusion and thermoforming pass lowers the resin weight-average molecular weight, increasing the melt flow rate and reducing melt strength.
Incorporating secondary stabilizer packages containing hindered phenol antioxidants and organic phosphites preserves the melt integrity through up to four consecutive recycling loops, keeping scrap value high and protecting conversion margins.
Protocol
Qualifying high-performance polypropylene sheet for non-isothermal stretch operations requires establishing clear mechanical inspection protocols across converter and customer facilities. Incoming raw material roll stock must carry verified material property certificates confirming melt flow rate tolerances, crystallization peak temperatures, and orientation ratios before release to the production floor. Relying strictly on basic supplier datasheets leaves the converter vulnerable to lot-to-lot thermal processing drifts.
Are Current Analytical Procedures Sufficient?
Standard quality control assays often miss subtle rheological changes that trigger press failures. Melt flow index measurements per ISO 1133 report an aggregate shear viscosity at a single shear stress point, completely ignoring extensional viscosity and melt elasticity. Converters operating high-speed thermoforming machinery run the risk of accepting resin lots that pass basic melt flow criteria but shatter during the biaxial stretch sequence due to uncharacterized shifts in high-molecular-weight fractions.
An effective incoming material inspection protocol implements a multi-tiered test regimen. The qualification sequence establishes whether a production lot possesses the extensional characteristics required for stable non-isothermal forming.
- Differential scanning calorimetry runs per ISO 11357-3 at heating and cooling rates of 10 degrees Celsius per minute. The analysis records the peak melting temperature, onset temperature of melting, crystallization temperature, and total enthalpy of fusion. A shift in crystallization peak temperature exceeding 2.0 degrees Celsius indicates altered nucleation behavior, which changes downstream mold cycle timing.
- High-pressure capillary rheometry evaluates shear viscosity across shear rates from 10 to 10,000 reciprocal seconds, paired with an extensional drawing attachment to determine melt strength and drawability at 190 degrees Celsius. Melt strength values must hold within positive or negative 10 percent of the engineering baseline.
- Free thermal shrinkage testing per ASTM D2732 exposes circular sheet specimens to a silicone oil bath held at 150 degrees Celsius for 60 seconds. Dimensional changes measured in the machine and transverse directions reveal frozen-in orientation stresses induced during sheet extrusion calendar roll quenching.
- High-speed biaxial puncture testing per ISO 6603-2 maps multiaxial impact energy and ductile-to-brittle transition temperatures on pre-stretched sheet samples, validating baseline mechanical toughness under high strain-rate loading.
Procurement agreements must document exact allowable tolerances for sheet thickness and orientation metrics. A thickness variation across the extruded roll exceeding positive or negative 2.5 percent guarantees temperature variations inside the thermoformer heating oven, as thicker sections require longer times to absorb radiant energy. The purchase order must state that rolls exhibiting thickness deviations beyond this limit will be rejected at the loading dock, shifting the commercial cost of extrusion line gauge variation back to the material converter.
Contractual terms should specify that any change in resin catalyst system, co-monomer percentage, or external nucleator additive requires formal written qualification before production roll shipments commence. A supplier changing from a traditional Ziegler-Natta catalyst to a metallocene system yields a resin with narrow molecular weight distribution. Even if the melt flow rate matches nominal specifications, the metallocene-catalyzed grade exhibits sudden thinning during stretch forming, crashing press capability across established tooling setups.
The purchaser can protect project margins by enforcing dynamic mechanical and thermal properties as binding quality acceptance criteria rather than relying on standard commercial trade tolerances. Incorporating clear thermal and viscoelastic parameters into supply contracts prevents expensive press troubleshooting sessions, reduces unexpected tooling rework, and ensures high-speed forming equipment operates at maximum output from the first machine cycle.