Meaning
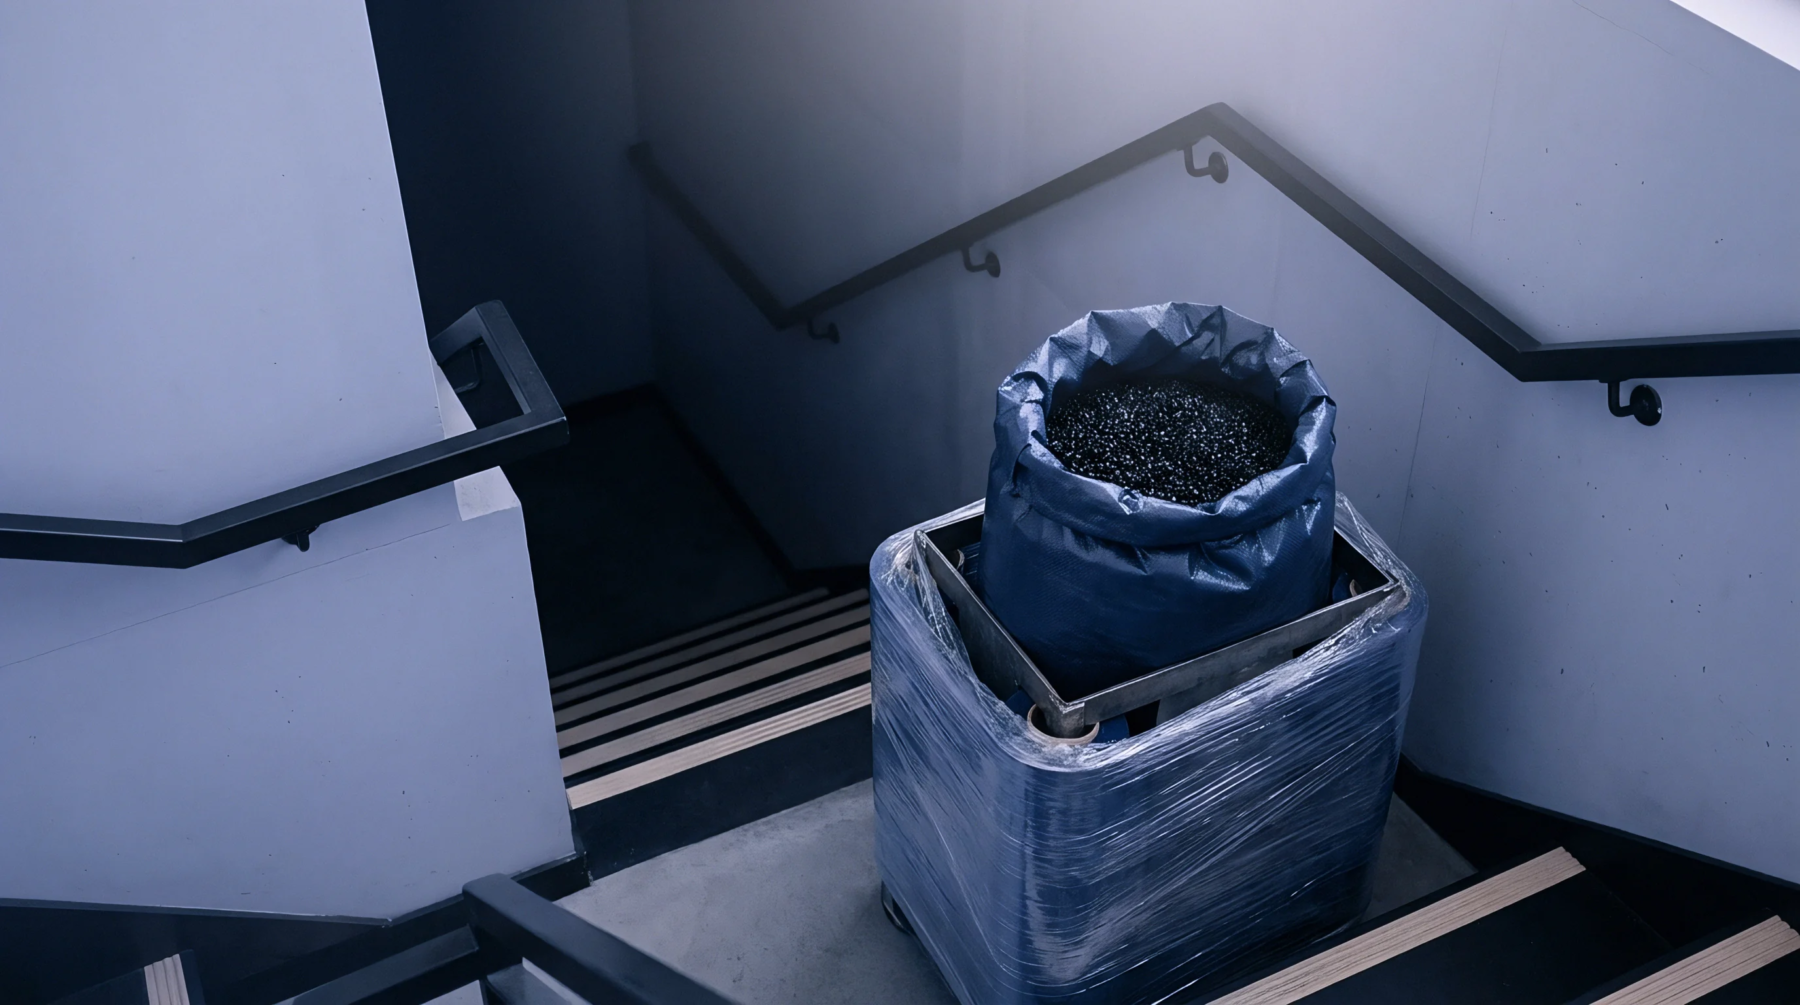
Leftover plastic generated during a manufacturing process that has not been used by a consumer is collected and reprocessed into new compounding streams. Managing post industrial scrap provides a highly consistent, low-contamination source of recycled resin for injection moulders and extruders. This material class governs the economics of in-house recycling and the sourcing of secondary feedstocks for technical parts.
The classification excludes regrind that is generated and directly re-introduced into the same production run on the factory floor.
Purity Assurance
Runoff from start-up purging, sprues, runners, and rejected parts represents a clean source of single-origin polymer. This post industrial scrap has a known thermal history and contains no post-consumer contaminants, such as food residues or paper labels. Compounders use this clean feedstock to produce high-quality recycled resins that closely match the mechanical properties of virgin polymers.
This material helps moulders reduce their raw material costs without risking the structural failure of the finished part.
Pricing Advantage
Purchasing this pre-consumer material is significantly cheaper than sourcing virgin resin, especially for high-volume, lower-performance applications. Incorporating post industrial scrap into a compound lowers the carbon footprint of the product and helps brands meet their environmental goals. The financial savings are realized when the moulder can maintain stable process cycles and avoid the contamination issues that cause mold damage.
This balance of cost and reliability makes it a preferred choice for industrial pallets, crates, and automotive brackets.
Polymer Dilution
Reprocessing this scrap degrades the polymer chains slightly each time it is exposed to the heat of the injection barrel. If the percentage of post industrial scrap in the melt is too high, the resin will show a higher melt flow index and lower impact strength. Moulders must limit the blend ratio to ensure that the material can hold the required tolerances across a long production run.
Testing the melt flow and mechanical properties of each batch helps prevent variations that cause flash or short shots on the moulding line.