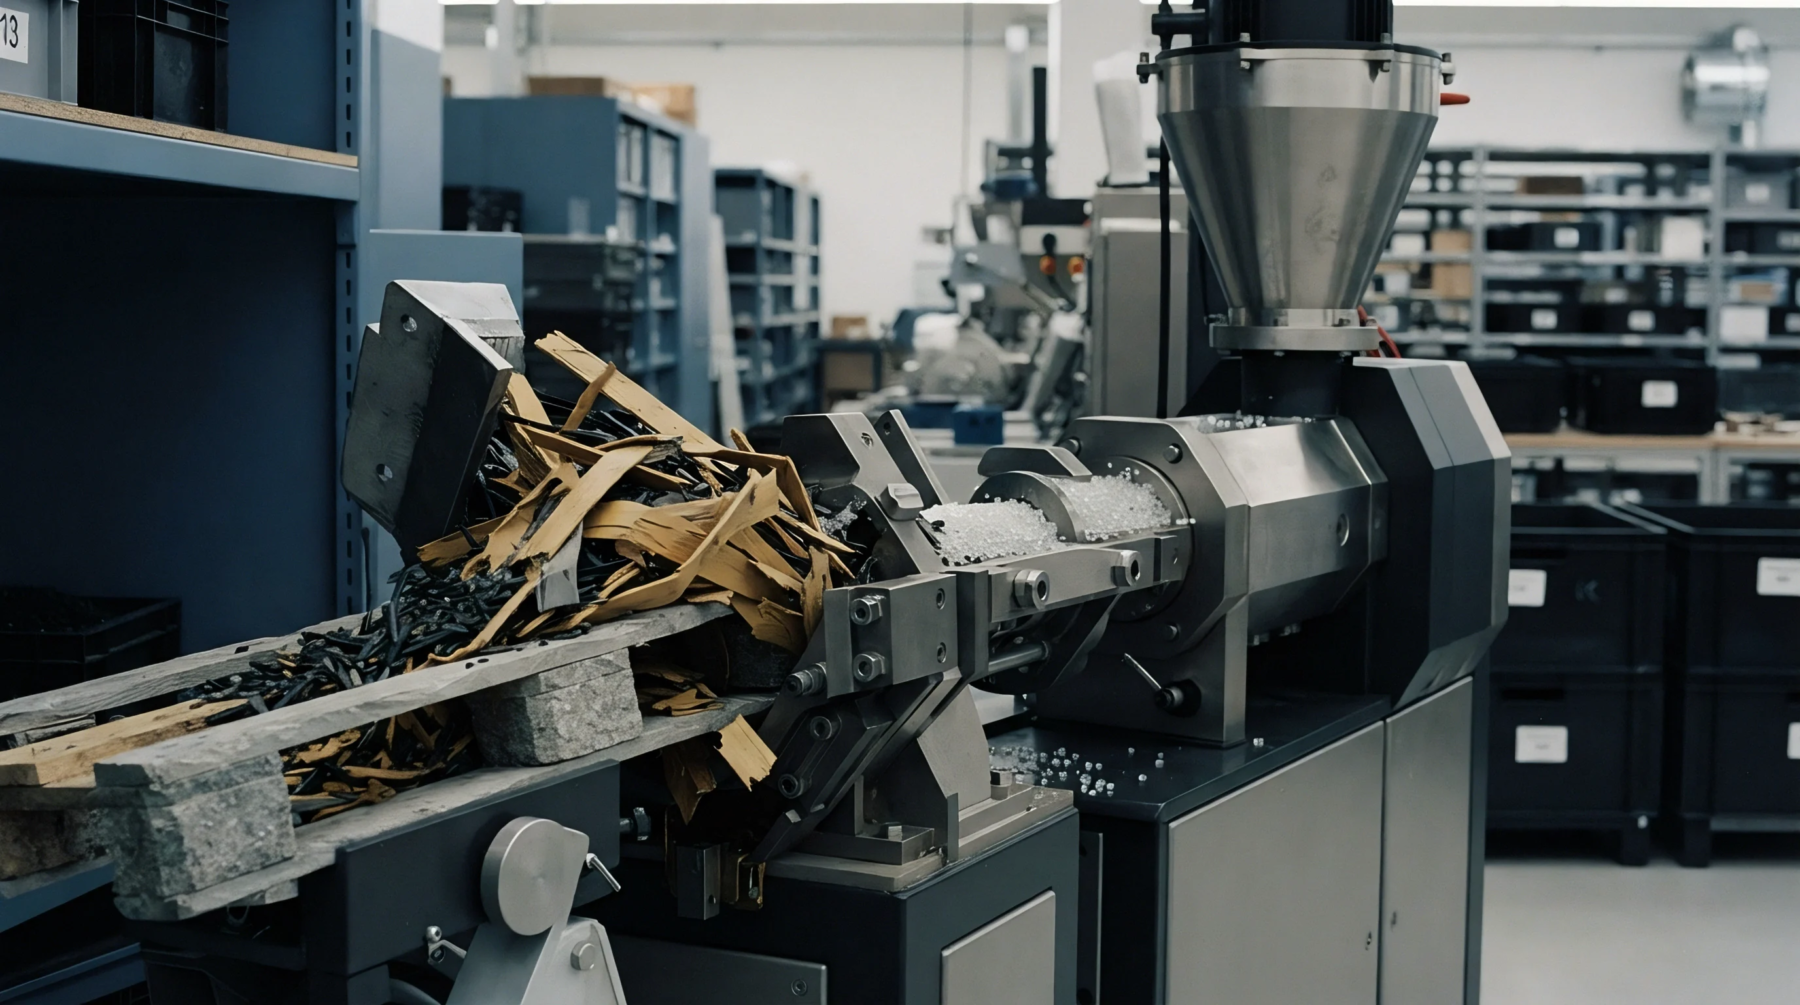
Recycled Content Claims Priced into a Packaging Tax Line
Recycled content tax claims require lot-specific EN 15343 audit trails and migration reports to withstand customs audits and avoid retroactive landed tax liabilities.
Post-consumer material serves as a feedstock classification for plastic manufacturers requiring recycled streams derived from end-of-life products rather than industrial scrap. This pcr resin represents polymer pellets processed from plastic items gathered through municipal collection or retail return programs. The classification covers materials undergoing sorting, washing and shredding before extrusion into usable molding stock.
Boundary conditions dictate that the material remains excluded from categories containing pre-consumer factory waste or virgin feedstock. Physical consistency dictates the performance metrics of the output.
Feedstock variability creates the primary constraint for molders utilizing this recycled stream within their production cycle. Chemical chains break during initial use and subsequent heat exposure, causing the molecular weight to drift compared to virgin equivalents. Process engineers often observe fluctuations in melt flow rate when high percentages of the material enter the extruder.
Consistency depends on the quality of the wash phase and the effectiveness of density-based sorting methods. Excessive contaminants lead to brittle molded parts or surface blemishes during cooling cycles. Injection pressure remains the primary tool for mitigating viscosity changes across distinct lots.
Tooling geometry must accommodate a wider tolerance for these variations if a manufacturer plans to increase the recycled content percentage.
Production costs rise when the intrinsic properties of the material require slower injection speeds or higher clamp force to fill mold cavities effectively. Moulders verify the quality by checking the color match and impurity level against a defined standard before starting a long run. Regrind economics shift when the inclusion of this material demands additional stabilizer additives to counteract thermal degradation.
Virgin supply chains operate with predictable degradation curves, whereas recycled polymers present a moving target for thermodynamic stability. Excess heating during the barrel dwell time increases the rate of molecular chain scission in the melt. Proper temperature control minimizes the risk of charring or localized burning within the nozzle.
High-shear zones in the runner system create a demand for gate sizing that accounts for the irregular flow behavior of mixed polymer streams.
Market price fluctuates based on the availability of clean post-consumer plastic waste and the energy requirements for purification. Downstream processors pay for the testing burden associated with certifying the recycled content for regulated packaging standards. Virgin resins provide a baseline for cost, yet they fail to meet the sustainability mandates currently driving corporate procurement.
Procurement departments manage this gap by balancing the necessity of recycled volume with the technical reality of lower part durability. Suppliers define the quality floor based on the percentage of contamination allowed in each shipment. Contract specifications detail the maximum variance in melt index to prevent equipment shutdowns.
Successful conversion relies on the calibration of machine settings to the specific viscosity profile of the current lot. Consistent resin quality remains the limiting factor for scaling the adoption of circular materials in rigid packaging production.
Recycled content tax claims require lot-specific EN 15343 audit trails and migration reports to withstand customs audits and avoid retroactive landed tax liabilities.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.