Analytical Chemistry Procedures for Verifying Chemically Recycled Content in Polymers
Verify chemically recycled polymers via mass balance audit files, as steam cracking renders circular and virgin fossil hydrocarbons analytically identical.
Furnace
Analytical proof of chemically recycled content in polymers depends on a physical boundary that separates post-consumer waste inputs from fossil naphtha before synthesis ever starts. Most advanced recycling routes run through pyrolysis or gasification units, converting mixed polyolefin fractions into synthetic crude oil, cracking this oil into standard monomers such as ethylene and propylene, and polymerizing those monomers on identical industrial lines. The resultant macromolecules contain identical chain architectures, end groups, and comonomer distributions as virgin material derived directly from fossil reservoirs.
Standard polymer characterization tools like gel permeation chromatography, differential scanning calorimetry, and nuclear magnetic resonance spectroscopy confirm the polymer’s specification while remaining blind to its molecular origin. Direct material attribution by spectroscopy is chemically impossible once the recycled feedstock passes through a thermal steam cracker.
Nuclear analytical procedures solve this blind spot when recycled polymers originate from biogenic packaging or agricultural plastics. Carbon-14 radiocarbon dating under ASTM D6866 or EN 16640 measures the decay of unstable carbon-14 isotopes against stable carbon-12 and carbon-13 baselines. Living biomass maintains a contemporary atmospheric fraction of approximately 1.2 x 10^-12 carbon-14 per carbon-12, yielding an activity of roughly 14 disintegrations per minute per gram of carbon.
Fossil-derived hydrocarbons reside underground across geological timescales exceeding ten half-lives of carbon-14, which sits at 5,730 years, depleting all measurable radiocarbon activity. When a pyrolysis facility converts mixed bio-based waste or blends post-consumer municipal fractions containing biogenic cellulose and paper fiber into crackable waxes, the down-stream polyolefin retains a definitive radiometric signature.
Analytical chemists burn the finished polymer pellet in an oxygen combustion bomb or elemental analyzer furnace to produce pure carbon dioxide gas. The laboratory purifies this gas through liquid nitrogen traps, graphitizes the carbon over iron or cobalt powder catalysts at 600 degrees Celsius, and presses the resulting graphite into target cathodes for Accelerator Mass Spectrometry (AMS). High-voltage electrostatic acceleration separates carbon isotopes by mass, deflecting carbon-12 and carbon-13 into Faraday cups while carbon-14 ions pass through a gas stripper into a solid-state detector.
AMS quantifies total bio-based carbon with an analytical detection limit of 0.1 percent modern carbon (pMC) and an absolute measurement uncertainty of plus or minus 0.5 percent.
AMS quantification measures down to 0.1 percent modern carbon under ASTM D6866 Method B.
AMS testing provides zero analytical signal for polymers derived strictly from post-consumer fossil plastics like discarded polyethylene gas pipes or polypropylene battery cases. A pyrolysis oil refined entirely from fossil polyolefins yields precisely 0.00 pMC, registering the identical dead-carbon baseline as standard paraffinic feeds. Radiocarbon measurements confirm bio-content rather than circular fossil content.
A buyer holding an AMS test certificate for a chemically recycled polypropylene article can verify modern carbon inputs, but the certificate provides zero evidentiary support for post-consumer fossil plastic origins. Misinterpreting zero carbon-14 activity as proof of virgin origin exposes purchasing teams to severe verification deficits, because fully circular fossil polymer and virgin fossil polymer share identical zero-activity signatures.
ASTM D6866 Method B governs graphite AMS analysis, requiring rigorous reporting of fractionation corrections using in-line delta carbon-13 isotope ratios measured relative to the Vienna Pee Dee Belemnite (VPDB) standard. Without carbon-13 fractionation corrections, thermal processing during cracking, distillation, and polymerization artificially shifts isotopic distributions by 1 to 2 permil, which skews calculated bio-based fractions by up to 3 percent. Laboratories documenting test compliance report both the raw fraction modern (Fm) and the final bio-based carbon content calculated against the atmospheric reference standard specified in the regulations for the shipping year.
Buyers handling circular biopolymers incorporate these precise isotope calibration standards directly into purchasing specifications to prevent misattribution audits.
The unresolved industrial tension centers on whether customs and regulatory authorities will formally accept isotope-ratio tracking as sufficient legal evidence of circularity in the absence of co-processed fossil tracers.
Cracking
Secondary chemical markers generated during high-temperature cracking cycles offer an alternative path to establish recycled feedstock utilization. Pyrolysis oil derived from unsorted municipal post-consumer plastic contains a distinct profile of chemical impurities that are absent from refined virgin petroleum naphtha. These impurities include chlorinated alkanes, organonitrogen residues, oxygenated aromatic compounds, conjugated dienes, and legacy additives.
High-temperature steam crackers cannot tolerate excessive levels of these compounds due to severe equipment corrosion, catalyst poisoning, and coking inside the furnace coils. Commercial plants therefore blend pyrolysis wax or crude pyrolysis oil into virgin petroleum naphtha at ratios rarely exceeding 5 to 20 percent by volume before cracking.
Advanced thermal desorbers coupled to two-dimensional gas chromatography time-of-flight mass spectrometry (GCxGC-TOFMS) resolve the complex chemical background of circular feedstocks. In this configuration, a non-polar first-dimension capillary column separates volatile and semi-volatile compounds by boiling point, while a polar second-dimension column separates the effluent by polarity across short modulation periods between 2 and 6 seconds. Pyrolysis oil samples display characteristic compound classes: homologous series of alpha,omega-dienes alongside standard alpha-olefins and n-alkanes, high concentrations of substituted cyclopentadienes, and halogenated decomposition byproducts originating from flame-retarded electronics scrap or polyvinyl chloride contamination.
Tracing Pyrolysis Fingerprints into Monomer Feeds
Downstream fractional distillation strips most heavy heteroatomic molecules from the primary light olefin cuts. Ethylene and propylene fractions sent to the polymerization reactor undergo catalytic hydrotreating and deep refrigeration to achieve polymer-grade purities above 99.95 percent. Heteroatom-containing fragments, such as organic chlorides, nitriles, and silicones from polydimethylsiloxane defoamers, slip through separation trains at parts-per-billion or low parts-per-million levels.
Analytical chemists screen the monomer feed and finished polymer pellets using inductively coupled plasma mass spectrometry (ICP-MS) following closed-vessel microwave acid digestion to detect these inorganic signatures.
Volatile organic chlorides such as chloroethane, 1,2-dichloroethane, and chlorobenzene represent primary trace impurities in circular ethylene feeds. Standard testing utilizes gas chromatography equipped with an Atomic Emission Detector (GC-AED) or an electrolytic conductivity detector (ELCD) operating under ASTM D5884 parameters. Virgin polymerization feeds maintain organic chlorine concentrations below the quantification limit of 0.1 milligrams per kilogram.
Finished pellets processed from pyrolysis streams frequently retain measurable organic chlorine levels between 0.3 and 1.8 milligrams per kilogram, alongside elevated trace silicon values from thermal rubber degradation. The presence of these trace elements provides strong qualitative evidence of chemically recycled feedstock processing within the synthesis plant.
| Analytical Parameter | Virgin Petroleum Naphtha | Crude Plastic Pyrolysis Oil | Hydrotreated Pyrolysis Blend (10%) | Test Protocol |
|---|---|---|---|---|
| Total Chlorine (mg/kg) | Below 0.5 | 50.0 to 1,200.0 | 1.5 to 8.0 | ASTM D7536 / XRF |
| Total Nitrogen (mg/kg) | Below 1.0 | 150.0 to 2,500.0 | 5.0 to 35.0 | ASTM D4629 / Boat Combustion |
| Silicon Content (mg/kg) | Below 0.1 | 10.0 to 180.0 | 0.5 to 4.2 | ASTM D5185 / ICP-OES |
| Conjugated Dienes (wt%) | Below 0.05 | 2.50 to 8.50 | 0.10 to 0.45 | UOP 326 / Maleic Anhydride |
| Heavy Metals: Pb, Cd (ug/kg) | Below 5.0 | 50.0 to 850.0 | Below 10.0 | EN ISO 17294-2 / ICP-MS |
The physical challenge of relying entirely on trace impurity markers rests in modern purification engineering. Refineries employ guard beds containing activated alumina, molecular sieves, and zinc oxide absorbents alongside intensive multi-stage catalytic hydrodechlorination reactors. These purification trains reduce organic chlorine, sulfur, and nitrogen concentrations in circular pyrolysis oil down to levels that match virgin petroleum stocks.
When a petrochemical producer operates state-of-the-art hydrotreatment facilities, the chemical fingerprint of the recycled input disappears completely prior to furnace injection. The absence of pyrolysis impurities in the finished polymer does not prove the absence of chemically recycled content.
Operating a cracker on unrefined pyrolysis blends without adequate hydrotreatment triggers rapid catalyst deactivation, which voids the cracker’s operational efficiency guarantees within weeks.
Taggant
The analytical dead end caused by cracking high-purity recycled hydrocarbons has prompted the development of deliberate molecular taggants. When physical recycling leaves visual or structural signatures, chemical recycling requires artificial identity carriers if direct measurement in the finished article remains a legal requirement. Chemical tagging procedures introduce an engineered, chemically inert molecule into the post-consumer feedstock stream immediately prior to depolymerization or pyrolysis.
The taggant molecule must survive extreme thermal cracking temperatures, acidic catalyst exposures, and subsequent fractional distillation stages without breaking down, or it must cleanly partition into specific monomer fractions at predictable distribution coefficients.
Deuterated hydrocarbons, perfluorinated tracers, and high-stability fluorophores represent common marker chemistries tested for circular polymer tracking. Heavy isotope tracing uses fully or partially deuterated alkanes, such as deuterated dodecane (C12D26) or deuterated benzene (C6D6). These molecules behave almost identically to normal hydrocarbon feeds during fluid transport and mixing, yet their elevated mass-to-charge ratios separate cleanly under Selected Ion Monitoring Gas Chromatography-Mass Spectrometry (GC-MS-SIM).
A dosing unit introduces the deuterated tracer into the post-consumer pyrolysis oil tank at calibrated target concentrations, typically between 10 and 50 parts per million. As the crude oil processes through the cracking furnace, the C-D bonds exhibit slightly higher thermal bond dissociation energy than conventional C-H bonds, preserving a predictable mass fraction of deuterated fragments into downstream propylene or ethylene cuts.

What Analytical Limits Constrain Molecular Tracers?
Direct chemical tagging faces severe regulatory and analytical limitations when applied to food-contact polymers. Any synthetic marker introduced into a circular plastics stream ends up distributed throughout the final article matrix. Under European Union Regulation (EU) 10/2011, any chemical substance present in a plastic material intended for food contact must appear on the positive list of authorized substances in Annex I, or meet the non-detectable migration limit of 0.01 milligrams per kilogram established for unauthorized non-carcinogenic substances behind a functional barrier.
Most persistent tracer chemistries lack positive food-contact authorizations. If an unauthorized industrial taggant migrates into food simulants above 10 parts per billion, the finished packaging breaches compliance.
Surface-enhanced Raman scattering (SERS) taggants and micro-encapsulated inorganic nanoparticles provide an alternative dosing pathway for depolymerization recycling, particularly in closed-loop polycondensation systems for polyethylene terephthalate (PET) and polyamide (PA). Rather than tagging the liquid feed before cracking, these systems dose rare-earth inorganic oxides, such as yttrium-doped lanthanide compounds, directly into the purified bis(2-hydroxyethyl) terephthalate (BHET) monomer prior to melt repolymerization. These ceramic nano-taggants survive polymerization conditions exceeding 280 degrees Celsius and vacuum levels below 1 millibar without degrading.
- Baseline polymer screening confirms the natural matrix is free from interfering background elements through high-resolution inductively coupled plasma mass spectrometry using a triple-quadrupole analyzer (ICP-QQQ).
- Solvent dissolution breaks down the PET matrix via hexafluoroisopropanol (HFIP) and dichloromethane extraction to isolate the inorganic suspended fraction from the organic polymer chains.
- Laser-induced breakdown spectroscopy quantifies the elemental ratios of the rare-earth metals inside the polymer pellet with an optical emission resolution under 0.05 nanometers.
- Spectral deconvolution matches emission intensity against established calibration curves to calculate the mass fraction of tagged recycled content in the batch down to 1.0 weight percent.
Substances migrating behind a functional barrier cannot exceed 0.01 milligrams per kilogram under Regulation (EU) 10/2011.
Inorganic taggants added at the monomer stage avoid cracker destruction, but they face pushback from industrial recycling associations. Introducing foreign metal species into polymer loops complicates subsequent post-consumer mechanical recycling cycles. Accumulating inorganic oxides across multiple mechanical cascading loops alters polymer crystallization kinetics, hazes transparent packaging films, and impairs melt filtration meshes.
Chemical markers added to verify chemical recycling can render the material unrecyclable under mechanical processing standards.
The taggant supplier always emphasizes that the tracer remains non-volatile, completely inert, and invisible to food inspection laboratories.
Monomer
Solvolysis, glycolysis, and enzymatic depolymerization operate under different chemical rules than pyrolysis, breaking heteroatom bonds in condensation polymers without cracking the hydrocarbon backbone. Polyethylene terephthalate, polyamides, and polyurethanes can be completely deconstructed into their original monomers, such as terephthalic acid (TPA), monoethylene glycol (MEG), bis(2-hydroxyethyl) terephthalate (BHET), caprolactam, or adipic acid. In these systems, analytical verification shifts from the polymer pellet back to the monomer purification stage.
The chemical purity of the regenerated monomer directly dictates whether the resulting resin complies with food-contact migration limits and finished technical tolerances.
Reversed-phase high-performance liquid chromatography coupled to ultraviolet-diode array detection (HPLC-UV/DAD) and electrospray ionization mass spectrometry (LC-ESI-MS) serves as the primary bench method for checking recycled BHET and TPA purity. When post-consumer polyester textiles containing elastane, dyes, and finish oils undergo glycolysis, thermal degradation generates characteristic side products: diethylene glycol esters, 4-carboxybenzaldehyde (4-CBA), oligomeric cyclic esters, and aromatic amine residues from azo dyestuffs. Liquid chromatography resolves these impurities on a C18 stationary phase using an acidified water-to-acetonitrile gradient elution profile at 40 degrees Celsius.
Chromatographic Quantification of Solvolysis Intermediates
During glycolysis of post-consumer PET flakes with zinc acetate catalysts at 190 degrees Celsius, incomplete transesterification leaves dimeric and trimeric glycol-esters in the monomer melt. The analytical protocol must separate monomeric BHET from its secondary side-reaction products, specifically methyl-(2-hydroxyethyl) terephthalate (MHET) and bis(2-hydroxyethyl) ether adducts. Liquid chromatography running with mobile phases buffered with 0.1 percent formic acid provides stable retention time repeatability with baseline separation between BHET and MHET within a 15-minute run window.
Detection at 242 nanometers quantifies monomer concentration against external primary calibration standards spanning 10 to 500 micrograms per milliliter.
| Analyte Molecule | Retention Time (min) | Monitored Wavelength / Ion | LOD (mg/kg) | Typical Recycled Monomer Range |
|---|---|---|---|---|
| Monoethylene Glycol (MEG) | 2.15 | m/z 63.0 + | 0.5 | 0.05 to 0.40 wt% |
| Terephthalic Acid (TPA) | 4.80 | 242 nm / m/z 165.0 – | 0.2 | 0.10 to 1.20 wt% |
| 4-Carboxybenzaldehyde (4-CBA) | 6.45 | 258 nm / m/z 149.0 – | 0.1 | 10.0 to 180.0 mg/kg |
| BHET Monomer | 8.90 | 242 nm / m/z 255.1 + | 1.0 | 95.5 to 99.2 wt% |
| MHET Intermediate | 11.30 | 242 nm / m/z 225.1 + | 0.5 | 0.20 to 2.50 wt% |
| Cyclic PET Trimer | 16.20 | 242 nm / m/z 577.1 + | 2.0 | 0.05 to 0.85 wt% |
Heavy metal catalyst residues represent an additional critical chemical checkpoint in depolymerization monomers. Industrial glycolysis processes frequently use zinc acetate, cobalt acetate, manganese salts, or titanium alkoxides to catalyze transesterification. If the downstream purification train fails to strip these catalysts through distillation, solvent recrystallization, or ion-exchange chromatography, high metal concentrations remain in the monomer feed.
When repolymerized, these metal residues accelerate thermo-oxidative degradation during subsequent extrusion, generating elevated levels of acetaldehyde in PET beverage bottles. Acetaldehyde levels are monitored via headspace gas chromatography with flame ionization detection (HS-GC-FID) following incubation at 150 degrees Celsius for 60 minutes, where values above 1.5 milligrams per kilogram impart distinct off-flavors to mineral water.
Polyamide depolymerization follows a similar analytical requirement. The hydrolytic depolymerization of nylon 6 carpet waste yields crude caprolactam contaminated with spin finishes, polypropylene backing fragments, and flame retardants. Verification of recycled caprolactam purity relies on gas chromatography with nitrogen-phosphorus detection (GC-NPD) and ultraviolet transmission testing at 290 nanometers.
Standard specifications mandate a minimum permanganate absorption number to ensure the removal of all readily oxidizable unsaturated impurities. A buyer receiving chemically recycled nylon 6 checks both the individual volatile amine contents and the optical absorbance curves across 200 to 400 nanometers to verify the thoroughness of monomer distillation.
Failing to strip cyclic oligomers from the recovered monomer stream causes extensive die-lip build-up and filament breakage during high-speed spinning operations on technical textile lines.
Leachate
When chemically recycled resins enter packaging production, compliance auditors evaluate the migration of Non-Intentionally Added Substances (NIAS). Thermal degradation during chemical recycling generates complex mixtures of branched hydrocarbons, cyclic alkanes, alkylated aromatics, and recombined molecular fragments. These substances do not appear on regulatory authorized lists and must undergo systematic risk assessments under Article 19 of Regulation (EU) 10/2011.
Migration testing quantifies whether these breakdown compounds leach from the finished plastic article into food at toxicologically unsafe levels.
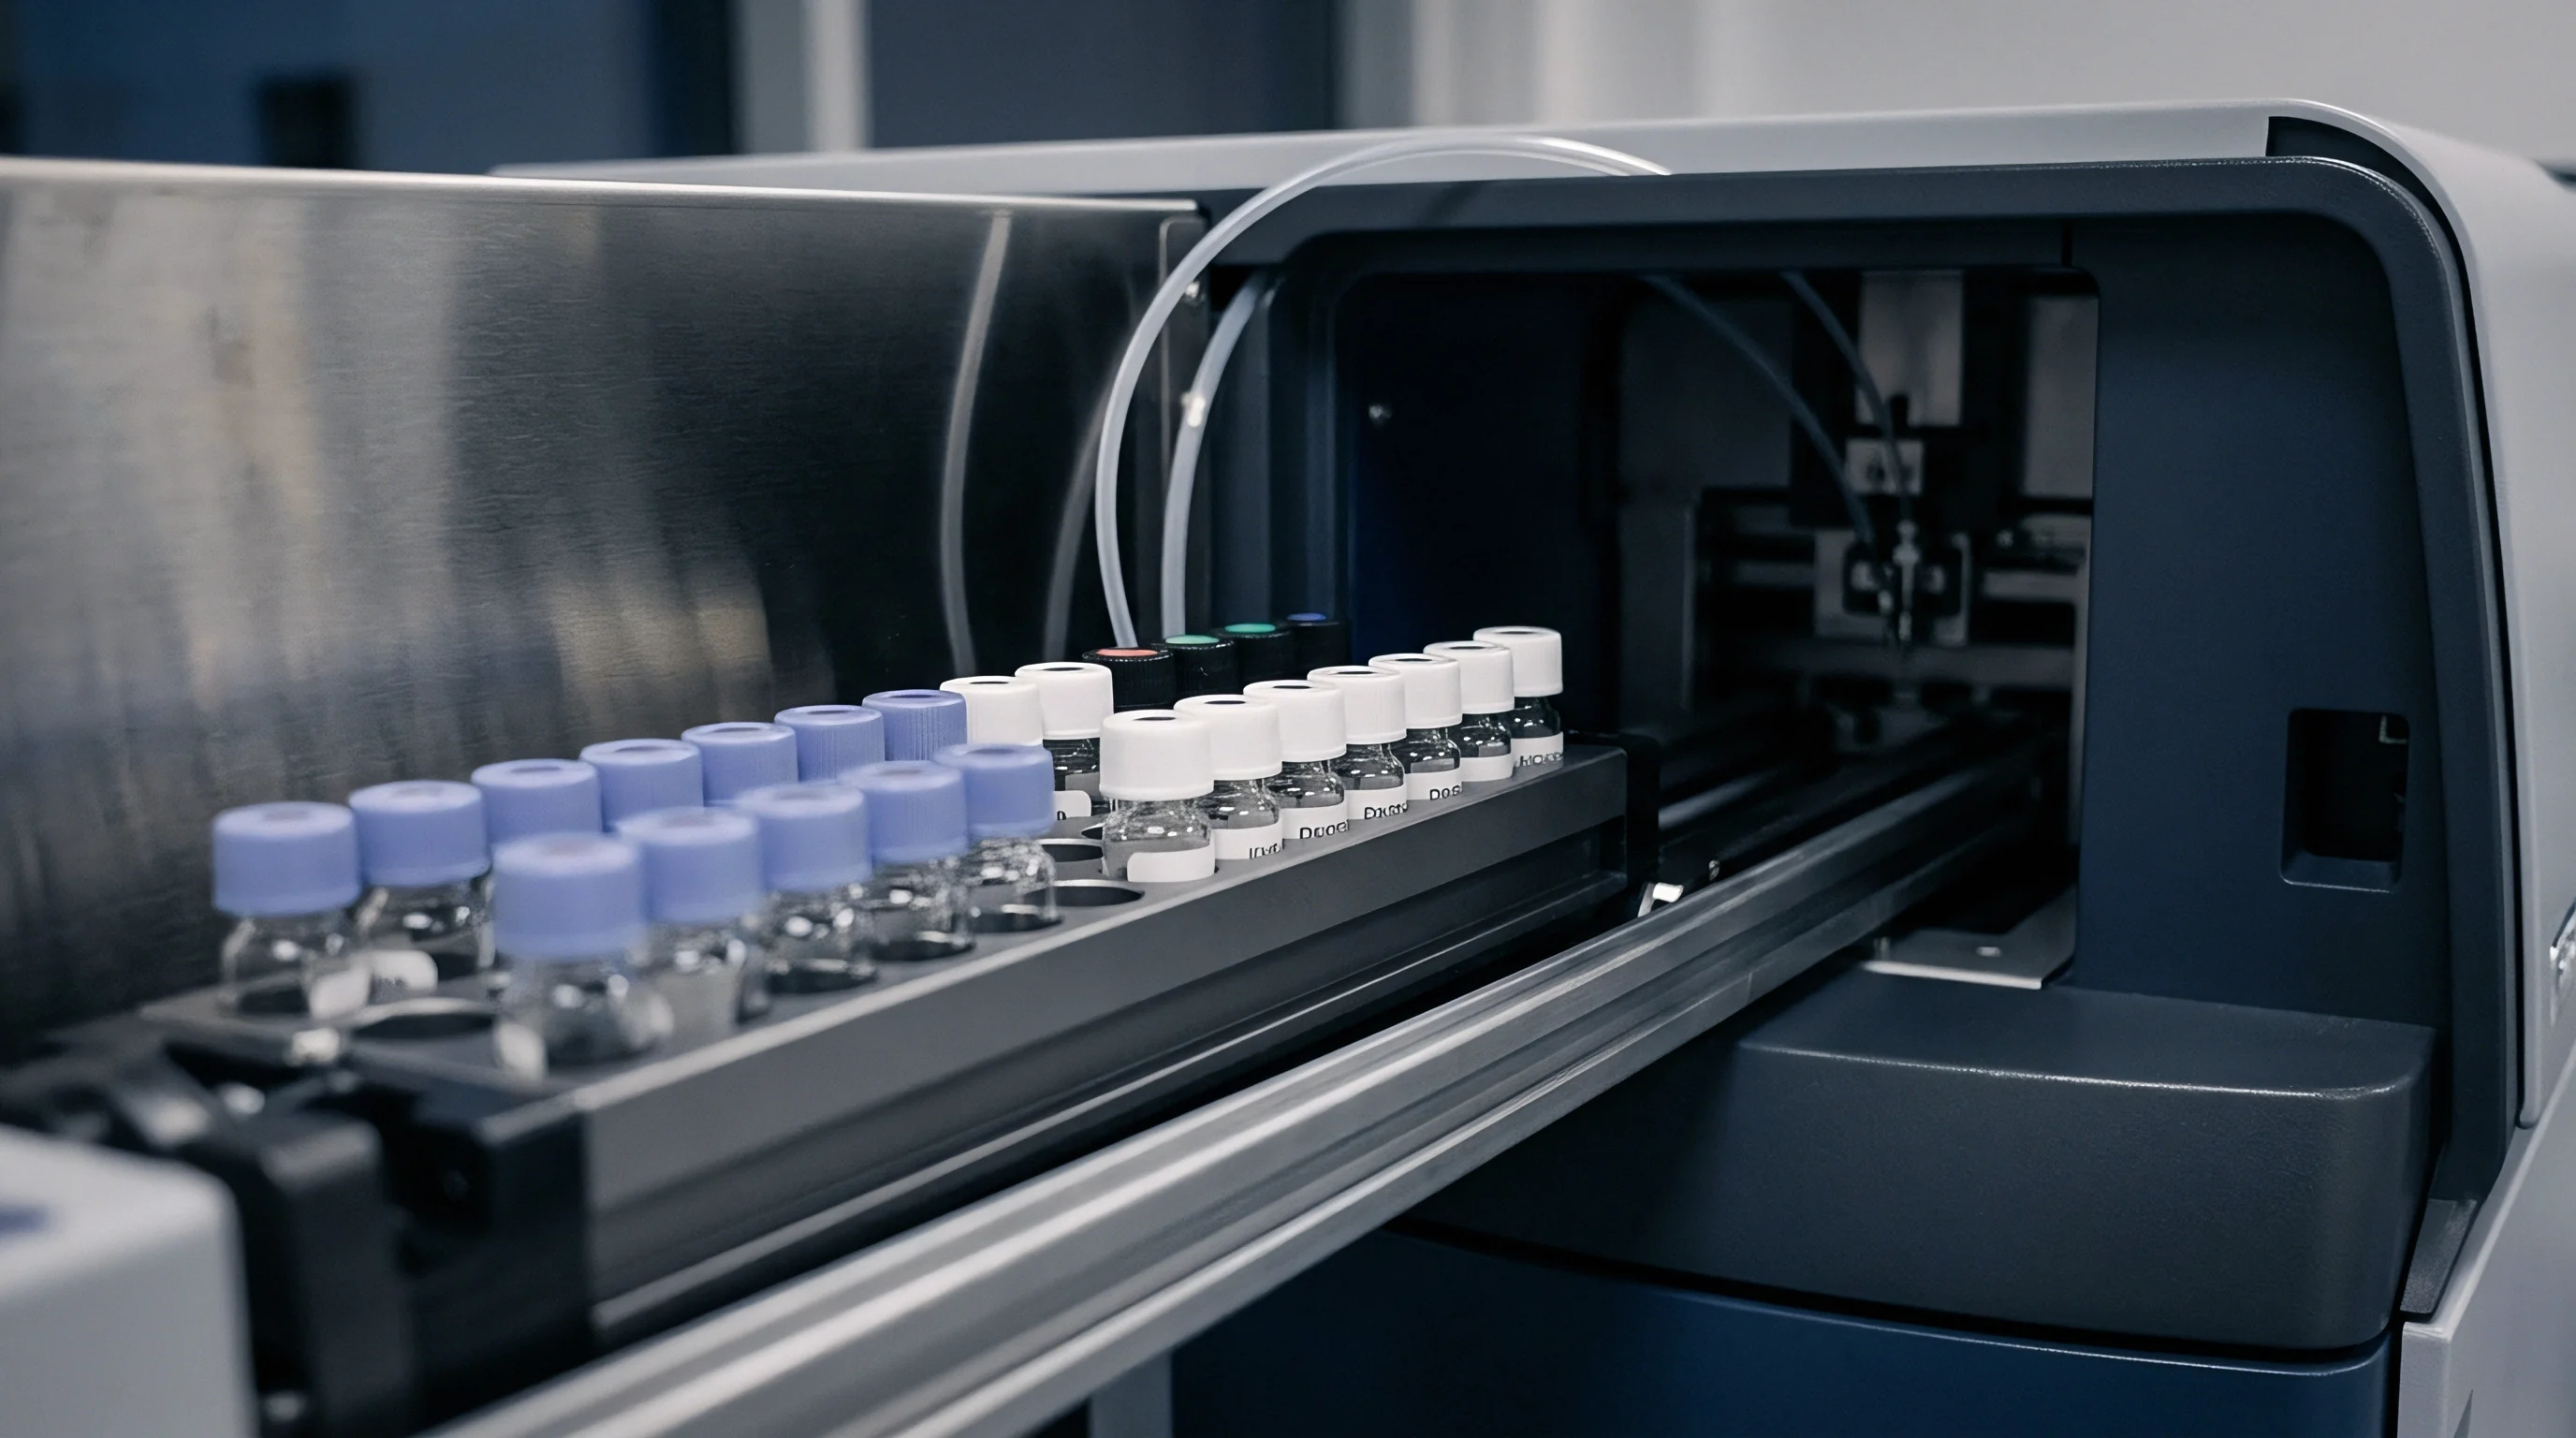
Laboratories expose finished plastic articles to liquid food simulants under controlled contact time and temperature regimes. The standard testing matrix uses simulant A (10 percent ethanol by volume) for aqueous foods, simulant B (3 percent acetic acid by weight) for acidic foods, and simulant D2 (rectified olive oil or vegetable oil) for fatty foods. For dry foods or high-temperature applications, poly(2,6-diphenyl-p-phenylene oxide), known commercially as Tenax, acts as simulant E under EN 14338.
Articles destined for room-temperature storage with extended shelf life undergo testing at 40 degrees Celsius for 10 days, while articles intended for hot-fill or microwave exposure face conditions reaching 100 degrees Celsius or higher under EN 1186 standards.
Extract Extraction and Gas Chromatography-Mass Spectrometry Screening
Following exposure, the simulant undergoes liquid-liquid extraction with dichloromethane or diethyl ether, volume reduction under gentle nitrogen streams at 35 degrees Celsius, and injection into high-resolution gas chromatography coupled to high-resolution accurate mass spectrometry (GC-HRAM-MS). For non-volatile extractables, liquid chromatography linked to quadrupole time-of-flight mass spectrometry (LC-QTOF-MS) provides accurate mass profiling with mass errors below 3 parts per million. Chemical identification matches accurate mass, isotopic abundance patterns, and fragmentation spectra against commercial databases, while semi-quantification proceeds against internal standards added prior to simulant extraction.
Overall migration from plastic materials into food simulants must not exceed 10 milligrams per square decimeter under Regulation (EU) 10/2011.
Chemically recycled polyethylene articles frequently release complex chromatographic humps consisting of thousands of unresolved branched alkanes and cycloalkanes, termed mineral oil saturated hydrocarbons (MOSH) and mineral oil aromatic hydrocarbons (MOAH). These mixtures originate from the cracked polyolefin waxes that failed to achieve full conversion to light monomers. Analysis by on-line coupled liquid chromatography-gas chromatography with flame ionization detection (LC-GC-FID) under EN 16995 separates MOSH and MOAH fractions into distinct integration windows.
The laboratory removes natural lipid interferences using an activated silica gel column impregnated with silver nitrate, preventing false positive readings for circular polyolefins.
- Aliphatic oligomer accumulation generates significant chromatographic background between carbon numbers C16 and C35, requiring baseline subtraction routines to isolate discrete contaminant peaks.
- Aromatic contamination profiles identify mono- and di-aromatic fractions derived from alkylbenzenes and alkylnaphthalenes, where MOAH levels above 0.5 milligrams per kilogram trigger toxicological alerts.
- Organophosphite breakdown products appear as oxidized phosphate esters and alkylphenols resulting from secondary processing stabilizers consumed during the original pyrolysis cycle.
- Epoxidized soybean oil byproducts leach as mono- and di-hydroxy derivatives when plasticized waste streams enter chemical depolymerization reactors without prior washing.
Toxicological qualification of migrating NIAS follows the Threshold of Toxicological Concern (TTC) approach established by the European Food Safety Authority. Compounds lacking specific structural alerts for genotoxicity, categorized under Cramer Class I or III, carry human exposure thresholds of 1,800 and 90 micrograms per person per day, respectively. For substances exhibiting unverified structures or clear genotoxic structural alerts, such as certain aromatic amines or epoxides, the exposure threshold drops to 0.15 micrograms per person per day.
Translated to packaging migration limits, this demands an analytical detection limit of 0.0001 milligrams per kilogram in the foodstuff, challenging the limits of modern extraction and mass spectrometry workflows.
A buyer cannot verify circularity from migration clean sheets, because exceptional chemical purification can render a circular polymer analytical profile indistinguishable from virgin grade resin.
Audit
Because finished polymers produced from cracked pyrolysis oils remain chemically indistinguishable from virgin fossil materials, the plastics industry verifies chemically recycled content primarily through administrative mass balance systems. In a mass balance framework, circular and fossil feedstocks mix freely inside the refinery cracker, and accounting rules attribute the input recycled volumes to specific output product batches. Independent certification schemes, most prominently the International Sustainability and Carbon Certification (ISCC PLUS) and REDcert2, provide the verification architecture governing these attribution claims.
Auditors verify the mass balance ledger by matching mass quantities across the chemical transformation chain. The tracking balance requires strict physical boundaries, termed the system boundary, which encompasses the pyrolysis plant, cracking furnace, polymerization unit, and compounding lines. The conversion factors linking input oils to finished polymers must reflect physical yields rather than arbitrary allocations.
When a cracker runs 100 tonnes of post-consumer pyrolysis oil alongside 900 tonnes of fossil naphtha, the facility produces distinct chemical fractions based on thermal cracking dynamics: roughly 30 percent ethylene, 15 percent propylene, 10 percent C4 olefins, and 45 percent heavy pyrolysis gasoline and aromatics.
Credit Allocation and Substitution Bookkeeping
The core dispute in mass balance certification surrounds attribution methodology. Under free attribution rules, a chemical manufacturer can mathematically pool all recycled credits generated from the 100 tonnes of mixed pyrolysis oil and allocate them exclusively to a single high-value product, such as food-grade polypropylene. This allows the producer to declare a batch of polypropylene as 100 percent chemically recycled, even though physical cracking yields make it chemically impossible for all cracker products to consist of propylene.
Under proportional attribution or fuel-exempt models, the producer can assign recycled content only in strict proportion to the stoichiometric yield of each product stream, deducting the 45 percent fraction consumed as cracker fuel or diverted into industrial aromatics.
| Product Stream | Physical Process Yield (wt%) | Proportional Allocation Output (Tonnes) | Free Attribution Maximum (Tonnes) | Fuel-Exempt Allocation (Tonnes) |
|---|---|---|---|---|
| Ethylene (PE Resin) | 31.0 | 31.0 | 0.0 (Shifted to PP) | 38.8 |
| Propylene (PP Resin) | 16.5 | 16.5 | 100.0 (Concentrated) | 20.6 |
| C4 Fraction (Butadiene) | 9.5 | 9.5 | 0.0 | 11.9 |
| Pyrolysis Gasoline (BTX) | 23.0 | 23.0 | 0.0 | 28.7 |
| Internal Fuel Gas / Loss | 20.0 | 0.0 (Unallocated) | 0.0 | 0.0 (Deducted) |
Declarations of Conformity (DoC) referencing chemically recycled plastics under mass balance rules must explicitly declare the certification scheme, the facility’s certificate number, the exact allocation methodology used, and the credit bookkeeping period. Under ISCC PLUS rules, credit transfer periods cannot exceed three months, preventing manufacturers from banking seasonal credits to smooth long-term inventory deficits. Auditors examine the incoming material invoices, bills of lading, and weighbridge records against internal Enterprise Resource Planning (ERP) receipts to ensure no double-counting of circular credits occurs across regional operating sites.
Document auditors verify whether the supplier’s declaration covers the entire finished packaging article or solely the base polymer granule. A container of finished pharmaceutical bottles accompanied by a mass balance certificate frequently contains virgin color masterbatches, uncertified slip additives, and fossil-based barrier coatings that dilute the final recycled content percentage. When the raw resin arrives with a certificate for 50 percent mass balance recycled content, but compounding adds 5 percent mineral talc and 2 percent pigment masterbatch without circular credentials, the finished container carries exactly 46.5 percent net circular content.
Failure to audit component declarations exposes importers to serious mislabeling penalties under packaging legislation.
The auditor verifies the site’s mass balance credit register directly against the ERP stock issuance logs to identify credit deficits before signing the conformity declaration.
Levy
The commercial friction surrounding chemically recycled content verification crystallizes in national packaging levies and Extended Producer Responsibility (EPR) fee modulations. Across the European Union and the United Kingdom, environmental tax laws impose steep financial charges on plastic packaging that fails to meet minimum verified thresholds of recycled content. The United Kingdom Plastic Packaging Tax charges 217.85 pounds per tonne on manufactured or imported plastic packaging components containing less than 30 percent verified recycled content.
Packaging containing chemically recycled plastic falls under this tax framework, making evidentiary records a primary tax liability issue.
Tax authorities do not accept standard commercial invoices or unverified factory assertions as proof of exemption. The UK HM Revenue and Customs (HMRC) requires importers and packaging converters to hold an unbroken chain of custody backed by certified mass balance records or physical analytical proof. If an importer claims exemption based on chemically recycled polymers certified under an unaccredited mass balance standard or a fuel-inclusive allocation model, tax auditors reject the exemption.
The importer faces retrospective payment of the full packaging tax, compound statutory interest, and severe administrative non-compliance fines.

Financial Risk under Divergent National Packaging Directives
Regulatory fragmentation across jurisdictions introduces compounding financial risks for multinational brand owners. In several European member states, including Spain under Law 7/2022 on Waste and Contaminated Soils, an excise tax of 0.45 euros per kilogram applies to non-recycled plastic packaging. The Spanish tax authority accepts recycled content declarations verified through accredited certification bodies under standard UNE-EN 15343 for mechanical recycling.
For chemical recycling, the acceptance of mass-balanced polymer credits remains constrained by strict national criteria governing attribution, where free attribution models risk rejection by local tax enforcement teams.
Corporate accounting departments balance the raw material premium demanded by resin suppliers against the avoided packaging tax. Virgin polypropylene granules trade within typical commodity price bands, whereas chemically recycled polypropylene carrying an ISCC PLUS mass balance certificate commands a green premium ranging from 400 to 900 euros per tonne above virgin market benchmarks. An operational scenario demonstrates the fine margins involved in purchasing decisions:
- Baseline resin procurement ~ A converter purchases 500 tonnes of virgin polypropylene at 1,200 euros per tonne, incurring 600,000 euros in direct polymer costs.
- Tax liability assessment ~ Shipping the finished packaging into Spain triggers an excise tax of 450 euros per tonne on non-recycled content, generating a 225,000 euro tax bill and bringing total landed material expenditure to 825,000 euros.
- Recycled resin procurement ~ Sourcing 500 tonnes of 30 percent mass-balanced polypropylene at a 600 euro per tonne green premium sets the base resin cost at 1,380 euros per tonne, totaling 690,000 euros.
- Tax mitigation calculation ~ If the mass balance certification withstands audit, the 30 percent circular credit reduces taxable virgin plastic down to 350 tonnes, lowering the excise tax liability to 157,500 euros and netting a total landed cost of 847,500 euros.
If the tax auditor rejects the mass balance attribution methodology, the converter loses the 90,000 euro resin premium paid to the supplier and pays the full 225,000 euro packaging tax. Procuring mass-balanced resin without verifying that the certification model aligns with the importing country’s tax code turns an intentional sustainability hedge into an immediate financial loss. Importers insulate themselves against these liabilities by integrating indemnification clauses into supply contracts, requiring the resin manufacturer to cover all packaging tax penalties and legal costs if their mass balance certificate fails to survive customs and tax authority scrutiny.
The contract clause holds the resin supplier liable for all assessed packaging taxes whenever their certification scheme fails national administrative audits.