Meaning
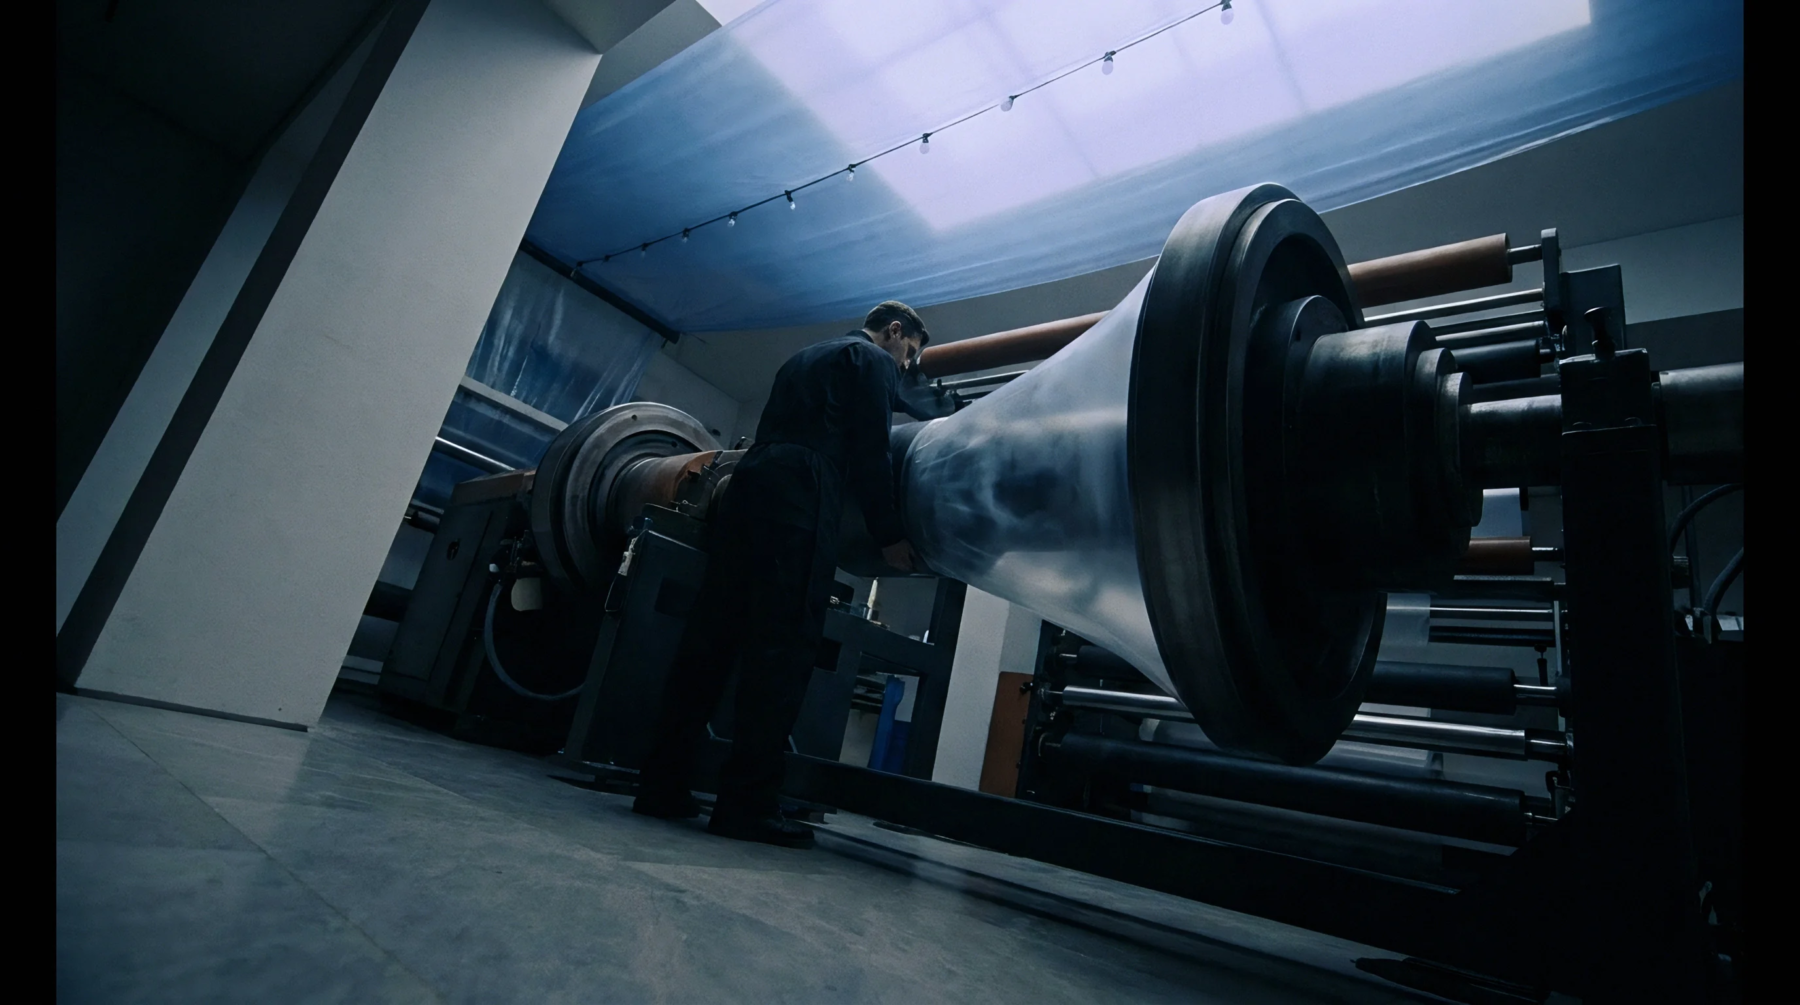
Melt elasticity under shear defines primary normal stress as the excess axial force generated perpendicular to the flow direction when polymer chains stretch during extrusion or moulding. This rheological property arises when polymer molecules uncoil and align under velocity gradients, creating a recoil force along the streamline that drives extrudate swell and melt fracture. The phenomenon dictates dimensional stability across processing equipment by storing elastic energy that recovers rapidly as material exits a shaping die or fills a mould cavity.
Elastic Recovery
Die swell magnitude depends directly on this internal stress state because stored elastic energy forces the extrudate outward upon pressure release. Polymeric melts with high elasticity exhibit pronounced diameter expansion relative to the orifice, requiring larger tooling offsets to achieve final part dimensions. Extrusion line speeds must compensate for this recovery to prevent dimensional drift and warping in continuous profiles.
Processing Limits
High shear rates in narrow runner systems elevate normal stress values until melt fracture occurs on the product surface. Moulders control barrel temperatures and injection velocities to keep these forces below the threshold of sharkskin defects and structural delamination. Processing windows narrow significantly when high molecular weight resins increase elastic resistance inside complex gating geometries.
Economic Tradeoffs
Virgin polymer grades maintain predictable elasticity parameters, whereas recycled resins show degraded normal stress responses due to chain scission during prior reprocessing cycles. Parts moulded from regrind blends require adjusted cooling cycles and clamping pressures to counteract unpredictable shrinkage caused by altered melt memory. Tooling designers account for these material variations by building adjustable calibration sleeves into the initial mould layout to absorb batch-to-batch rheological shifts without scrapping production runs.