Meaning
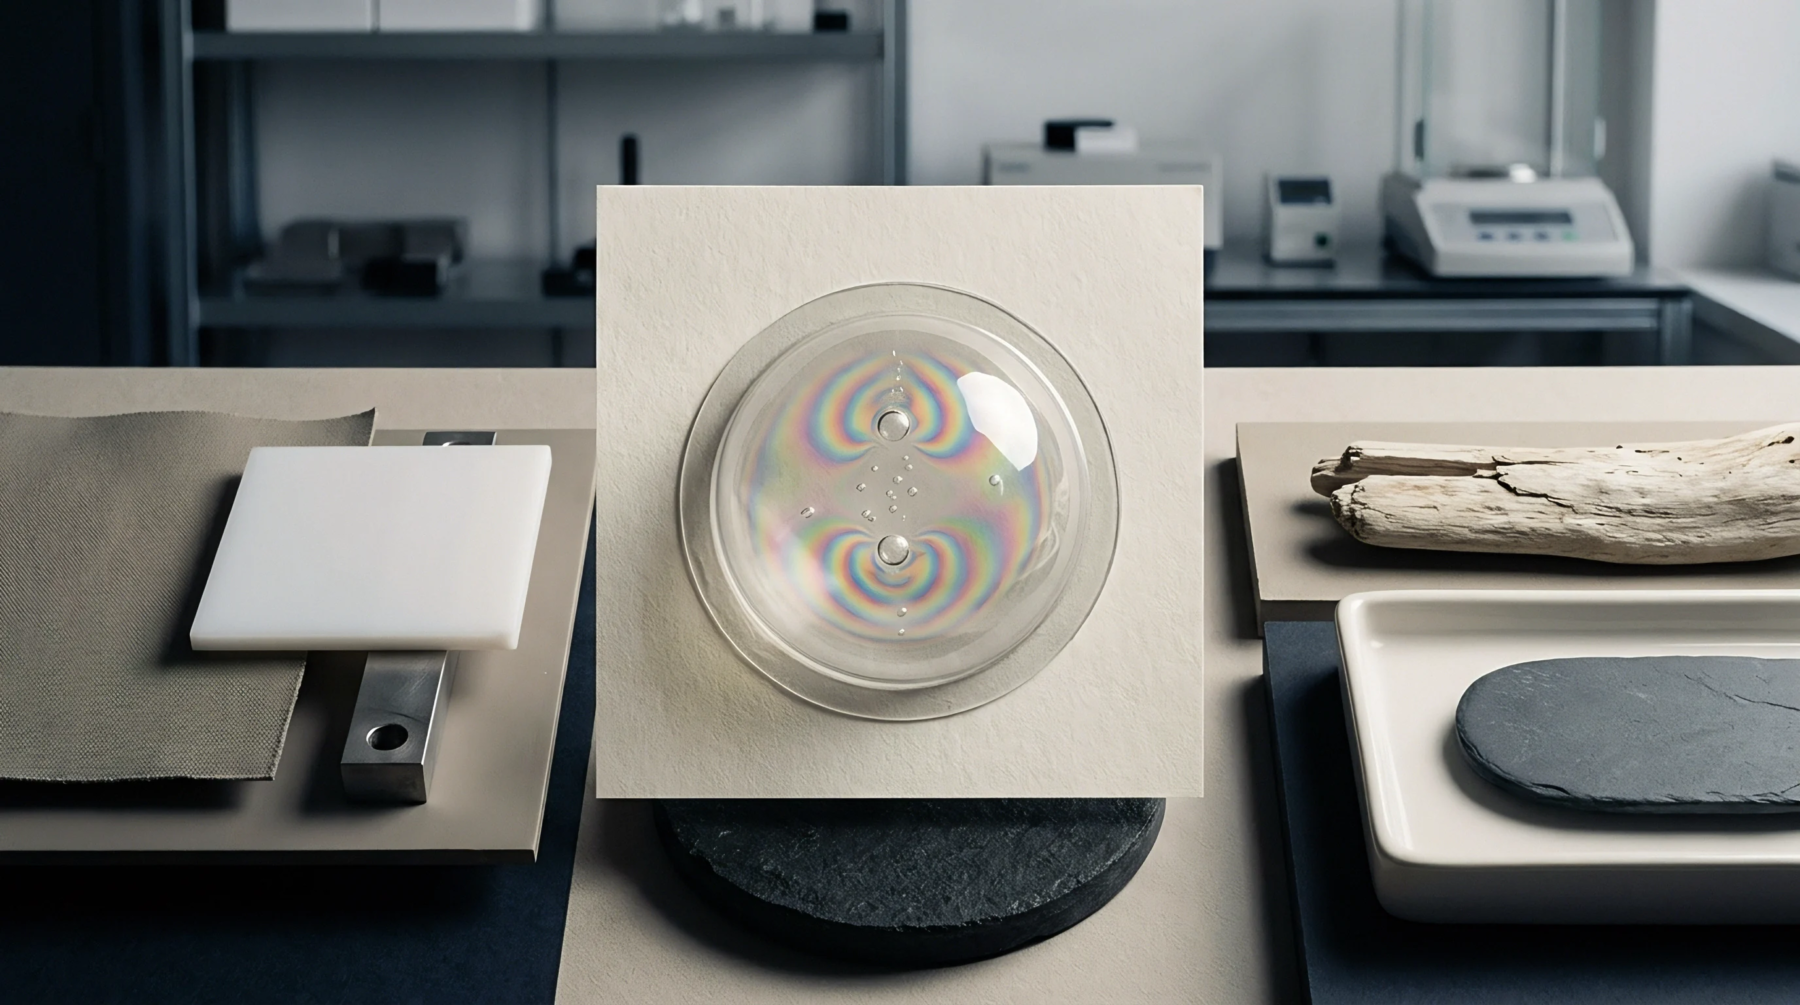
Light deviation arises when photons interact with microscopic inhomogeneities within a polymer matrix or upon the interface of a moulded surface. Optical scatter describes the angular redistribution of electromagnetic radiation as it traverses or reflects off a translucent medium. This phenomenon occurs when refractive index gradients or surface irregularities interrupt the incident path of light, forcing particles to deviate from their original vectors.
The intensity and direction of these dispersed waves define the clarity and haze characteristics of injection moulded parts and extruded films.
Processing Variable
Molecular weight distribution and thermal history dictate the internal uniformity of resin during the melt phase. Optical scatter increases when uncontrolled cooling rates create localised crystallisation zones or trapped air pockets inside a transparent part. Excessive shear stress during the injection process induces chain orientation that creates refractive index variations, which act as scattering centres.
Tooling temperature stability ensures the polymer cools in a manner that minimises these internal structural defects.
Resin Specification
Virgin pellets are tested against a baseline clarity standard to ensure batch consistency for high performance optical components. Manufacturers provide haze and transmission data to help moulders select materials for specific wall thicknesses where path length influences the degree of total dispersed light. Moulders verify these values by measuring a standard plaque because the internal scattering intensity depends on the actual cooling rate of the tool.
Regrind addition complicates the control of this metric as contaminants or degraded molecular segments introduce new sites for light deflection.
Cost Consequence
Surface roughness on the mould cavity imparts a finish that alters the way light exits the finished component. High levels of diffused light indicate a tool surface that has suffered from wear or chemical etching, leading to the rejection of parts that fail to meet visual aesthetic requirements. Excessive scrap rates accumulate when process adjustments fail to compensate for degraded resin properties or thermal drift.
Maintaining a strict correlation between tool polish and material throughput ensures that finished components remain within the tolerances set by the customer specification.