Transient Interfacial Macro Gap Prediction in Variotherm Injection Tooling
Coupled thermo-viscoelastic modeling of PVT shrink and tool expansion predicts variotherm macro gap formation and prevents optical distortion.
Interface
Piezoelectric transducer signals captured at the cavity wall reveal an immediate pressure decay from 45 MPa down to baseline during the cooling phase. Rapid mold surface temperature control elevates cavity steel above the polymer glass transition point before injection, then chills the steel rapidly prior to demolding. Elevated mold temperatures suppress premature freeze-off during filling, yielding pristine micro-replication and eliminating weld line witness marks.
Cooling forces rapid volumetric contraction within the polymer core while the outer skin freezes solid. Contraction pulls the polymer body away from cavity boundaries, creating a distinct air clearance.
Detachment creates a macro gap ranging between 5 and 60 micrometers wide across part surfaces. Thermal contact conductance collapses upon detachment. Direct solid-to-solid conduction through tool steel ceases, transferring heat transport duties to gas conduction across the entrapped air medium.
Interfacial thermal conductance drops from 3500 W/(m²·K) under full 40 MPa packing pressure down to 150 ~ 250 W/(m²·K) once a 20 µm gap opens. Thermal contact coefficient collapses. This sharp transition alters thermal boundary conditions mid-cycle, creating uneven cooling rates through wall sections.
Thermal Contact Degradation
Polymer melts rapidly transfer heat to cavity steel when high hydraulic packing pressures force full physical contact across mold surfaces. As packing pressure decays and volumetric shrinkage proceeds, contact pressure at the steel boundary drops to zero. Heat transfer kinetics shift from boundary conductance to gas-phase conduction across the developing macro gap.
Gas thermal conductivity governs heat dissipation once mechanical contact ceases.
| Material Grade | Cavity Pressure (MPa) | Interfacial Gap Width (µm) | Thermal Conductance (W/m²·K) | Heat Transfer Mechanism |
|---|---|---|---|---|
| Unfilled Polycarbonate | 40.0 | 0.0 | 3250 | Solid Micro-Contact Conduction |
| Unfilled Polycarbonate | 10.0 | 0.0 | 1400 | Deformed Contact Conduction |
| Unfilled Polycarbonate | 0.0 | 5.0 | 480 | Mixed Gas-Contact Conduction |
| Unfilled Polycarbonate | 0.0 | 25.0 | 180 | Entrapped Gas Conduction |
| PA66 GF30 | 45.0 | 0.0 | 3800 | High-Pressure Solid Conduction |
| PA66 GF30 | 0.0 | 35.0 | 145 | Entrapped Gas Conduction |
At an interfacial gap width of 25 micrometers under ambient cavity gas pressure, thermal contact conductance drops from 3200 W per square meter Kelvin to 180 W per square meter Kelvin.
Misjudging this thermal separation leads to asymmetric part warping, unpredicted core heat retention, extended cooling delay requirements, and rejected production lots under ISO 20753 dimensional inspection.
Mechanics
Polymer volumetric contraction interacts dynamically with tool expansion during surface thermal cycling. H13 tool steel expands linearly during elevated surface heating pulses, altering cavity dimensions relative to solidifying polymer. The steel expansion coefficient of 11.5 × 10⁻⁶ K⁻¹ expands a 100 mm cavity by 0.115 mm when thermal cycling swings tool surface temperatures by 100 °C. Polymer shrinkage kinetics follow modified Tait PVT equations, where volumetric contraction speeds up rapidly during phase transitions or glass conversion.
Thermal Expansion Coupling
Tool steel expands linearly during elevated surface heating pulses, altering cavity dimensions relative to solidifying polymer. Viscoelastic stress relaxation governs internal stress buildup as the material cools. Polymer volume drops rapidly.
Detachment occurs when internal thermal contraction forces surpass normal holding forces exerted by cavity pressure. Macro gap detachment triggers localized structural deformation modes across thin-wall and optical geometries.
- Differential Volumetric Sink Local detachment delays cooling rate, leaving interior melt hot while surrounding areas freeze, pulling surface inward.
- Optics Graded Birefringence Gradient Asymmetric thermal gradients lock in high residual shear stress along optic paths, causing refractive index shifts.
- Ejection Force Spikes Uneven gap growth causes part contraction onto mold cores, increasing frictional drag during pin ejection.
- Cycle Time Inflation Thermal resistance across macro gaps extends core cooling time past planned index targets.
Non-compliance with DIN 16742 Molded Part Tolerance Group TG4 invalidates delivery acceptance when unpredicted gap formation alters nominal linear dimensions beyond target limits.
Lowering tool cavity surface roughness delays skin detachment by enhancing microscopic mechanical adhesion during early thermal contraction.
Simulation
Finite element solvers calculate transient thermo-mechanical boundary shifts by updating local thermal contact conductance at discrete temporal steps. Numerical routines couple transient heat transport algorithms with non-linear mechanical stress computations. The mathematical formulation models thermal contact conductance across the macro gap as a composite function of gas thermal conductivity, gap width clearance, and radiation transport.
Gas conductivity dictates heat transfer. Calculated clearance values determine boundary resistance at every surface node. Solver stability demands tight time-step management during rapid fluid temperature switches, preventing numerical oscillations when contact pressure drops to zero.
Governing Contact Conductance Formulations
Mathematical representations of heat transport across gas gaps treat air conductivity and local displacement as primary variables. The gap conductance coefficient incorporates gas thermal conductivity divided by predicted clearance distance plus equivalent surface roughness parameters. Pressure-dependent contact functions govern heat transfer prior to physical detachment, switching smoothly to gap equations upon separation.
| Polymer Family | Tait Parameter b1m (m³/kg) | Tait Parameter b2m (m³/kg·K) | Volumetric Thermal Expansion (1/K) | Gas Conductivity k_gas (W/m·K) |
|---|---|---|---|---|
| Polycarbonate (PC) | 0.000852 | 0.00000068 | 2.1 × 10⁻⁴ | 0.028 |
| Polyetheretherketone (PEEK) | 0.000780 | 0.00000052 | 1.6 × 10⁻⁴ | 0.032 |
| Polymethyl Methacrylate (PMMA) | 0.000840 | 0.00000062 | 2.3 × 10⁻⁴ | 0.026 |
| PA66 30% Glass Fiber | 0.000720 | 0.00000041 | 1.1 × 10⁻⁴ | 0.030 |
- Import CAD boundary surface meshes with a minimum of eight layer elements across wall thickness.
- Input temperature-dependent thermal conductivity, specific heat capacity curves, and 13-parameter Tait PVT coefficients.
- Apply transient thermal boundary conditions reflecting rapid heating fluid flow followed by chilled coolant cycle times.
- Define contact boundary conditions incorporating pressure-dependent heat transfer coefficients prior to detachment.
- Solve coupled non-linear stress balance at each thermal step to evaluate gap clearance growth.
Tooling software vendors state that assuming a constant average heat transfer coefficient delivers adequate warpage trends without incurring numerical solver computation delays.

Bench
Experimental verification relies on flush-mounted sensor arrays embedded within test mold inserts. Quartz piezoelectric transducer pins record cavity pressure decay while fast-response thermocouples capture surface thermal transients. Fast sensor response rates identify the exact moment physical contact ceases during chilling pulses.
Shrinkage forces detachment early.
Could in Mold Sensors Track Detachment?
Fiber-optic infrared sensors track polymer surface temperature directly through sapphire optical windows. The instant detachment occurs, the cooling rate of the polymer skin dramatically drops while mold steel temperature drops rapidly, creating a clear thermal divergence point on the oscilloscope. In-tool capacitive sensors measure micro-capacitance variations across air gaps, delivering direct gap distance readings down to sub-micron resolution.
- Flush Piezoelectric Transducers Track exact timing of cavity pressure drop to zero, signaling loss of mechanical packing contact.
- Fiber Infrared Thermocouples Measure polymer surface temperature directly to detect instantaneous slope changes in thermal decay.
- In Tool Capacitive Sensors Monitor dielectric micro-capacitance changes across the air gap between cavity wall and polymer surface.
- Optical Coherence Tomography Capture cross-sectional profile evolution of interfacial clearance during transient thermal cycling pulses.
Higher packing pressure duration holds the polymer skin firmly against cavity steel until internal solidification prevents post-gate detachment.
ISO 294-4 specimen preparation protocols mandate uniform mold wall contact throughout cooling, forcing tools with unverified interfacial gap control into compliance audits.
Geometry
Part profile variations dictate how shrinkage forces translate into interfacial detachment distances. Curved surface contours and deep rib features alter localized strain accumulation. Radial thermal contraction pulls cylindrical geometries inward away from cavity walls while clamping tightly onto core pins.
Cavity surface temperatures decay. This directional anisotropy produces uneven gap clearances across complex tool cavities.
Optical Plaque Dimensional Analysis
A four-millimeter thick Polycarbonate optical plaque illustrates the thermal and mechanical progression of transient gap growth. Take a 120 mm diameter optical plaque produced in H13 tool steel with targeted thermal cycling (140 °C surface heating during injection, 70 °C chilling prior to ejection). Volumetric shrinkage of Polycarbonate from melt conditions (290 °C, 50 MPa) to ejection state (110 °C) reaches 0.65 percent.
H13 steel cavity radius contracts by 0.048 mm over the 70 °C thermal transition.
Interfacial gaps alter dimensions. Perimeter gap clearance reaches 34.2 µm under transient thermal cycling compared to 18.5 µm under constant 90 °C isothermal molding. Heat transfer conductance drops from 2800 W/(m²·K) down to 165 W/(m²·K) at second 4.8 of the cycle.
Extended thermal isolation requires an extra 3.4 seconds of core cooling to lower center temperature below the 125 °C ejection threshold.
| Molding Process Regime | Peak Gap Width (µm) | Conductance at Detachment (W/m²·K) | Cooling Time to Ejection (s) | Optic Planar Warpage (mm) |
|---|---|---|---|---|
| Isothermal 90 °C Tooling | 18.5 | 310 | 14.2 | 0.380 |
| Variotherm 140 °C / 70 °C Cycling | 34.2 | 165 | 17.6 | 0.045 |
| Variotherm with Extended Pack | 12.1 | 420 | 15.1 | 0.018 |
| Data derived from 120 mm plaque trials using optical polycarbonate grade under 50 MPa hydraulic injection pressure. | ||||
Volumetric shrinkage rates in thick optical sections outpace mold thermal contraction, creating interfacial clearances before core temperature stabilizes.
- Conformal Heat Channel Layout Position heating lines within one channel diameter of cavity walls to minimize bulk steel expansion differentials.
- High Thermal Conductivity Inserts Integrate copper-alloy mold inserts near deep ribs to maintain heat extraction after macro gap detachment.
- Pressurized Water Cycling Systems Utilize high-temperature pressurized fluid units capable of rapid valve switching to minimize thermal lag.
- Dynamic Cavity Pressure Control Maintain extended multi-stage packing pressure curves aligned with actual volumetric thermal contraction rates.
How advanced laser-textured micro-grooves along cavity walls might sustain micro-gas conduction paths without compromising optical clarity remains a subject of ongoing active testing across commercial mold shops.
Valuation
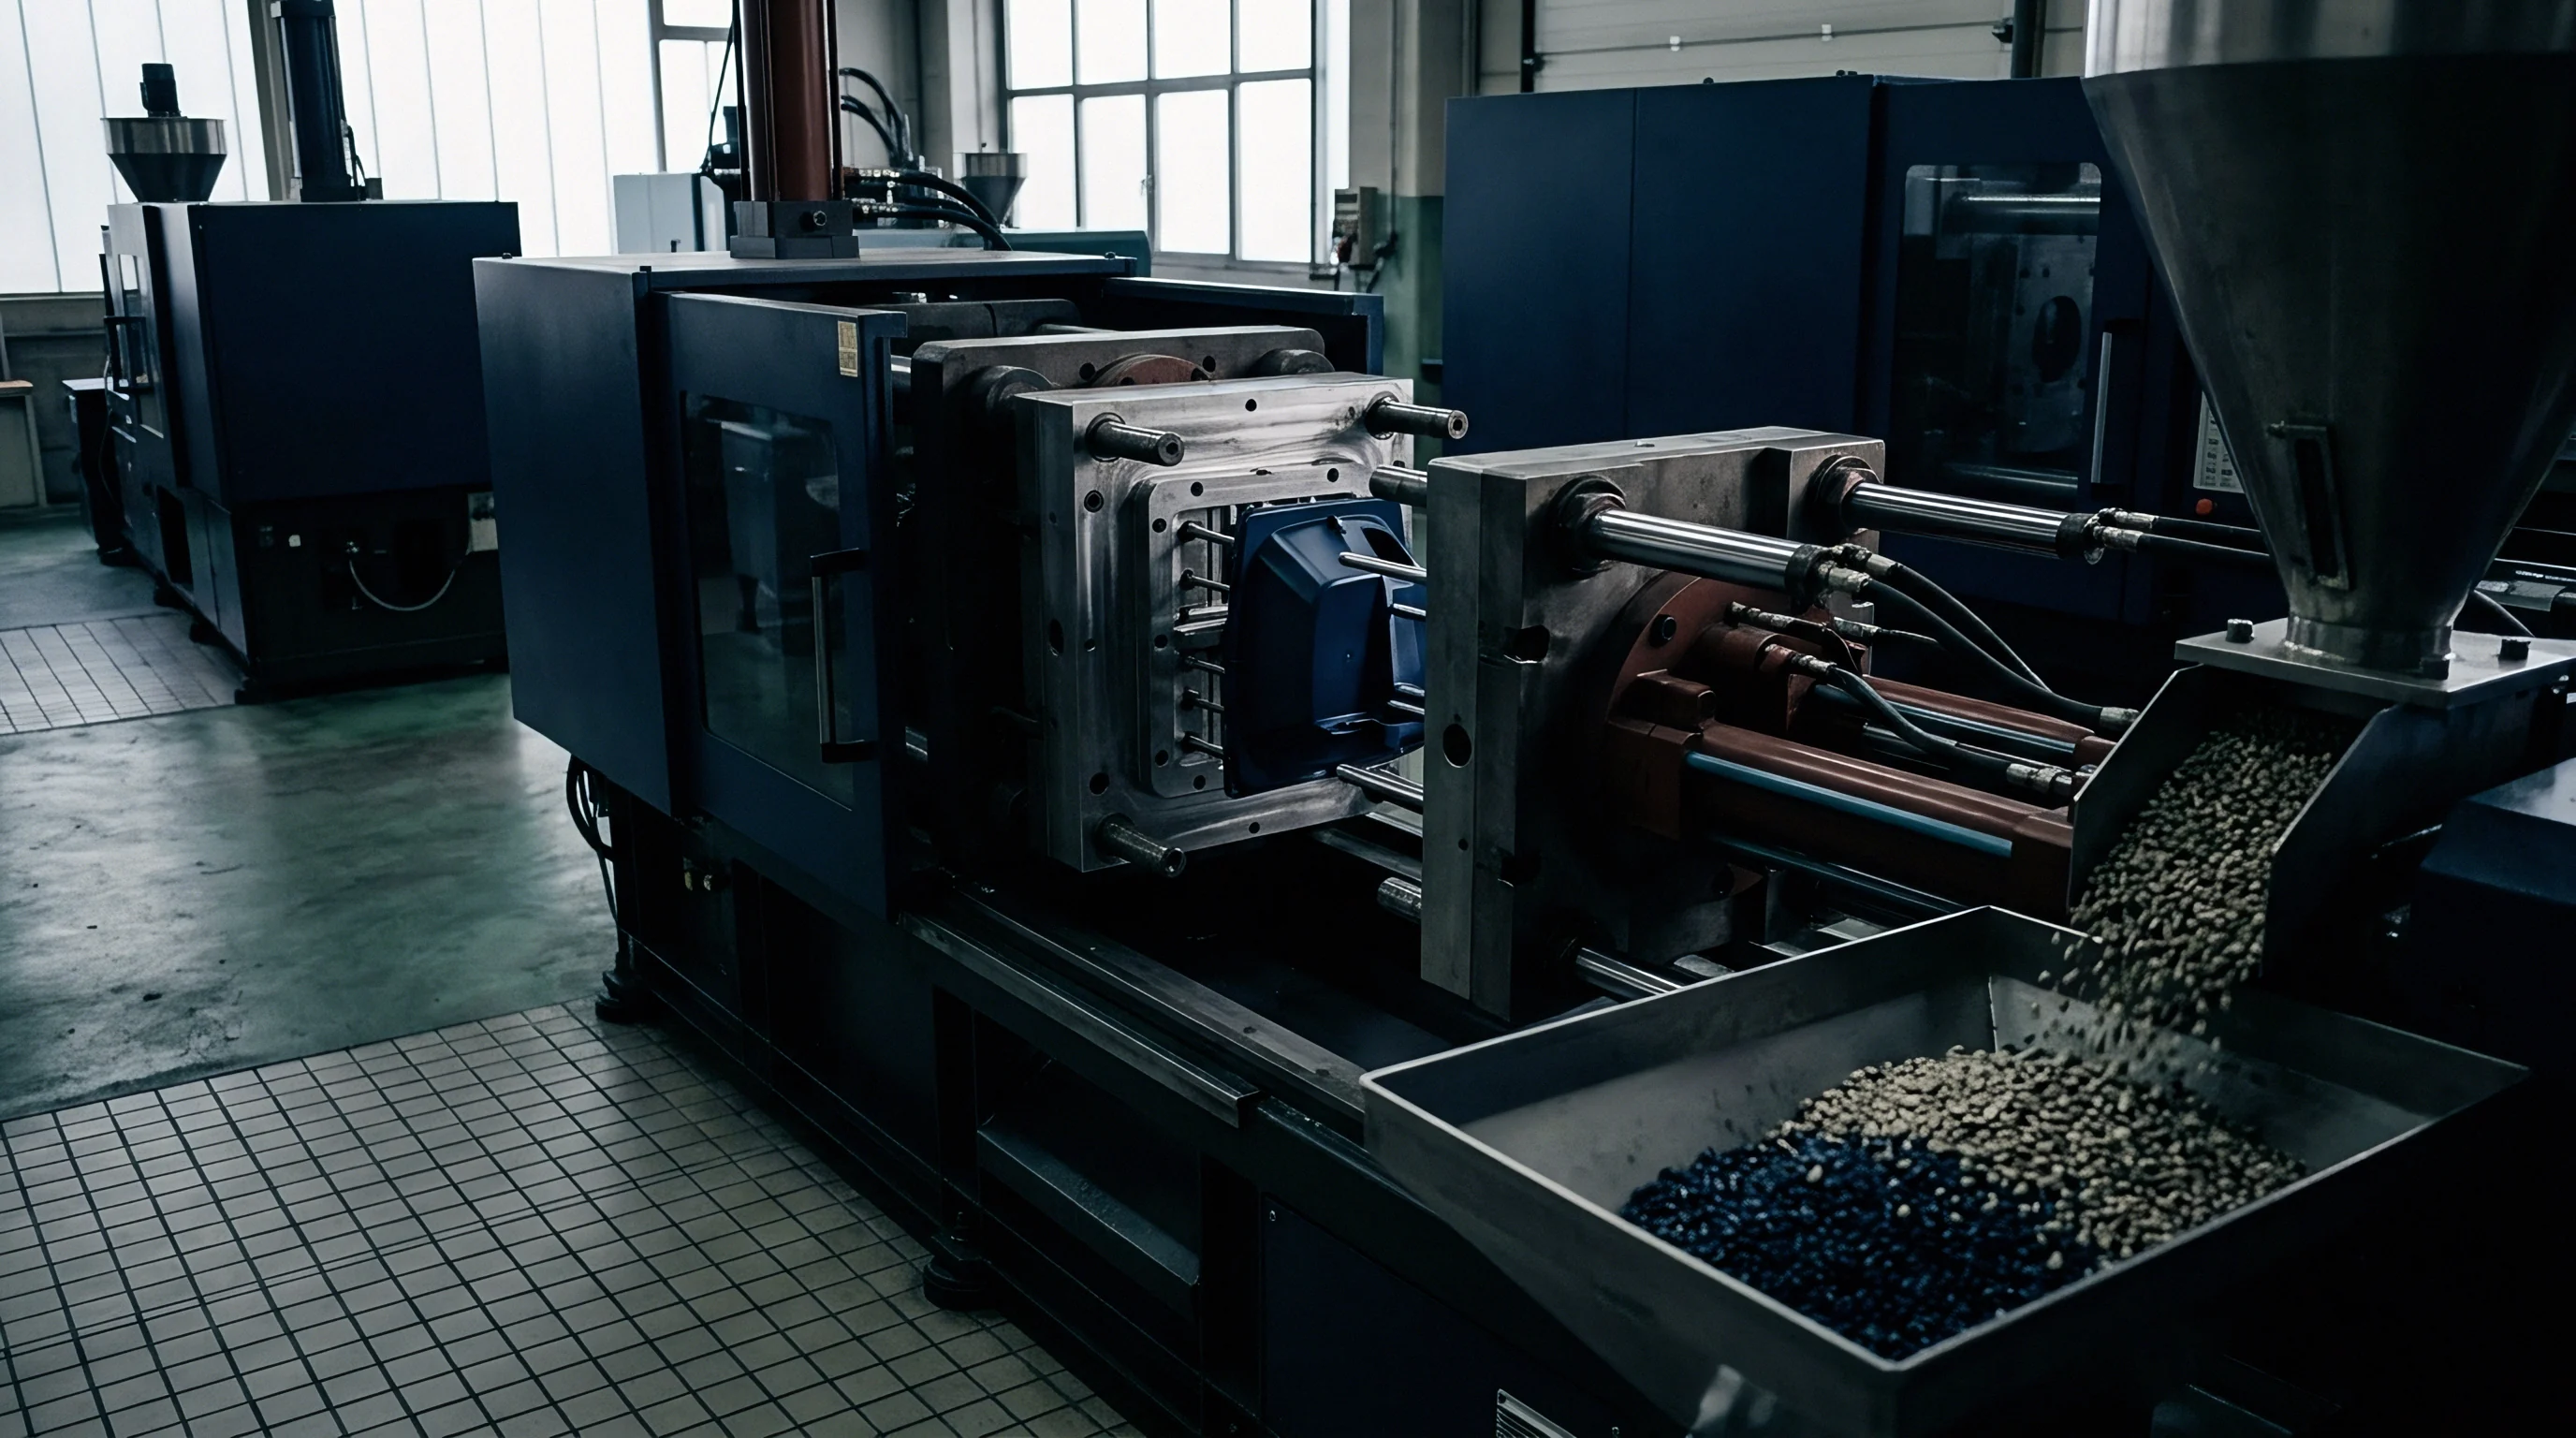
Dynamic mold heating equipment and specialized tooling structures add significant capital expenditure that must be justified through part quality improvements. Advanced conformal cooling circuits, specialized tool steel treatments, and dual-fluid control manifolds increase initial tooling charge by $28,000 to $65,000 for a 4-cavity production tool. Processing cycle time increases by 4.5 seconds for heating and fluid evacuation switches.
Wall thickness reduction made possible by eliminating surface stress allows nominal wall thin-down from 4.0 mm to 2.8 mm. Thinning reduces baseline cooling time by 6.2 seconds, securing a net savings of 1.7 seconds per cycle.
Tooling Amortization and Cycle Economics
Conformal variotherm tooling modifications increase initial mold fabrication costs by twenty-eight thousand to sixty-five thousand dollars per four-cavity tool. Consider a 500,000-unit annual production run operating on a $85 per hour press rate. Net cycle savings of 1.7 seconds yields 236 machine operating hours saved annually, amounting to $20,060 in direct annual machine time cost reductions.
Tooling premiums amortize fully within 20 months of continuous production while achieving zero-defect optical quality standards.
Sensors capture pressure drops. Thermal cycling between 80 °C and 160 °C generates cyclic thermal stress amplitudes near 180 MPa within surface steel layers. Tool life reflects thermal cycling.
H13 steel hardened to 52 HRC withstands approximately 650,000 thermal cycles before micro-cracking occurs across high heat flux regions.
Tool amortisation schedules for dynamic variotherm production runs must incorporate planned cavity insert refurbishments every five hundred thousand cycles to maintain sealing integrity and prevent thermal fluid leaks into the cavity interface.