Meaning
Dimensionless geometric characterization of particle contours and aspect ratios quantifies the deviation of polymer pellets, regrind flakes or mineral filler particles from perfect spherical geometry. Calculating the shape factor defines the physical profile that dictates bulk packing density, internal friction angles and fluidization dynamics in solids processing systems. The metric governs bulk material storage in silos, pneumatic transport line friction and solids feeding behavior in injection or extrusion throats.
Its influence stops applying once polymer particles undergo melting inside the barrel, where fluid rheology and molecular weight distribution replace particulate morphology as the dominant physical drivers.
Geometric Ratio
Aspect ratio calculations comparing maximum particle length to minimum equivalent diameter establish the numerical baseline for granulate morphology. A shape factor close to unity describes spherical underwater-pelletized resin, whereas strand-cut cylindrical pellets or irregularly shredded regrind flakes exhibit values deviating substantially from unity. High circularity promotes fluid gravity discharge from bins, whereas jagged regrind fragments lock together mechanically.
Optical image analyzers measure thousands of individual particles to determine the median dimensional distribution across a production batch.
Bulk Handling Behavior
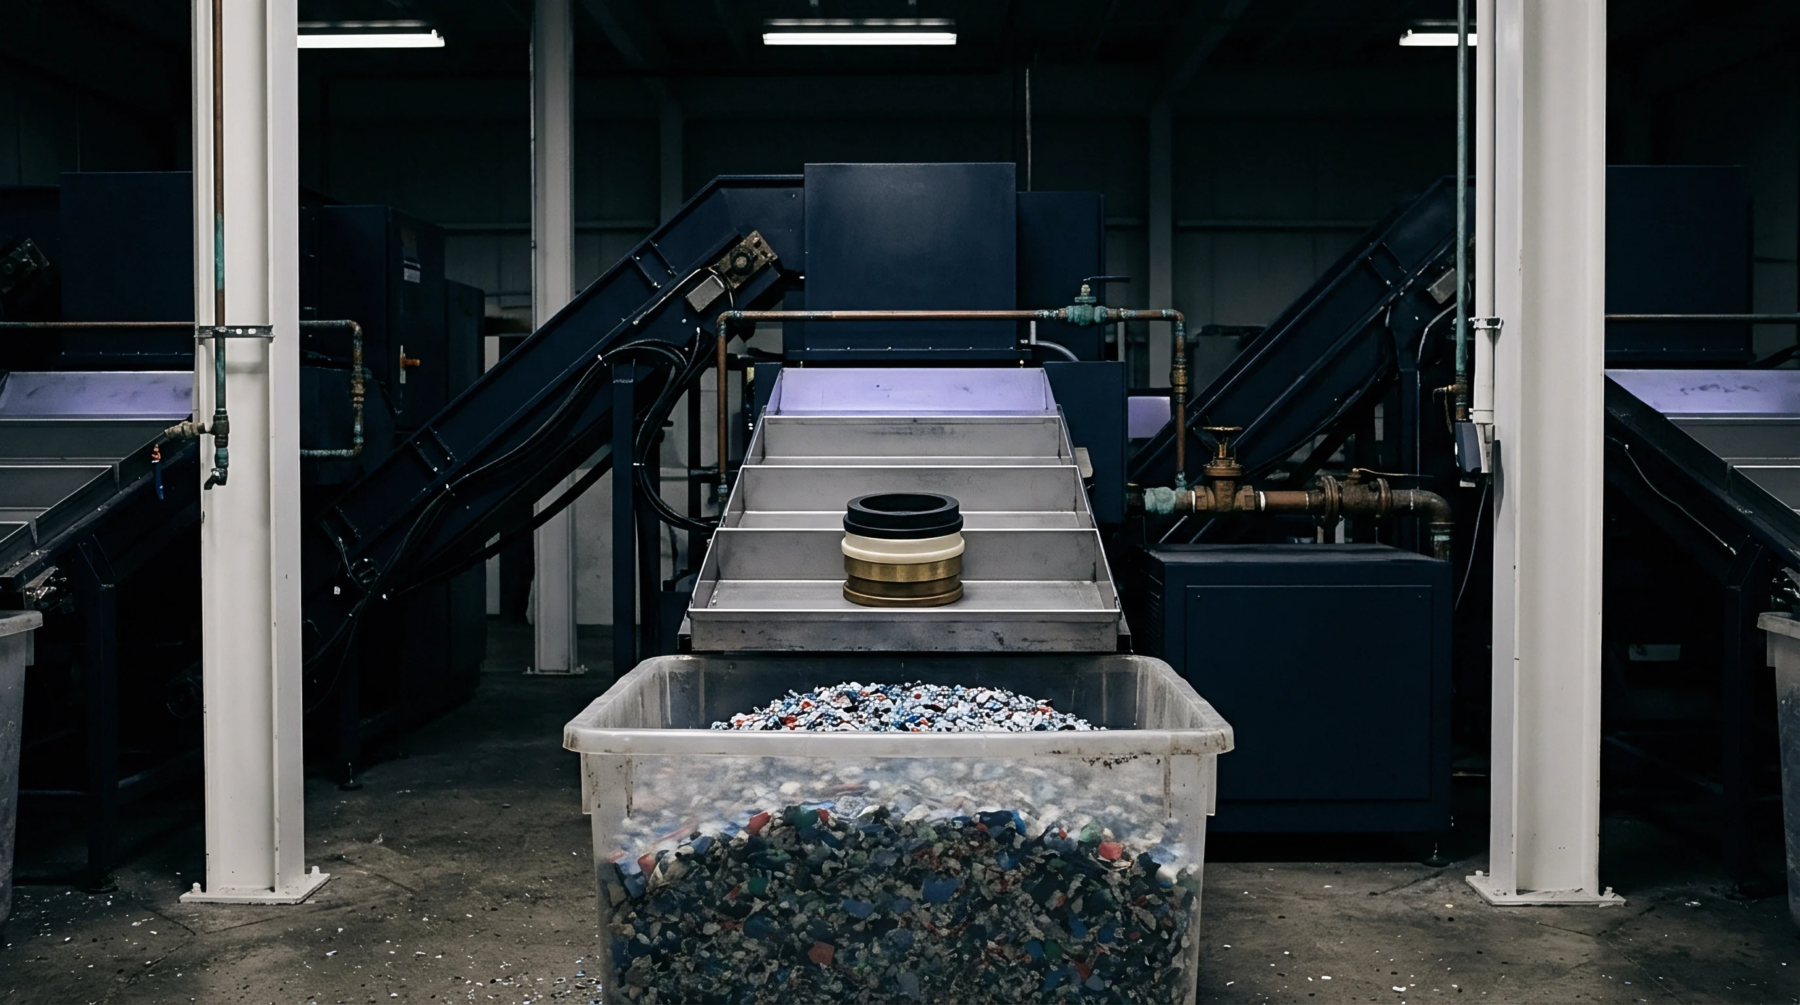
Gravity flow through hopper cones changes dramatically depending on whether resin particles are smooth spheres or jagged flakes. As the shape factor drifts away from spherical values, mechanical interlocking increases the angle of repose, leading to bridging, ratholing and feed throat interruptions. Extruder operators transitioning from spherical virgin polyethylene to post-consumer regrind frequently encounter surging because low shape factors lower apparent bulk density.
This low bulk density reduces the mass of resin conveyed per screw revolution, requiring higher screw speeds that introduce erratic shear heating. In gravimetric blenders, flat flakes settle differently than cylindrical masterbatch pellets, resulting in blend de-mixing and color shifts across long extrusion runs. Datasheet bulk density values measured with standardized test cups fail to capture dynamic flow disruptions caused by irregularly shaped particles during rapid hopper discharge.
Plastication Rate
Surface area exposure determined by particle geometry controls the rate of conductive heat transfer from heated barrel walls. A high shape factor in flat flakes accelerates initial melting along screw flights, causing uneven solid-bed breakup compared to uniform cylindrical pellets.