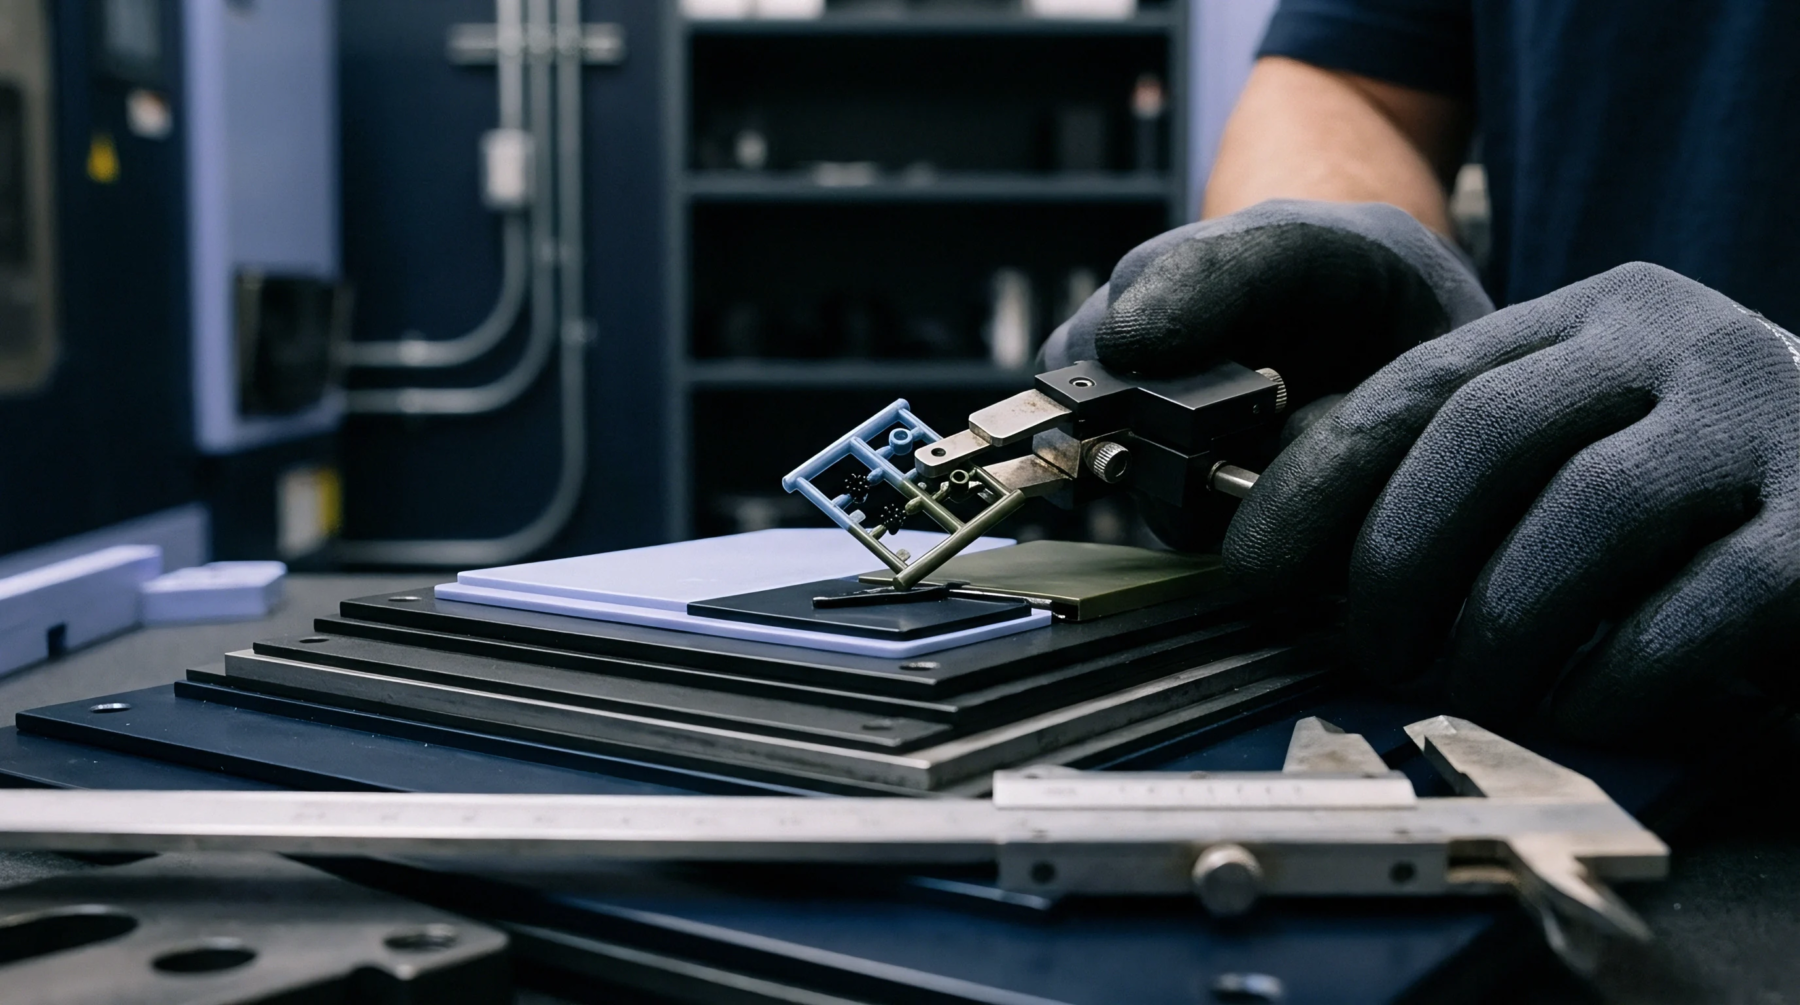
Meaning
Electro-discharge subtraction techniques erode metal using microscopic spark discharges to form intricate cavity geometries and micro vent channels in tool steel. Utilizing micro EDM machining allows toolmakers to cut narrow rib features, sub-millimeter gate openings and precise optical surface textures into hardened mold inserts. The method governs gate location precision, micro fluidic channel geometry and detail replication on core pins.
It stops applying when machining non conductive materials like ceramics or uncured polymer stock.
Erosion Dynamics
Fine copper or tungsten wire electrodes discharge high frequency electrical pulses into dielectric fluid to vaporize steel at microscopic scales. The pulse energy governs spark gap size, crater diameter and thermal recast layer thickness on tool steel faces. Toolmakers use micro EDM machining to generate fine ejector pin holes that prevent flash in high pressure moulding tools.
Precise spark control allows tool creation without introducing mechanical stress into delicate core structures.
Surface Finish
Sub microscopic discharge sparks produce uniform satin textures that improve part release during molding cycles.
Feature Resolution
Producing micro scale features requires electrodes shaped to tolerances below two micrometers. Steel cavities finished with micro EDM machining yield micro mould parts with sharp internal corners and minimal draft angles. High precision tool inserts enable processing of LCP and PEEK resins without material bleeding into vent paths.
Tooling accuracy directly determines whether final moulded plastic features meet micro fluidic and optical application specifications.