Meaning
The permanent status assigned to a validated polymer sample under this specific operational directive declares that once an article achieves approval during initial trials, that identical physical configuration remains the sole legal standard for subsequent production runs. The strict protocol governs tool qualification and cavity geometry, halting at the boundary of ordinary machine wear or approved engineering change orders.
Thermal Drift
Polymeric material behavior depends heavily upon barrel temperature profiles and clamp tonnage settings during injection. Variations in screw speed or back pressure alter molecular orientation across the molded part, creating localized stresses that deviate from approved reference standards. Production shifts experience dimensional shrinkage whenever melt temperatures drift outside specified processing windows, resulting in rejected components that fail initial part qualification checks.
Virgin resin batches exhibit different flow rates compared to recycled regrind streams, forcing technicians to adjust cooling times constantly to maintain part integrity. Machine operators must verify that hopper drying cycles remove sufficient moisture before pellets enter the feed throat, avoiding hydrolytic degradation in moisture sensitive engineering thermoplastics.
Cavity Pressure
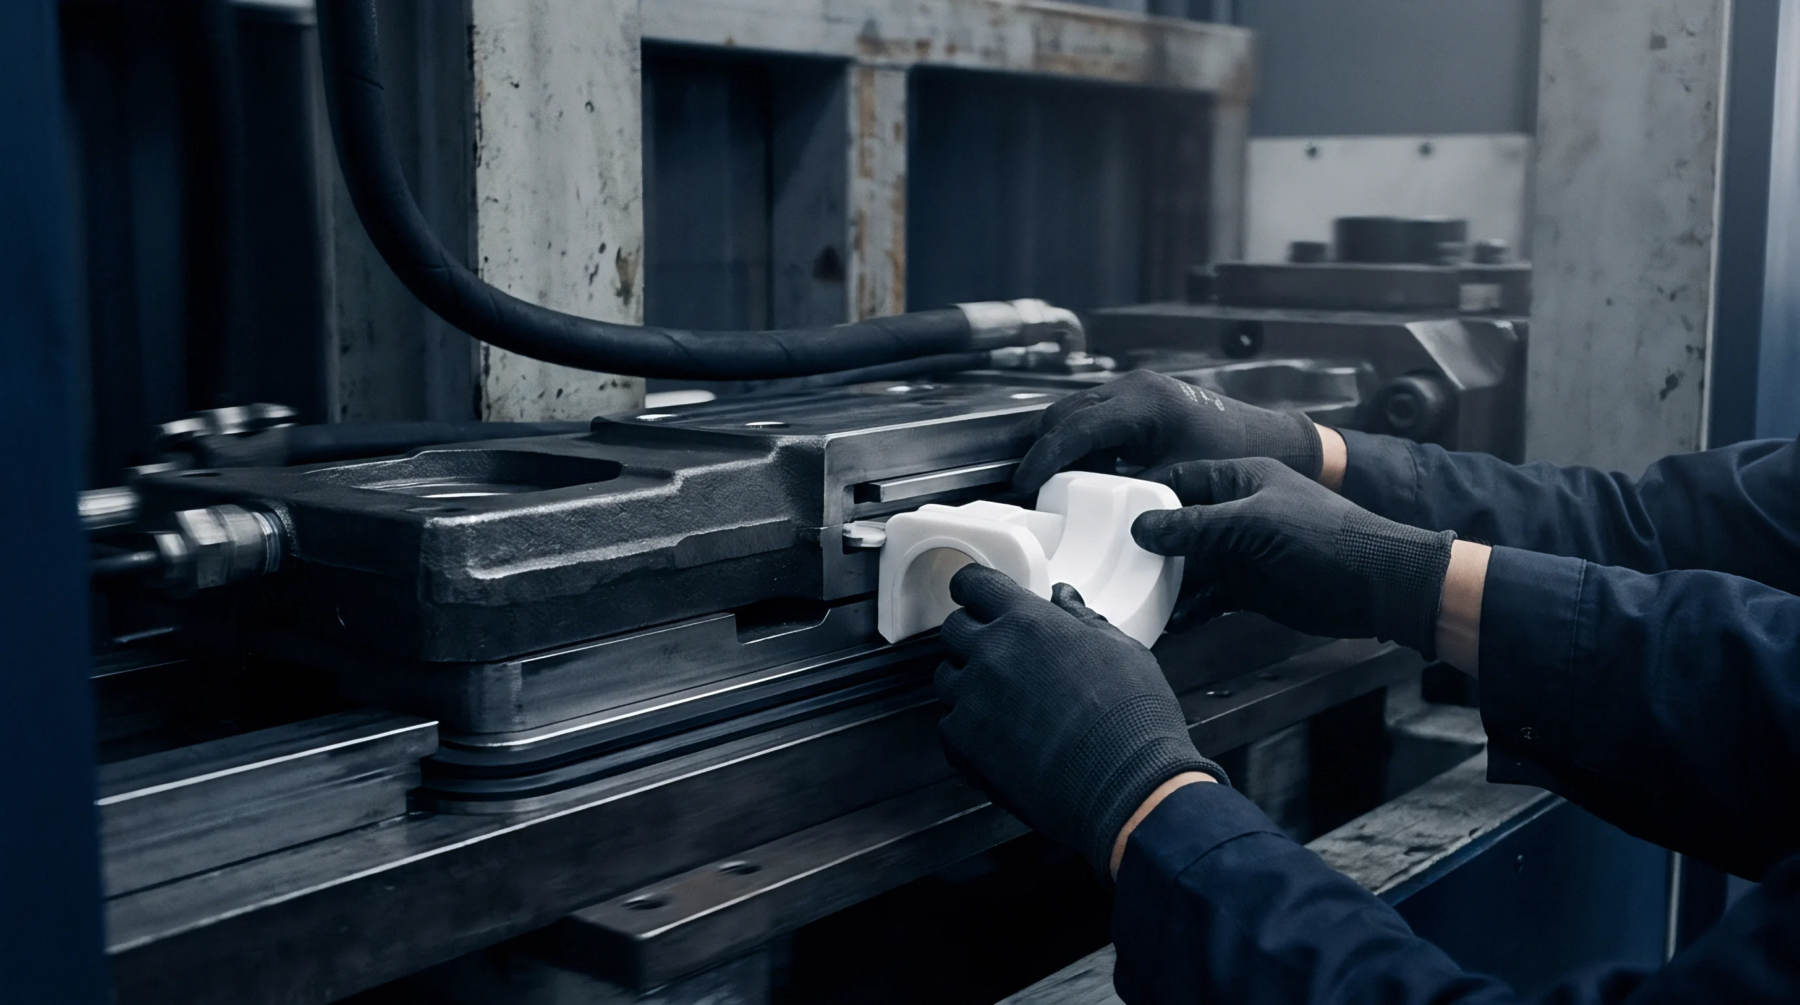
Tooling engineers monitor cavity pressure sensors embedded near the gate to track how plastic fills each individual mold insert during high pressure injection stages. Pressure curves provide immediate feedback regarding melt viscosity shifts, allowing automated controllers to compensate for batch variations before sink marks or short shots materialize on finished components. Multi cavity molds require balanced runner systems to ensure equal packing rates across every impression, preventing warp and uneven dimensional growth.
Production facilities maintain stringent calibration schedules for pressure transducers, because inaccurate sensor readings allow defective parts to pass downstream inspection gates undetected.
Specification Boundary
Component specifications dictate the final mechanical performance and geometric tolerances required for functional assembly in demanding industrial applications. Material datasheets supply baseline properties measured under controlled laboratory conditions, whereas actual injection molding environments introduce thermal gradients and shear stresses that alter final part behavior. Moulders establish processing windows that bridge the gap between theoretical laboratory values and real world shop floor capabilities, ensuring consistency across high volume production runs.
Component geometry changes require formal drawing revisions and new sample submissions, preventing unauthorized modifications from entering the supply chain without rigorous quality verification.